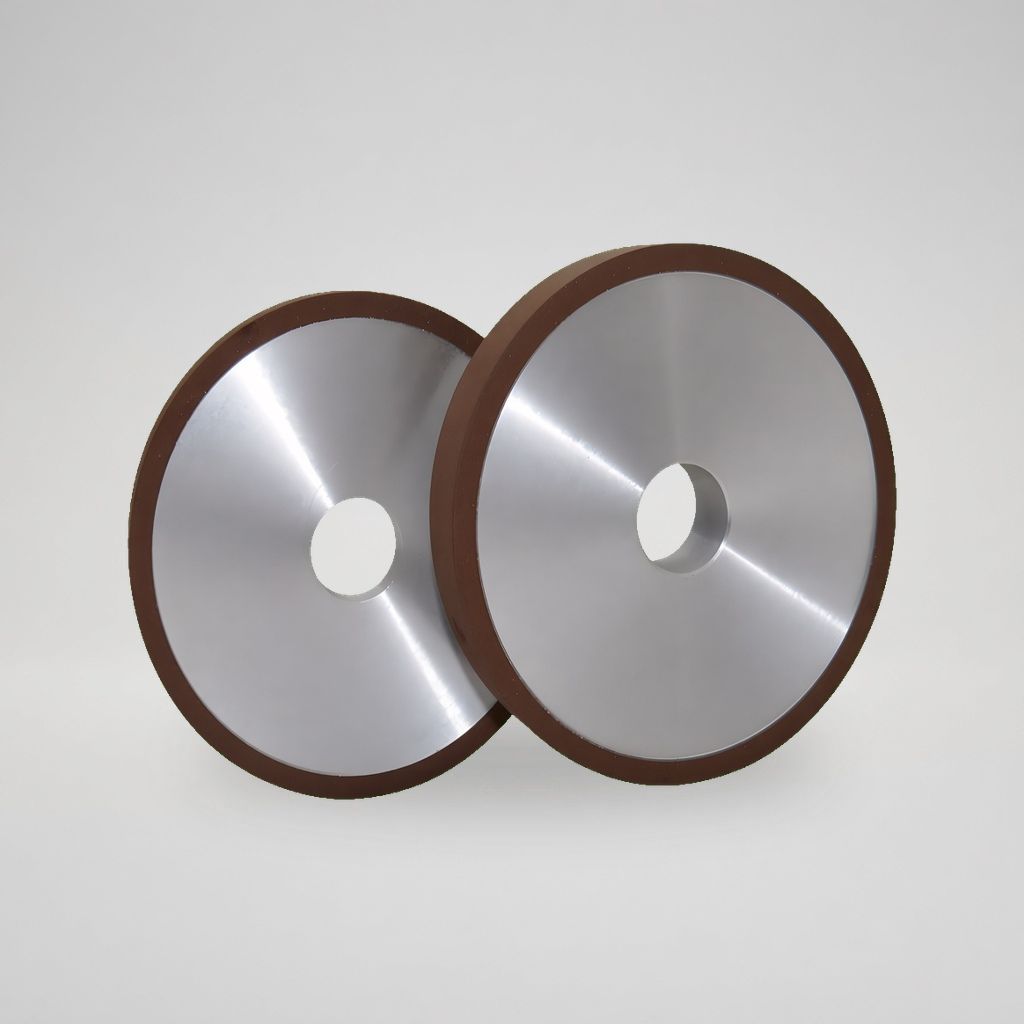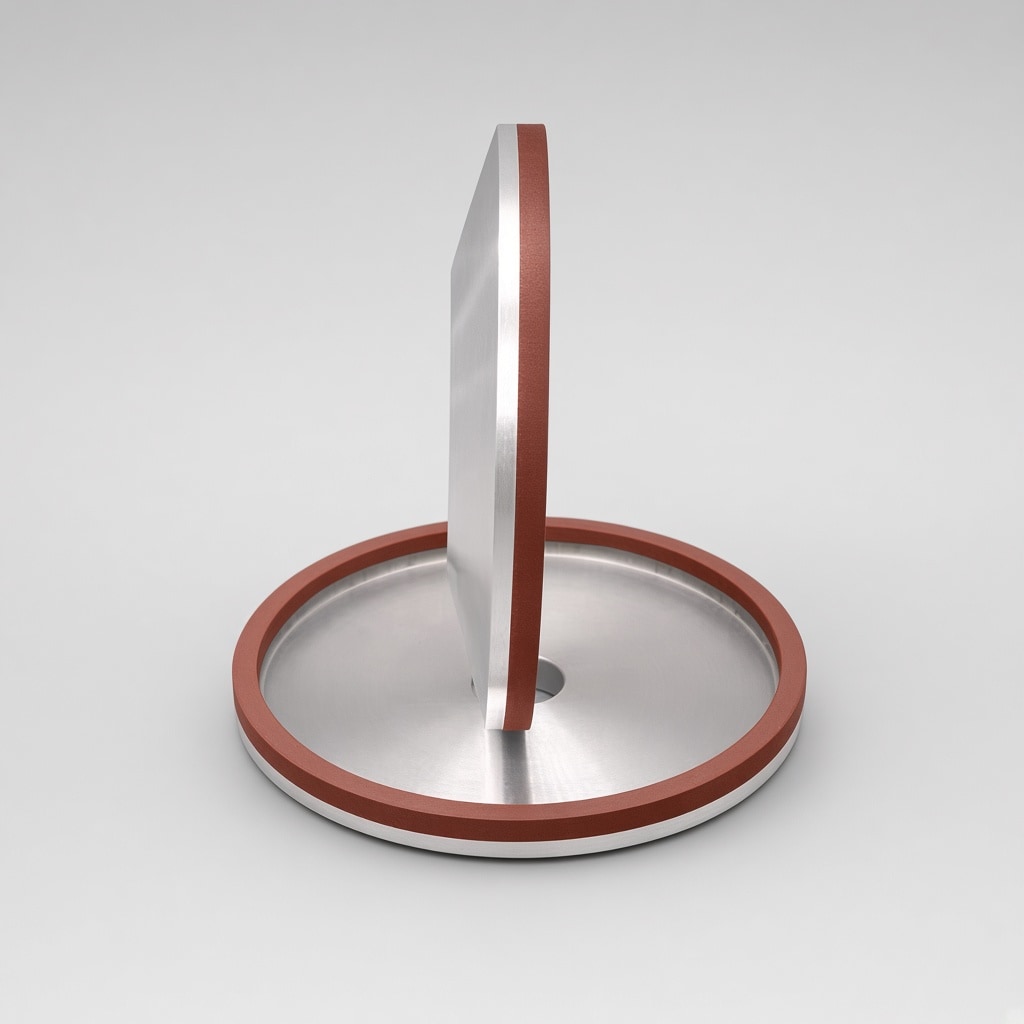
Metal Bond Diamond Wheels for Glass
- Wet edge grinding that holds profile on long runs
- 1A1R for thin cut-off of sheet and tube
- Diamond abrasive — not CBN, not for steel
- Made to your diameter, grit, and concentration
Product Information
What we grind
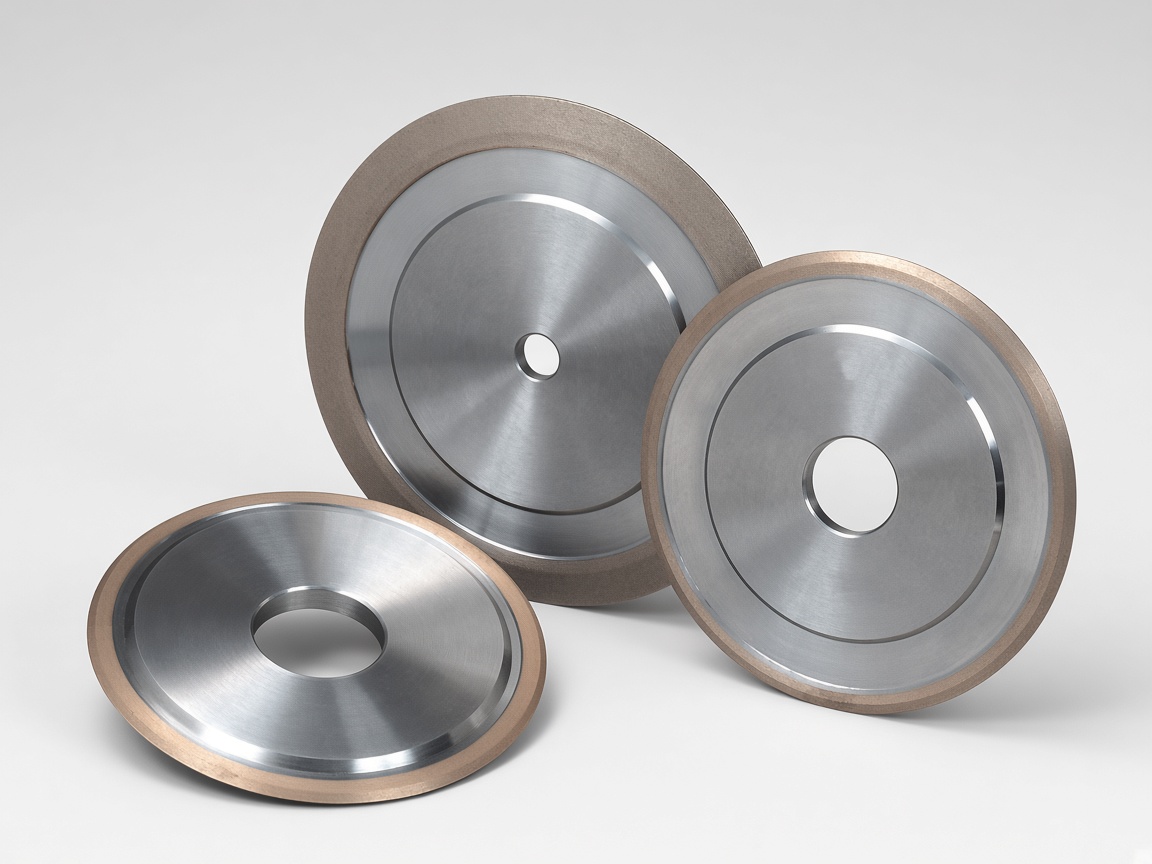
Metal bond wheels grind glass, not wood, not carbide tools, and not granite. Architectural float and laminated glass, glass-ceramic, and optical blanks — on straight-line edgers, bevellers, and cut-off saws.
Metal bond is used here for life and a stable edge. The rim does not shed grit the way resin does, so an arris or OG stays consistent through a shift. Coolant is normal; dry glass grinding is the exception, not the spec.
Carbide end mills belong on the Carbide Cutting Tools page. TCT saws belong on Woodworking Tools. Quartz tube, plate, and technical ceramics belong on Quartz and Ceramics. Granite, marble, and engineered stone belong on Stone.
Edge grinding or cut-off
Edge grinding and cut-off use different wheels.
Edge, arris, and OG
Straight-line edgers and bevellers (Bovone, Bottero, Bavelloni, Intermac, and equivalent) use a peripheral or cup wheel to grind the seamed edge, arris, or decorative OG. Start with 1A1. 6A2 when the machine takes a cup on the face.
Chip size and polish after the metal wheel are line settings, not a second bond. If the factory only needs a throwaway form for a short contour, electroplated may fit better.
Thin cut-off
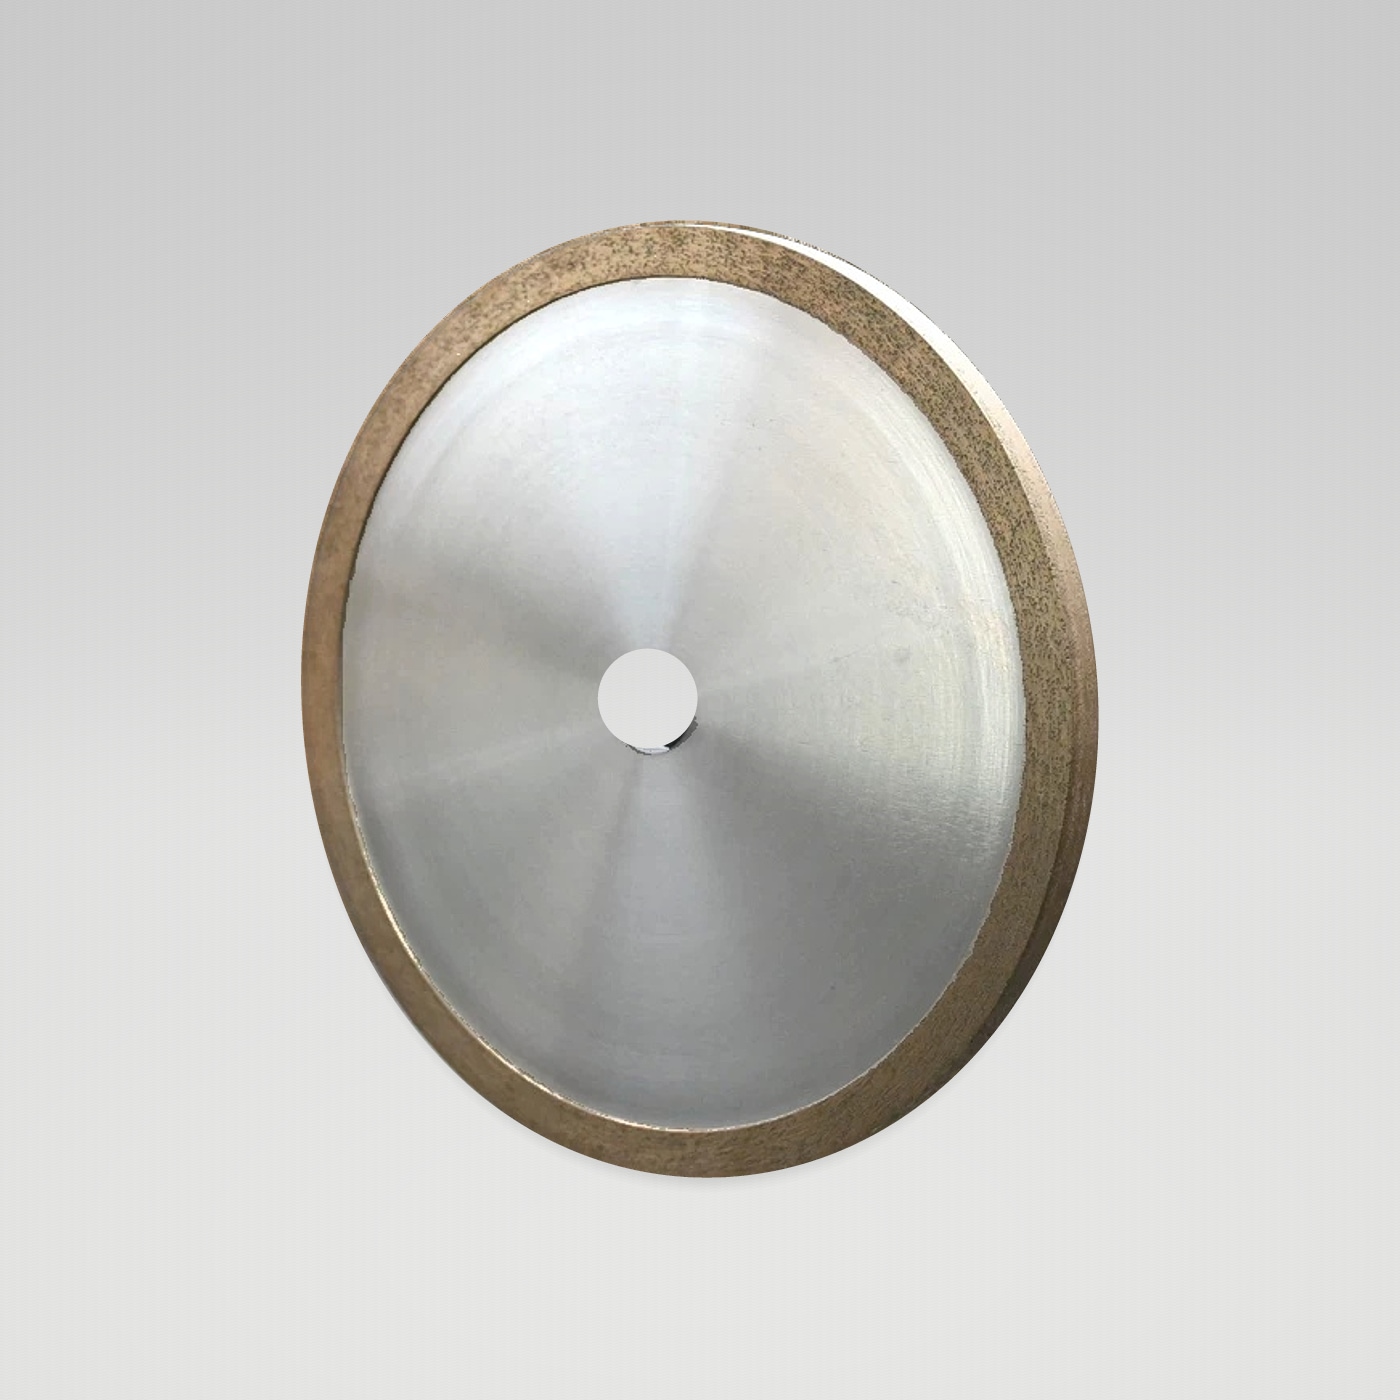
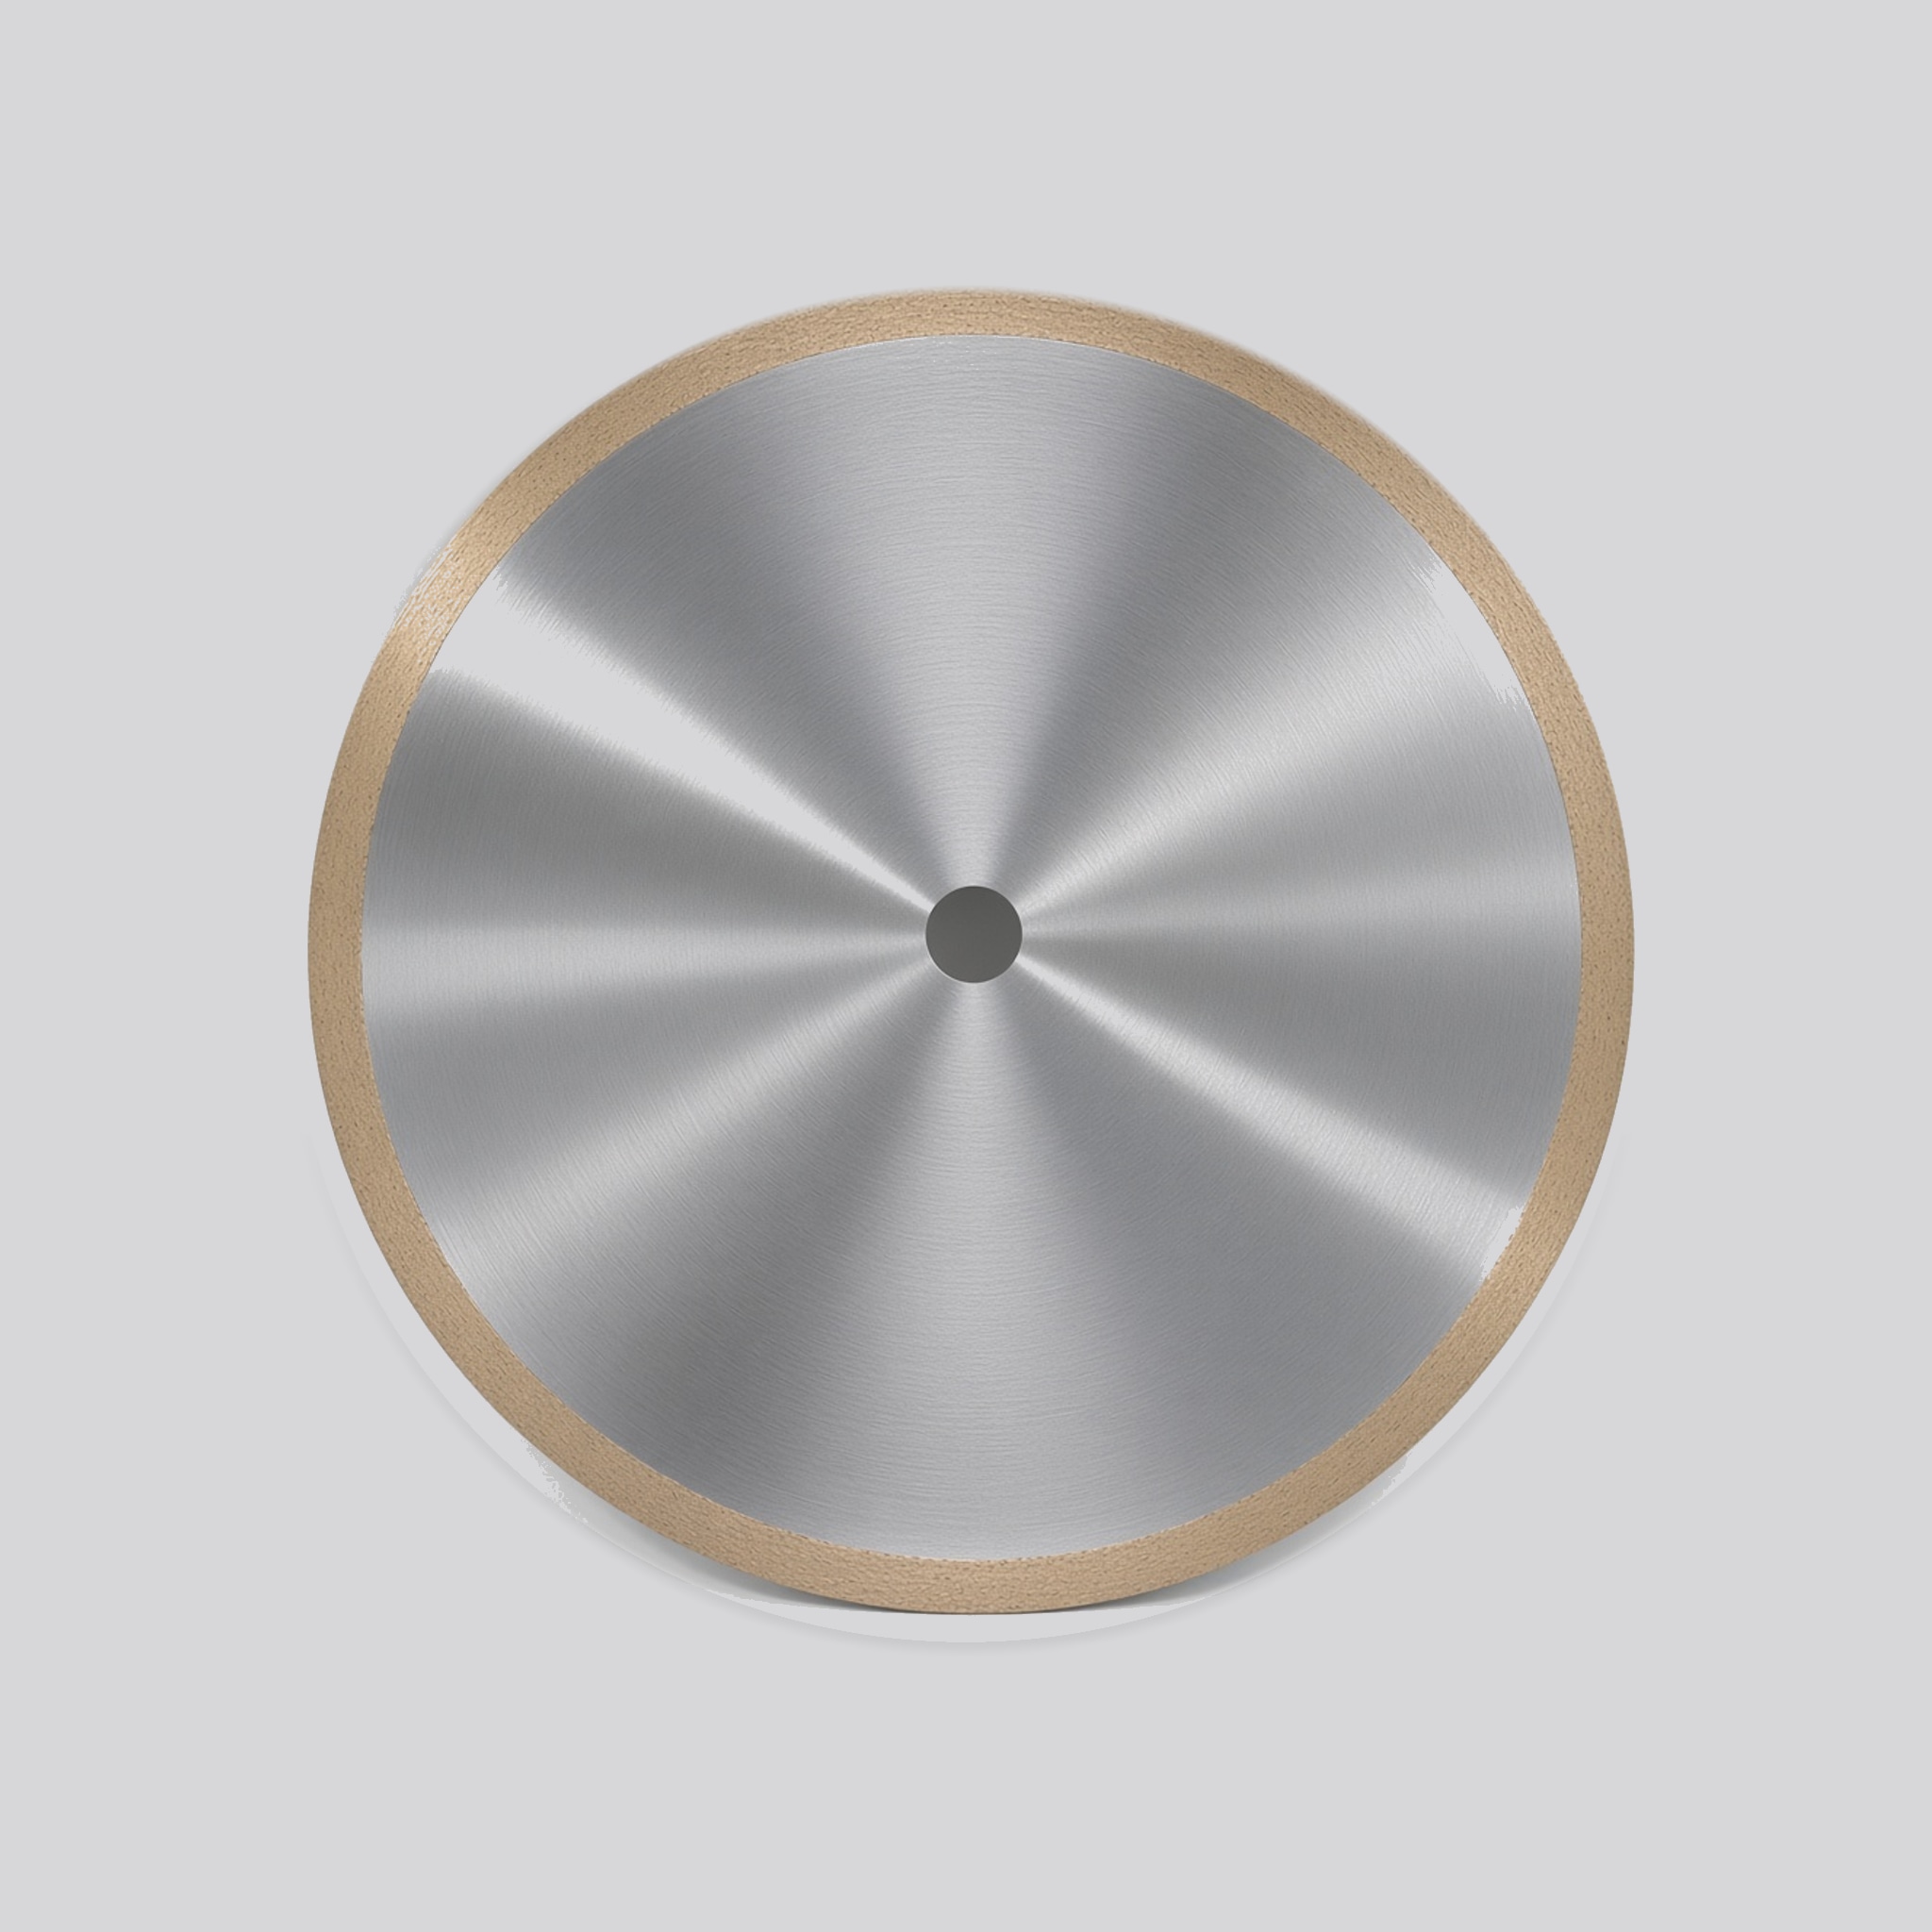
Sheet, tube, and rod cut-off use a thin 1A1R. Kerf and runout matter more than a pretty rim. Wet cut-off is the default.
Short-run or very thin cut-off can also be electroplated 1A1R. Metal 1A1R is the production choice when the blade has to last.
Shapes
| Shape | Drawing | Role on glass |
|---|---|---|
| 1A1 | ![]() |
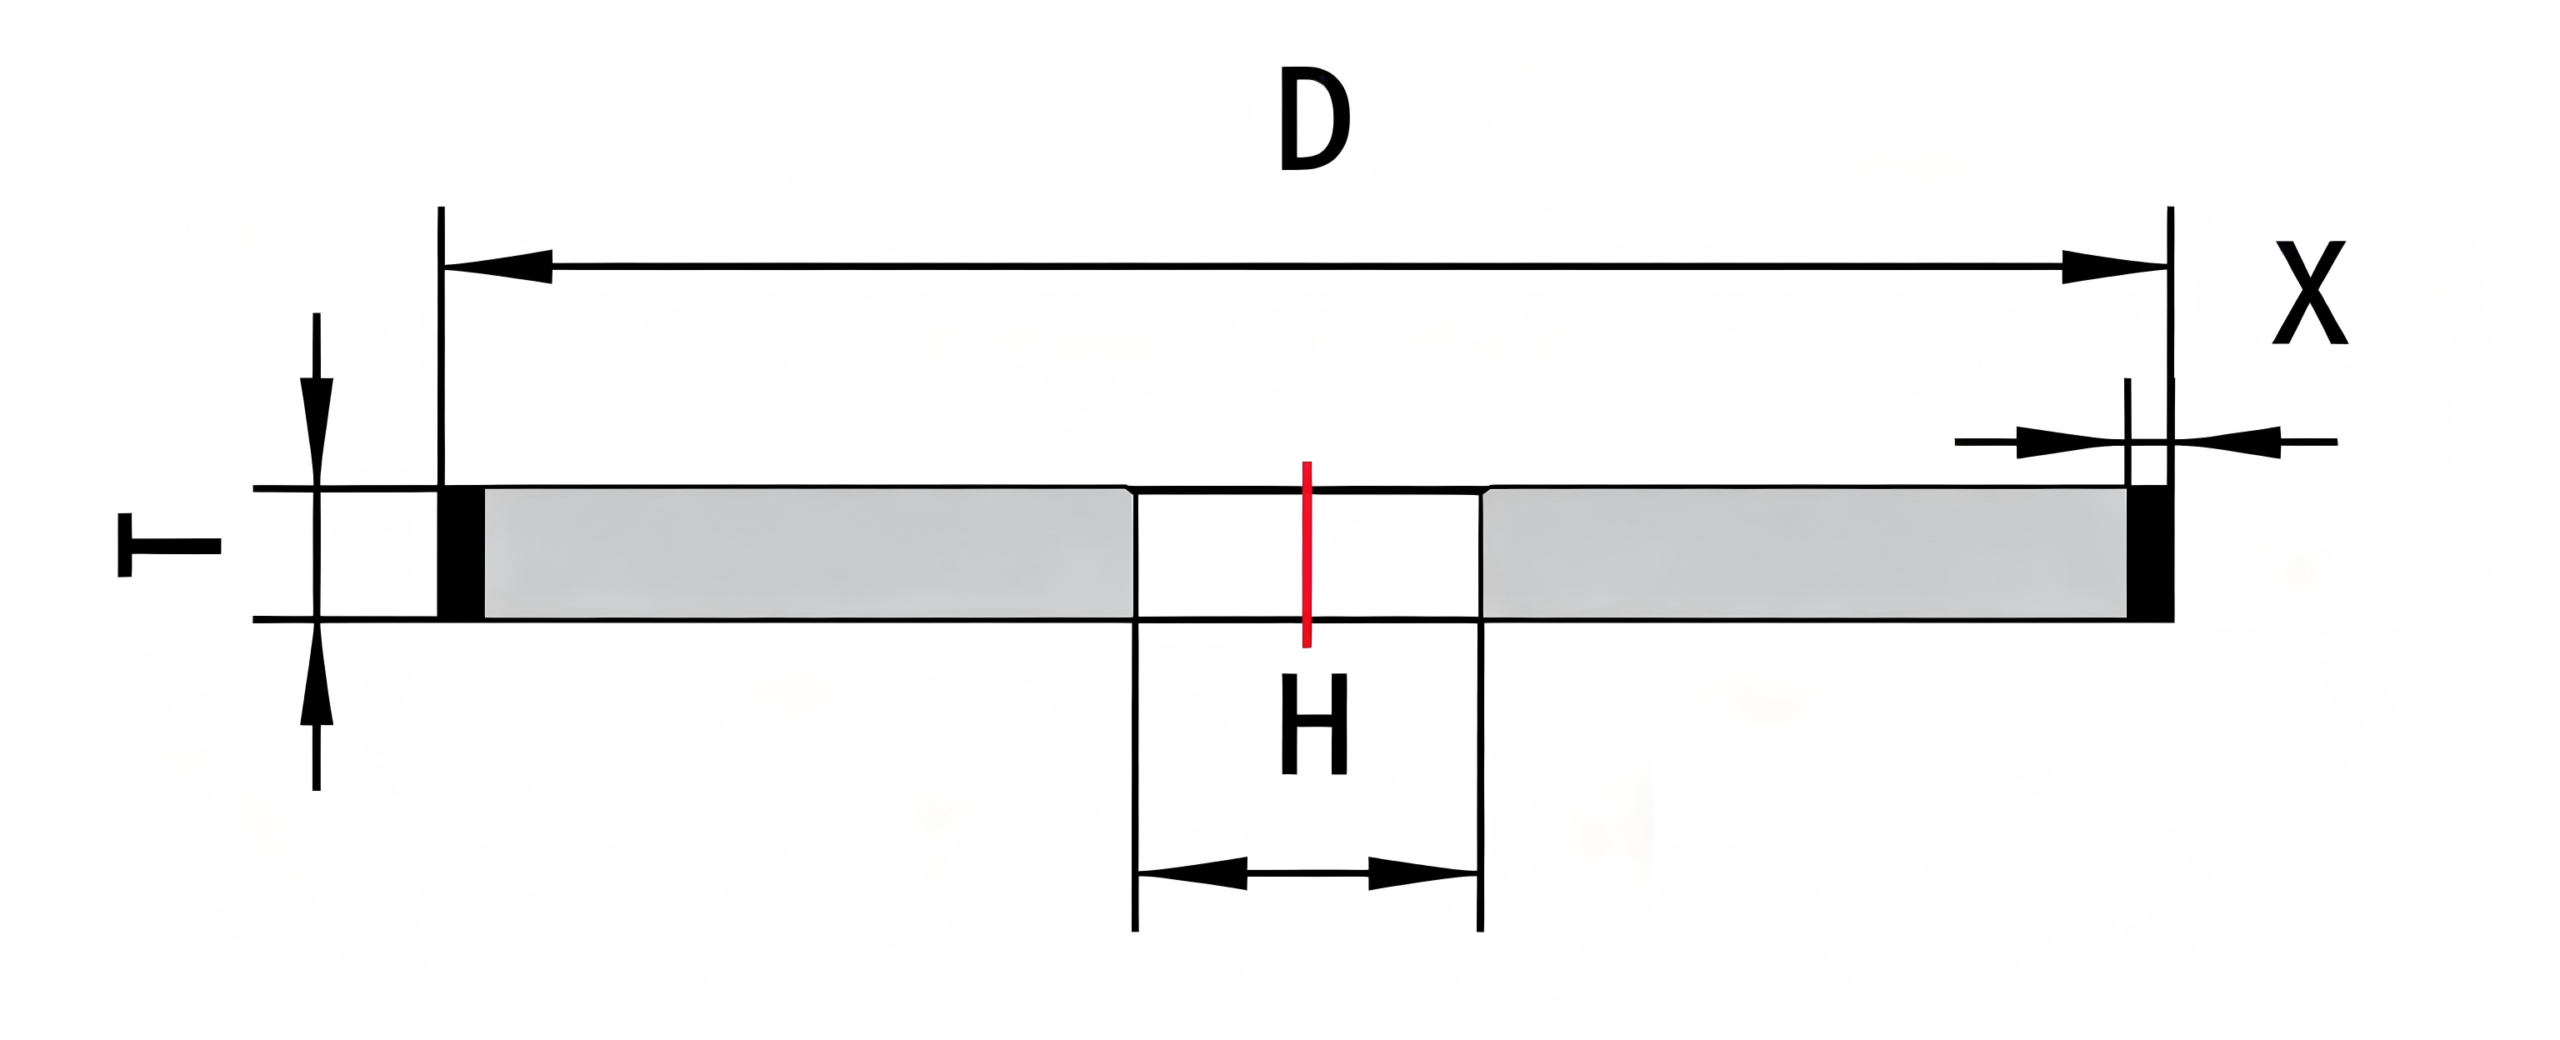
Peripheral edge grinding on straight-line and CNC edgers |
| 1A1R | ![]() |
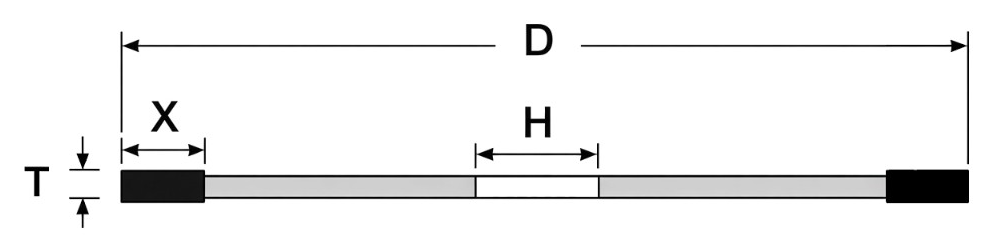
Thin cut-off of sheet, tube, and rod |
| 6A2 | ![]() |
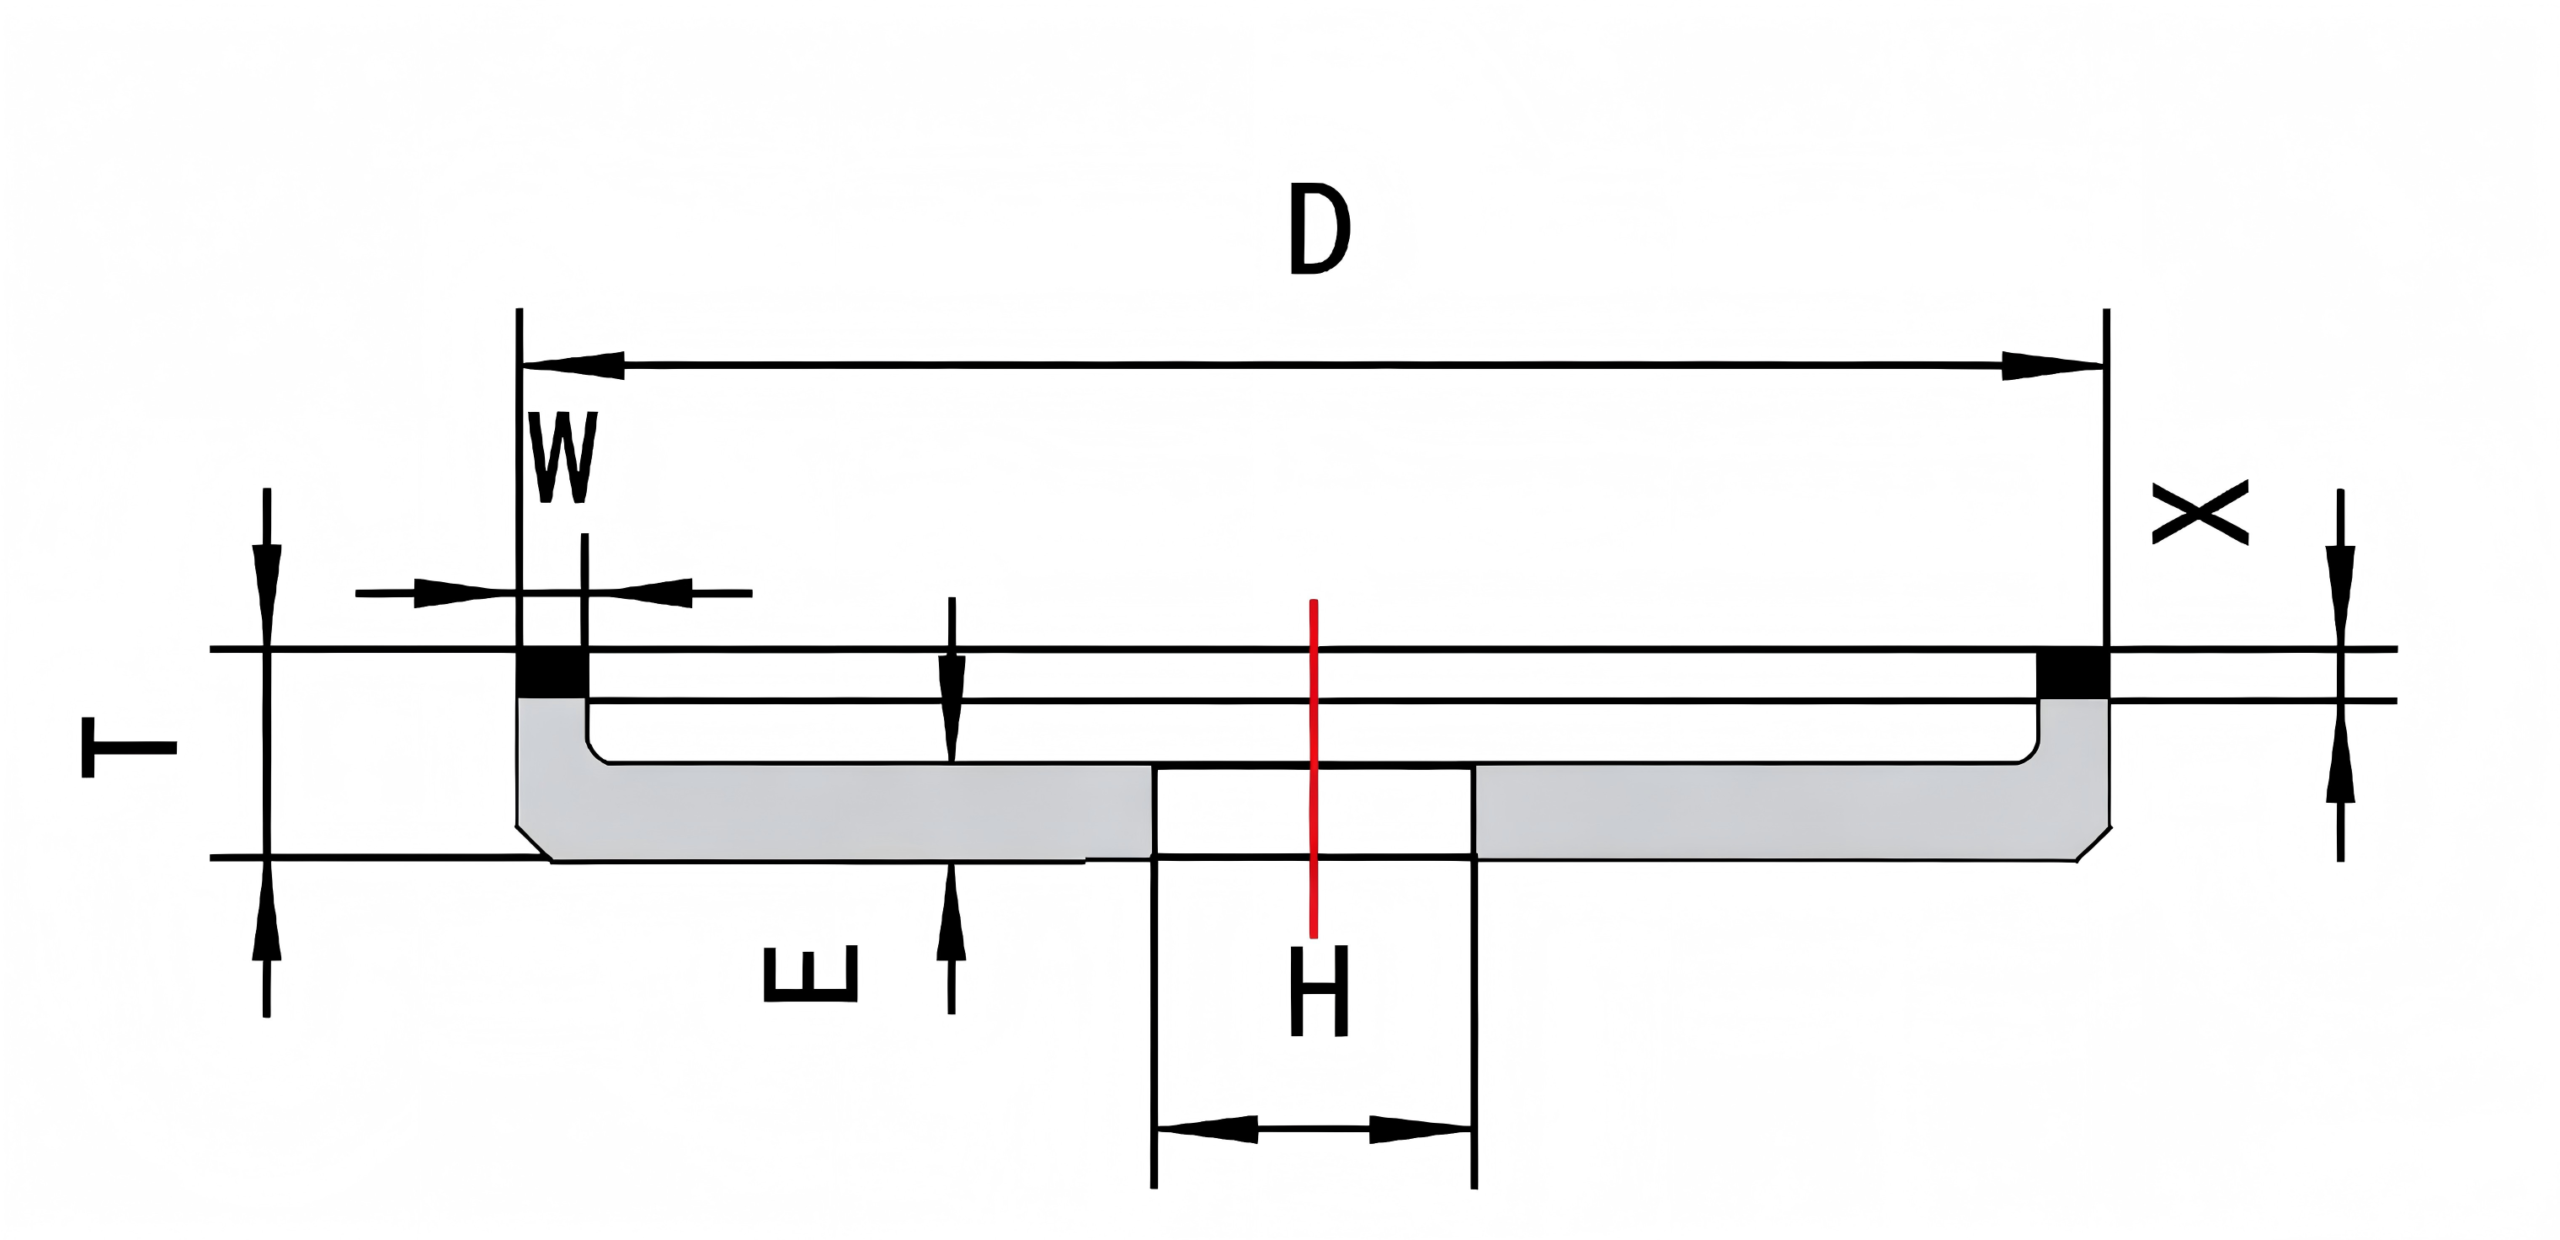
Cup grinding on faces and some beveller stations |
Also available: 1V1 (narrow grooves). If your line already runs a pencil or peripheral mark, send the stamp — we match it.
Send a mark such as 1A1-150-10-22 D76 or 1A1R-125-0.6-22 plus glass type and wet/dry. We match diameter, thickness, hole, grit, and concentration to the spindle and coolant.
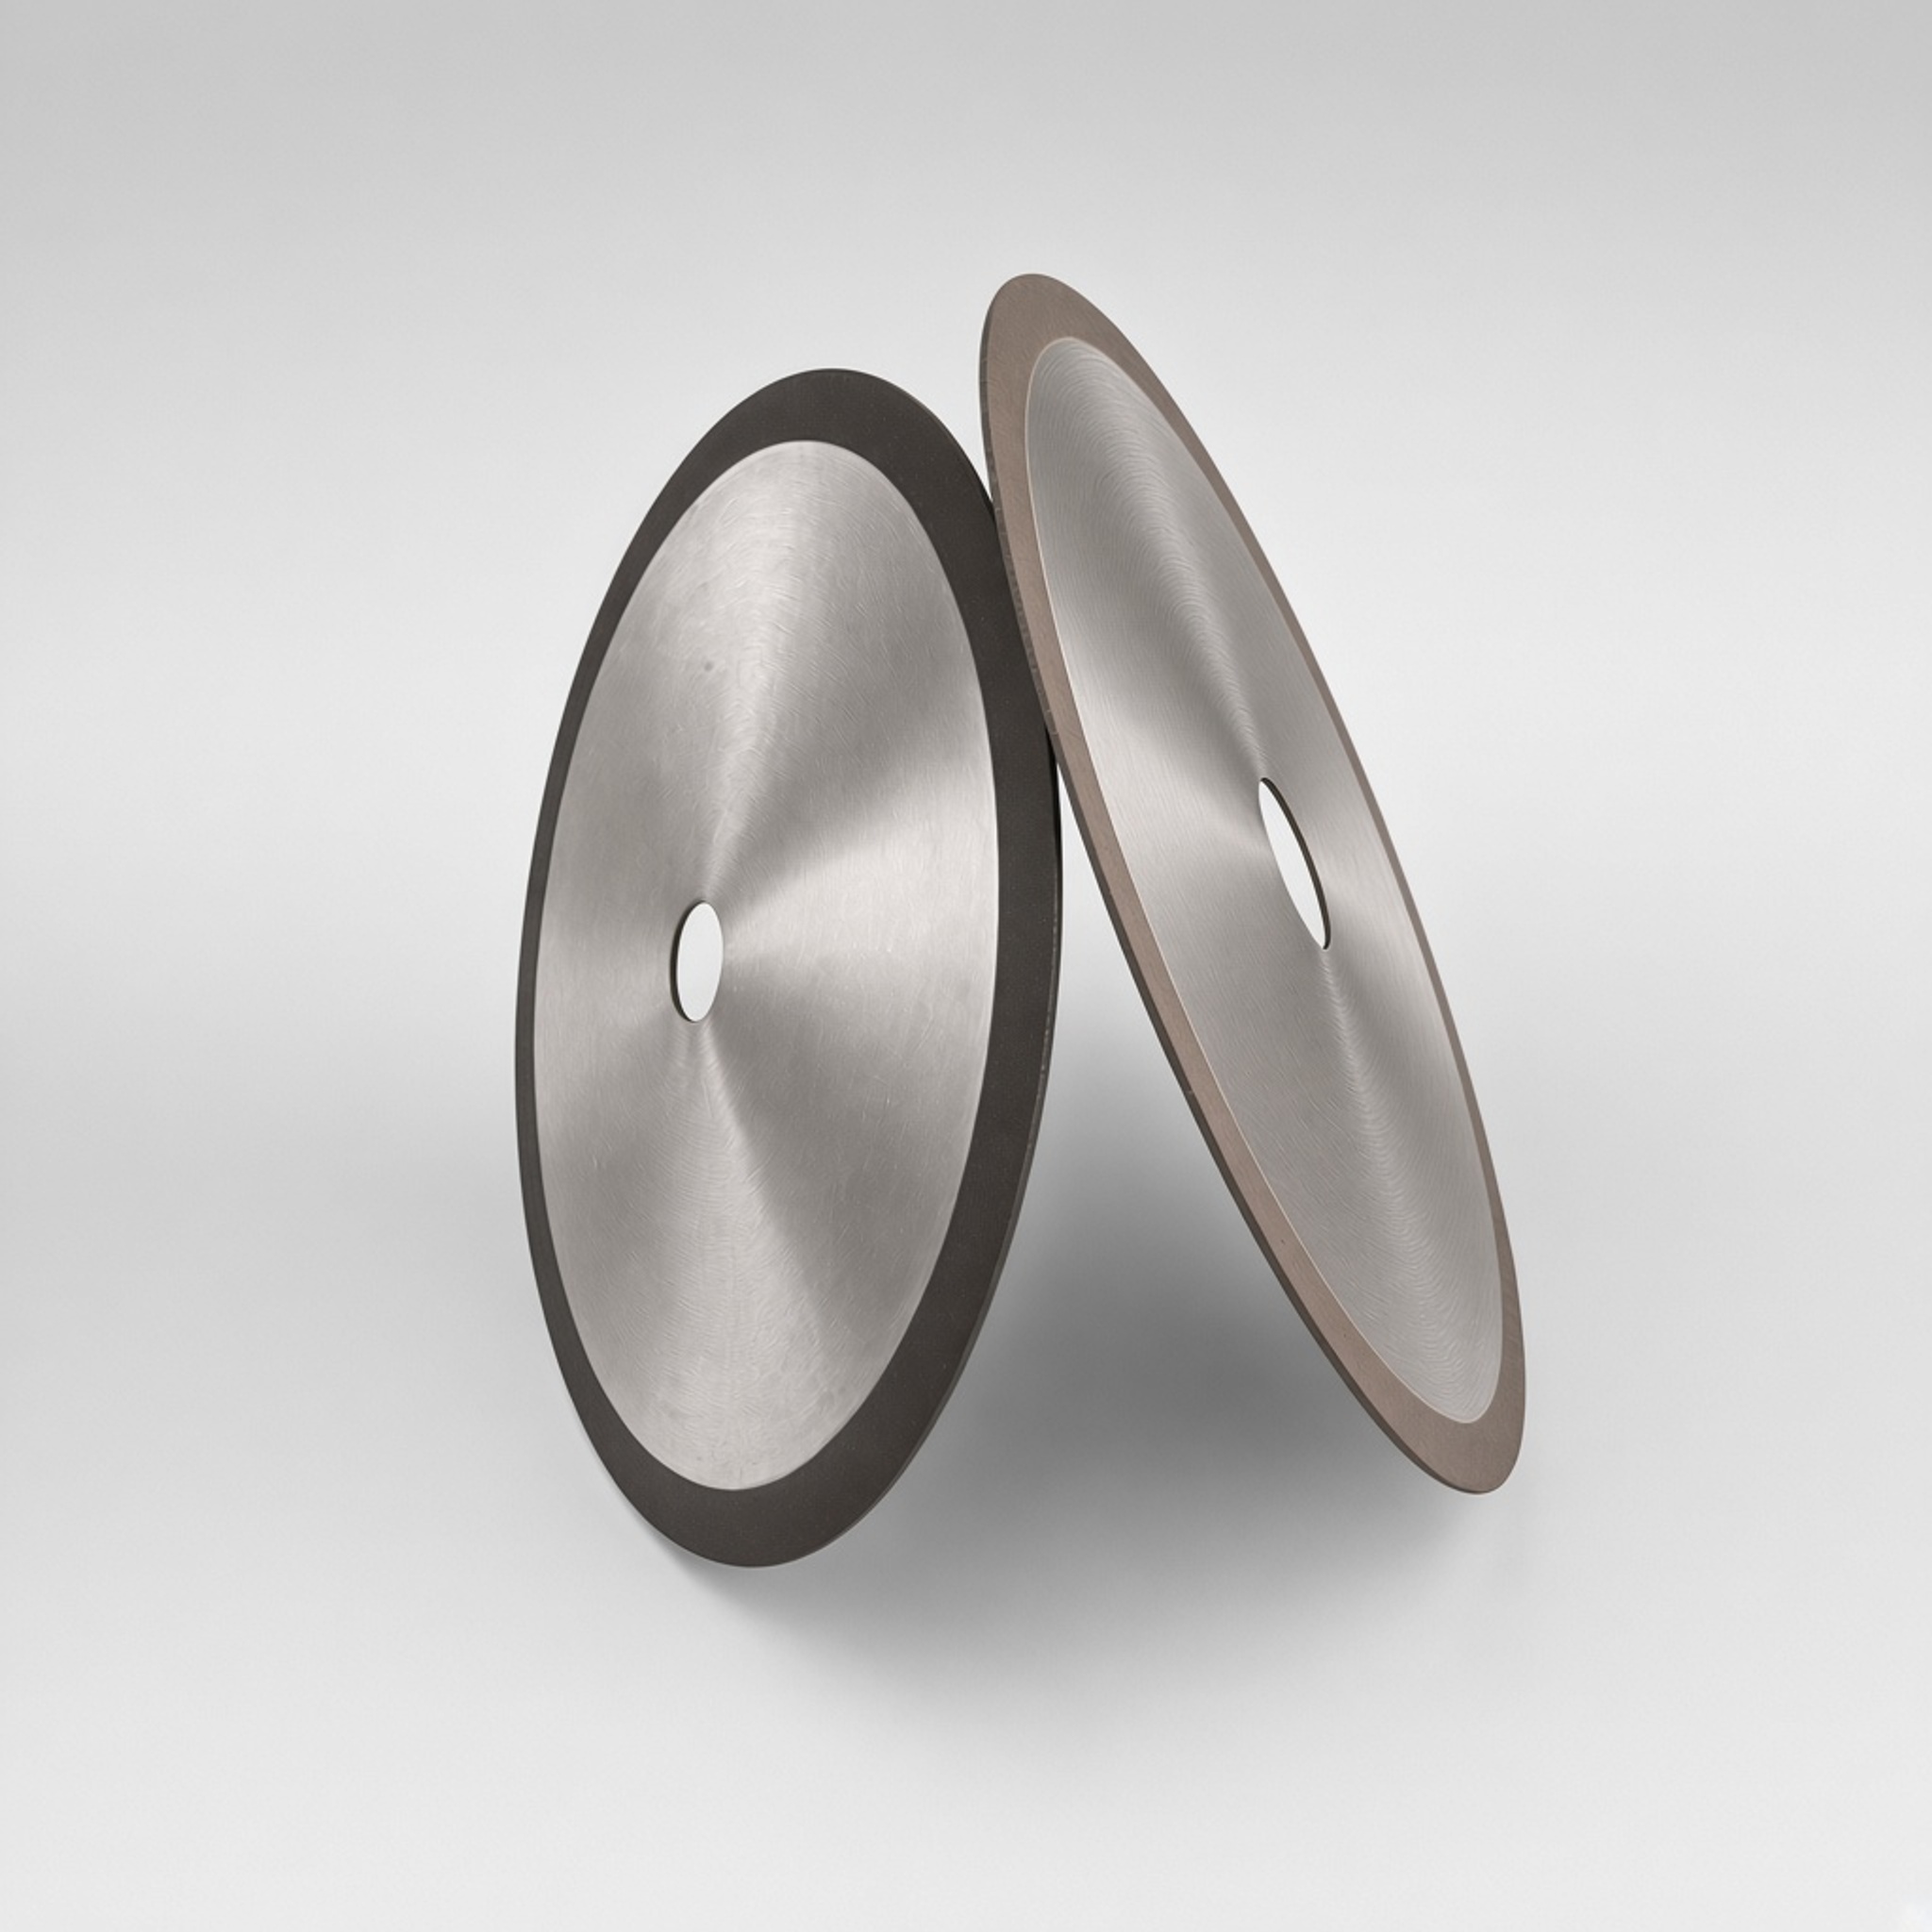
When metal bond is the wrong wheel
- One-off contour or a plated form you will scrap after a short job → electroplated
- Fine polish after the metal edge, if you already run a resin or felt station → keep that station
- Carbide tools, TCT saws, mold steel → resin bond
- Production grinding of hardened steel → vitrified CBN
- Granite, marble, and engineered stone → Stone
Metal bond wheels are wet, diamond, and made for glass.