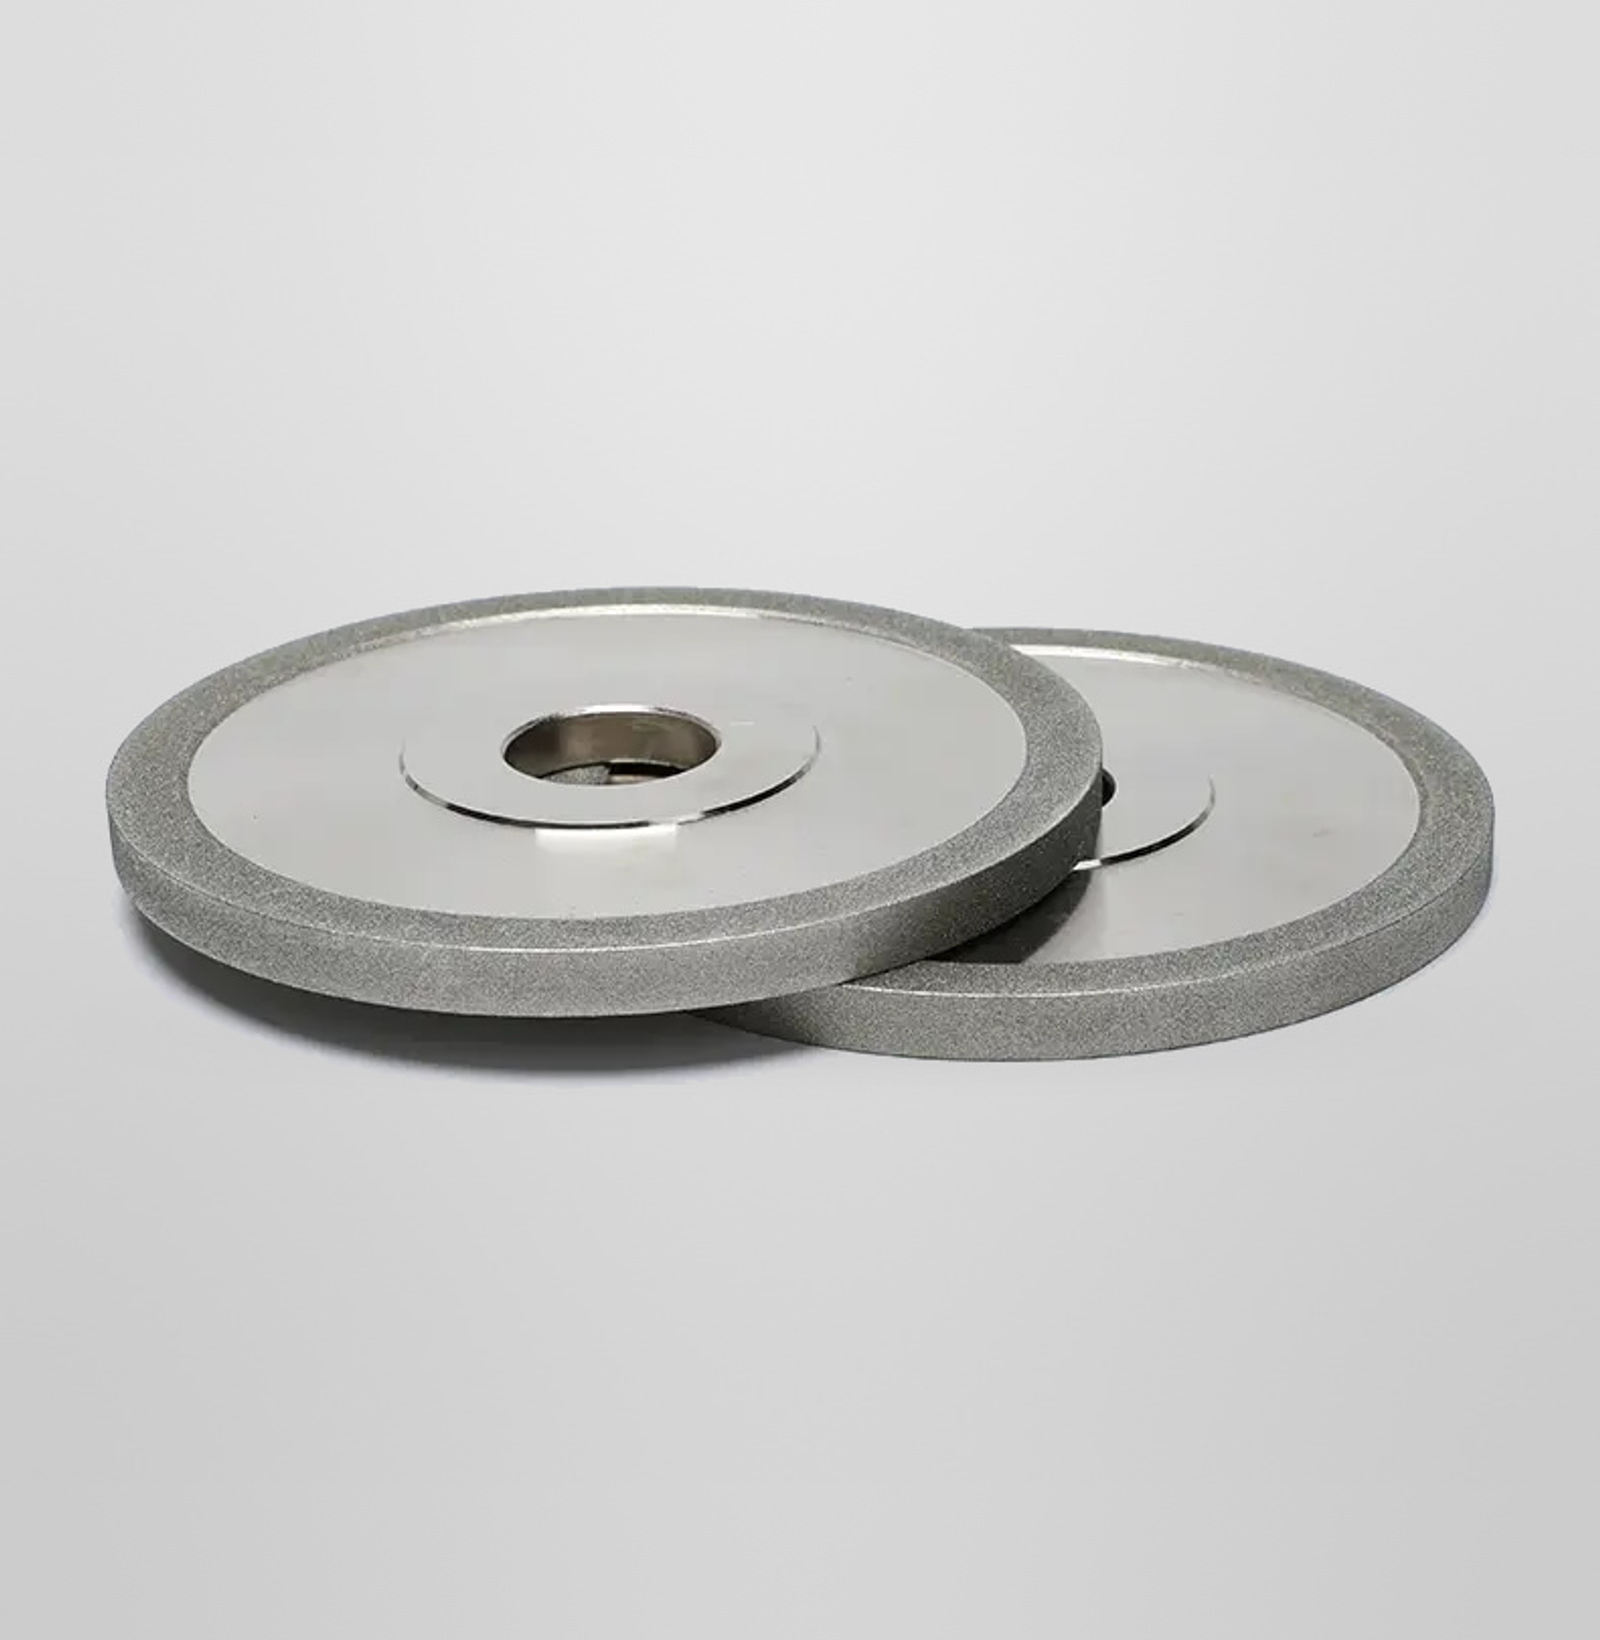
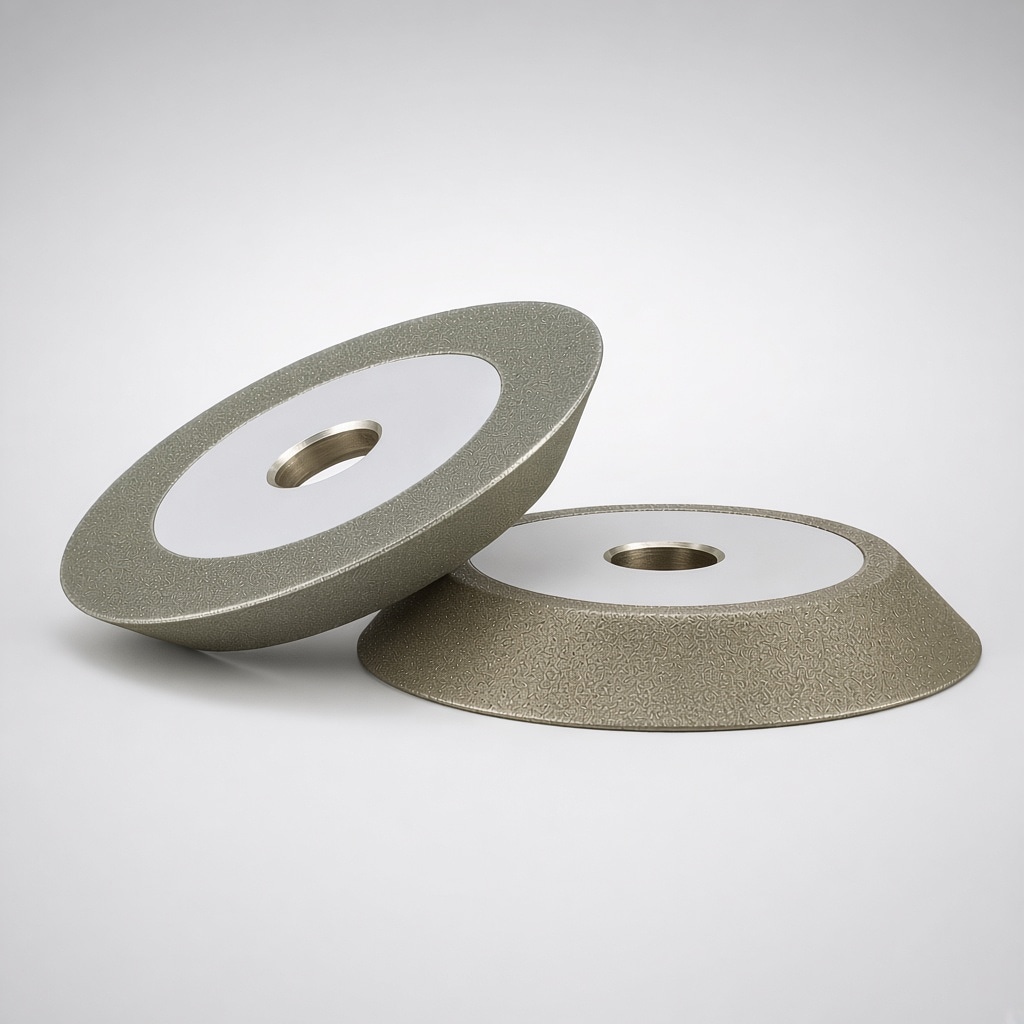
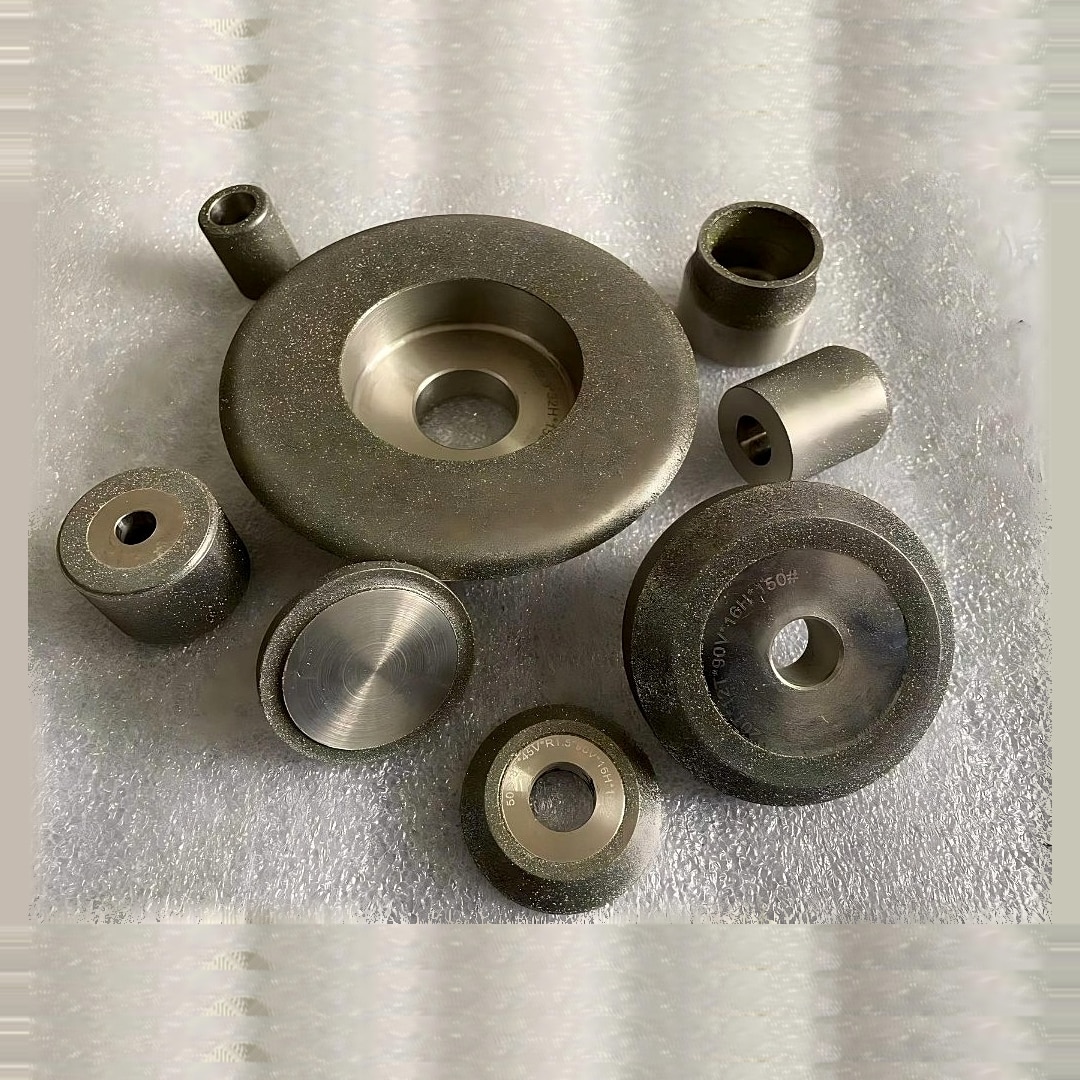
Electroplated Wheels for Jig and Internal Grinding

Product Information​

Overview

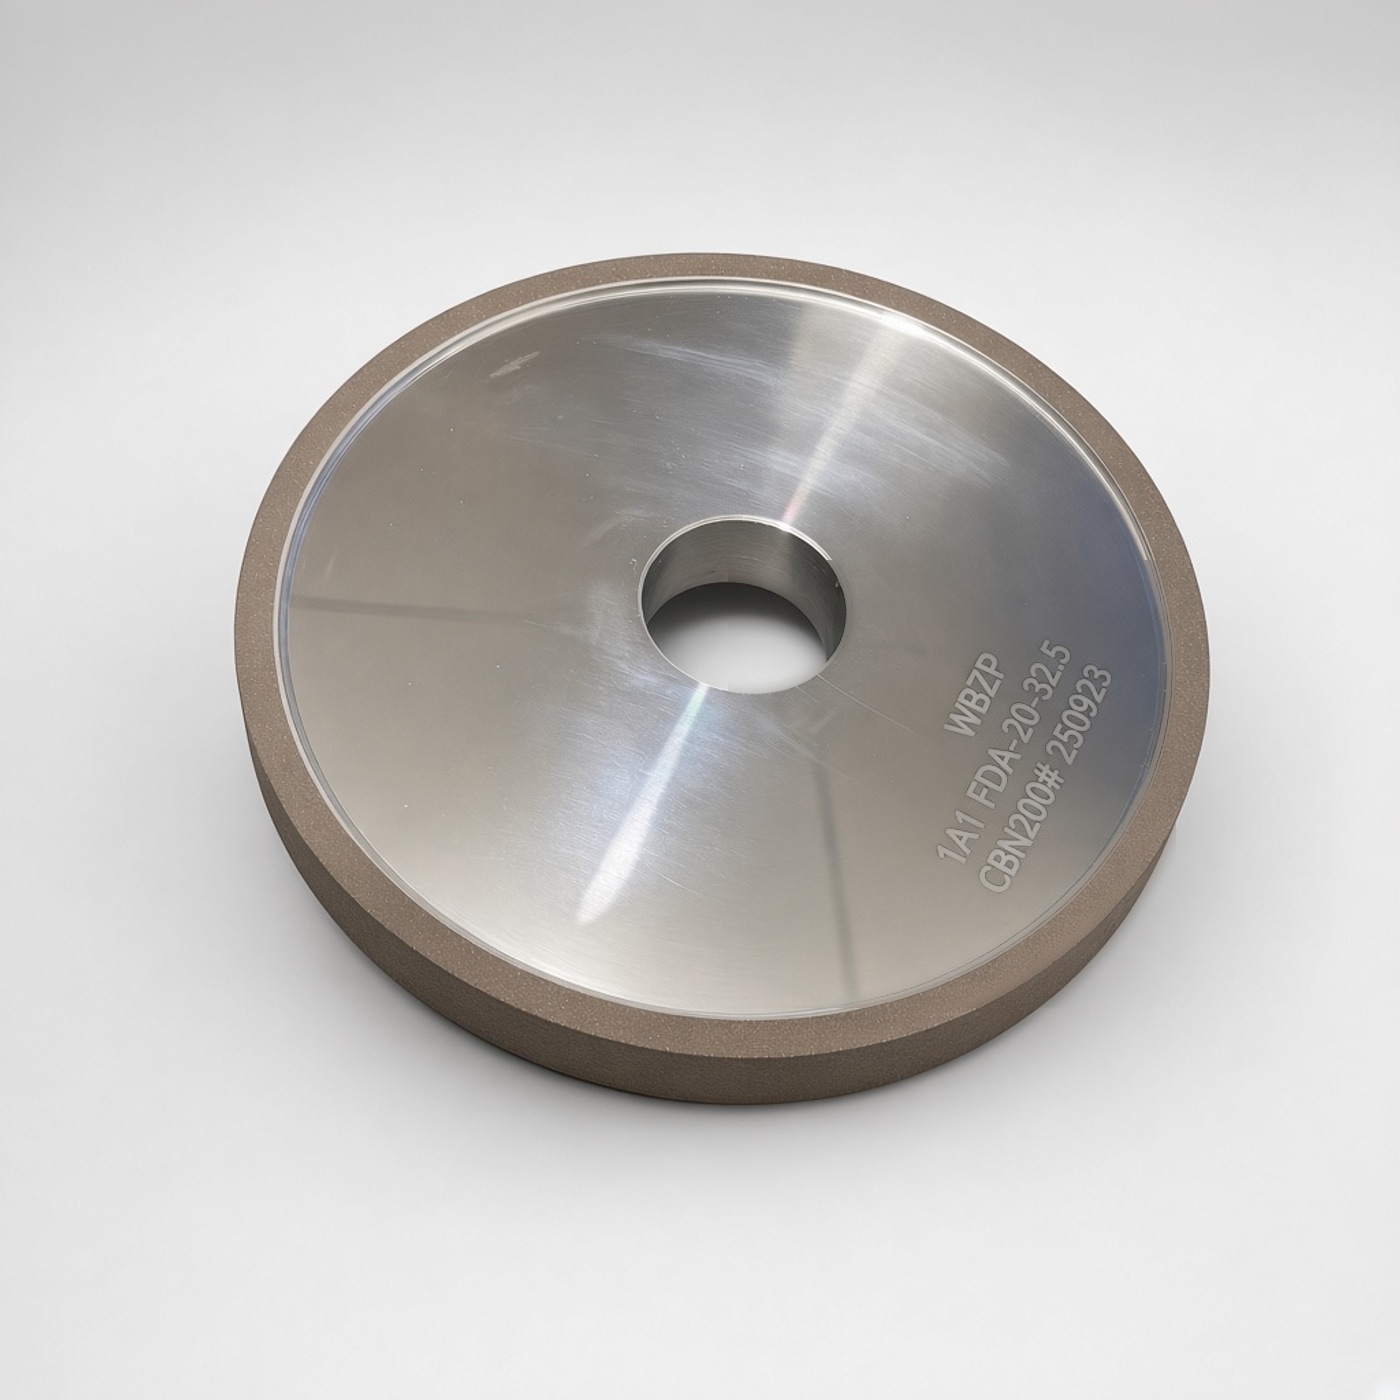
Electroplated wheels for jig grinding and internal grinding of bores, bushings, and related geometry. Single-layer abrasive on a steel core or shank. Wet grinding is standard.

  • Exposed grit on a small diameter — reaches the bore without a wide rim
  • Form is the plated layer; there is nothing to dress — replace when dull
  • Diamond for carbide, ceramics, and similar non-ferrous hard work
  • CBN for hardened steel dies, punches, and steel bores

Applications:

  • Jig grinding of die holes, punch openings, and locating bores (Moore, Hauser class)
  • Internal grinding of carbide and ceramic bushings
  • Hardened steel ID where a plated CBN rim is specified
  • Small-diameter form in the bore when the drawing is already 1A1 or 1V1

Thin cut-off of glass, quartz, LED, and ceramic blanks stays on electroplated cut-off. Production ID of hardened steel on a dressable ceramic bond stays on vitrified CBN.

Versus electroplated cut-off

Same nickel plate. Different job. Not interchangeable with electroplated 1A1R cut-off.

Jig / internal Cut-off
Lead shape1A1, 1V11A1R
JobBore, bushing, jig grindingThin wet cut-off
What you orderDiameter vs the hole; shank or HThickness is the kerf
AbrasiveDiamond or CBNDiamond

Shapes

Shape Drawing Role
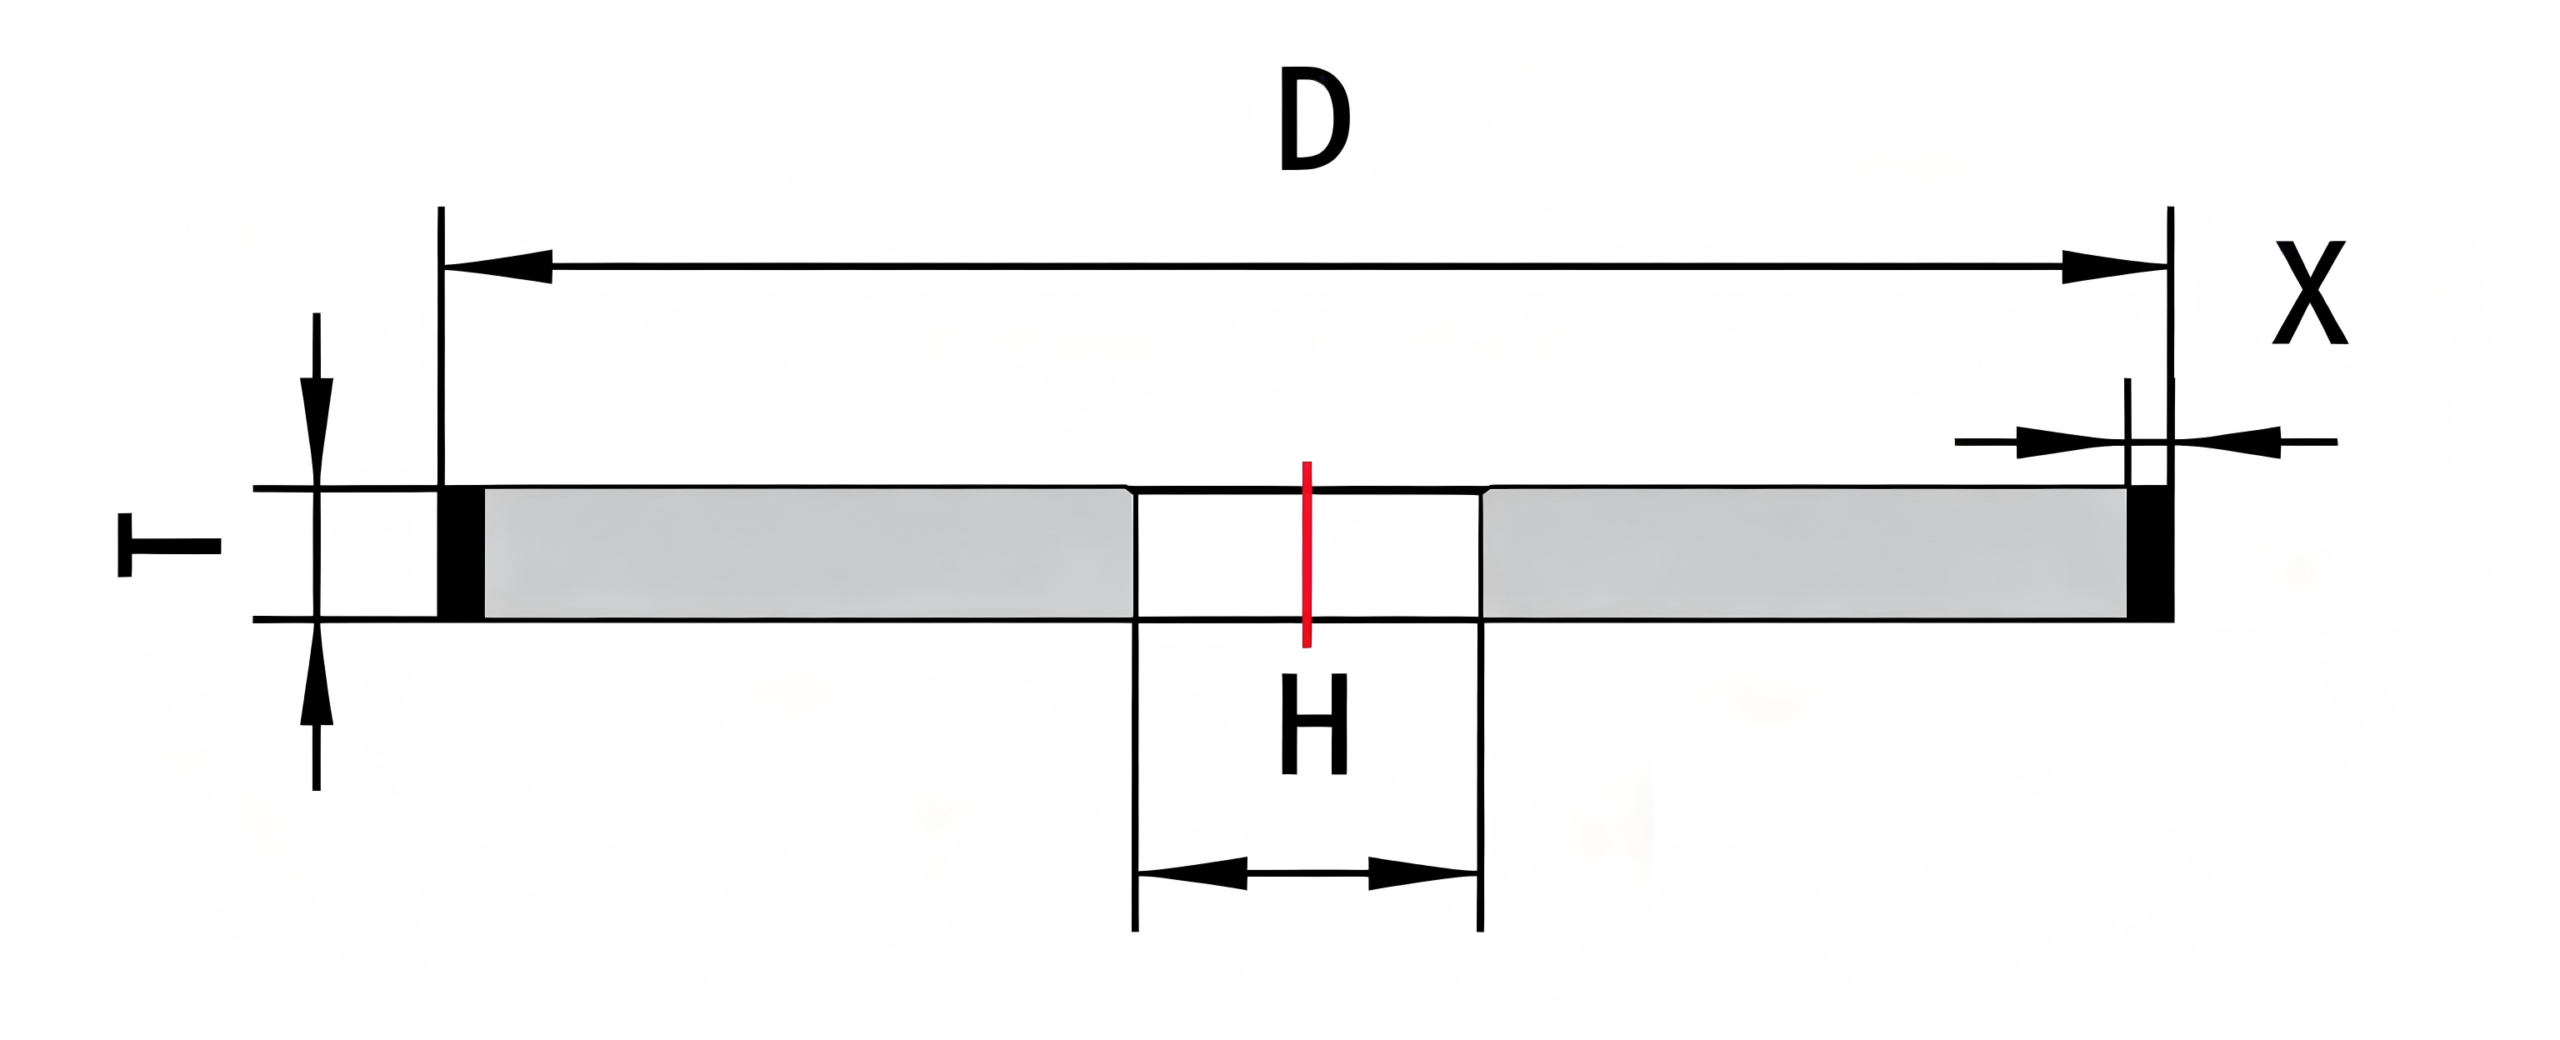
1A1 1A1 wheel drawing Small straight wheel for ID and jig grinding
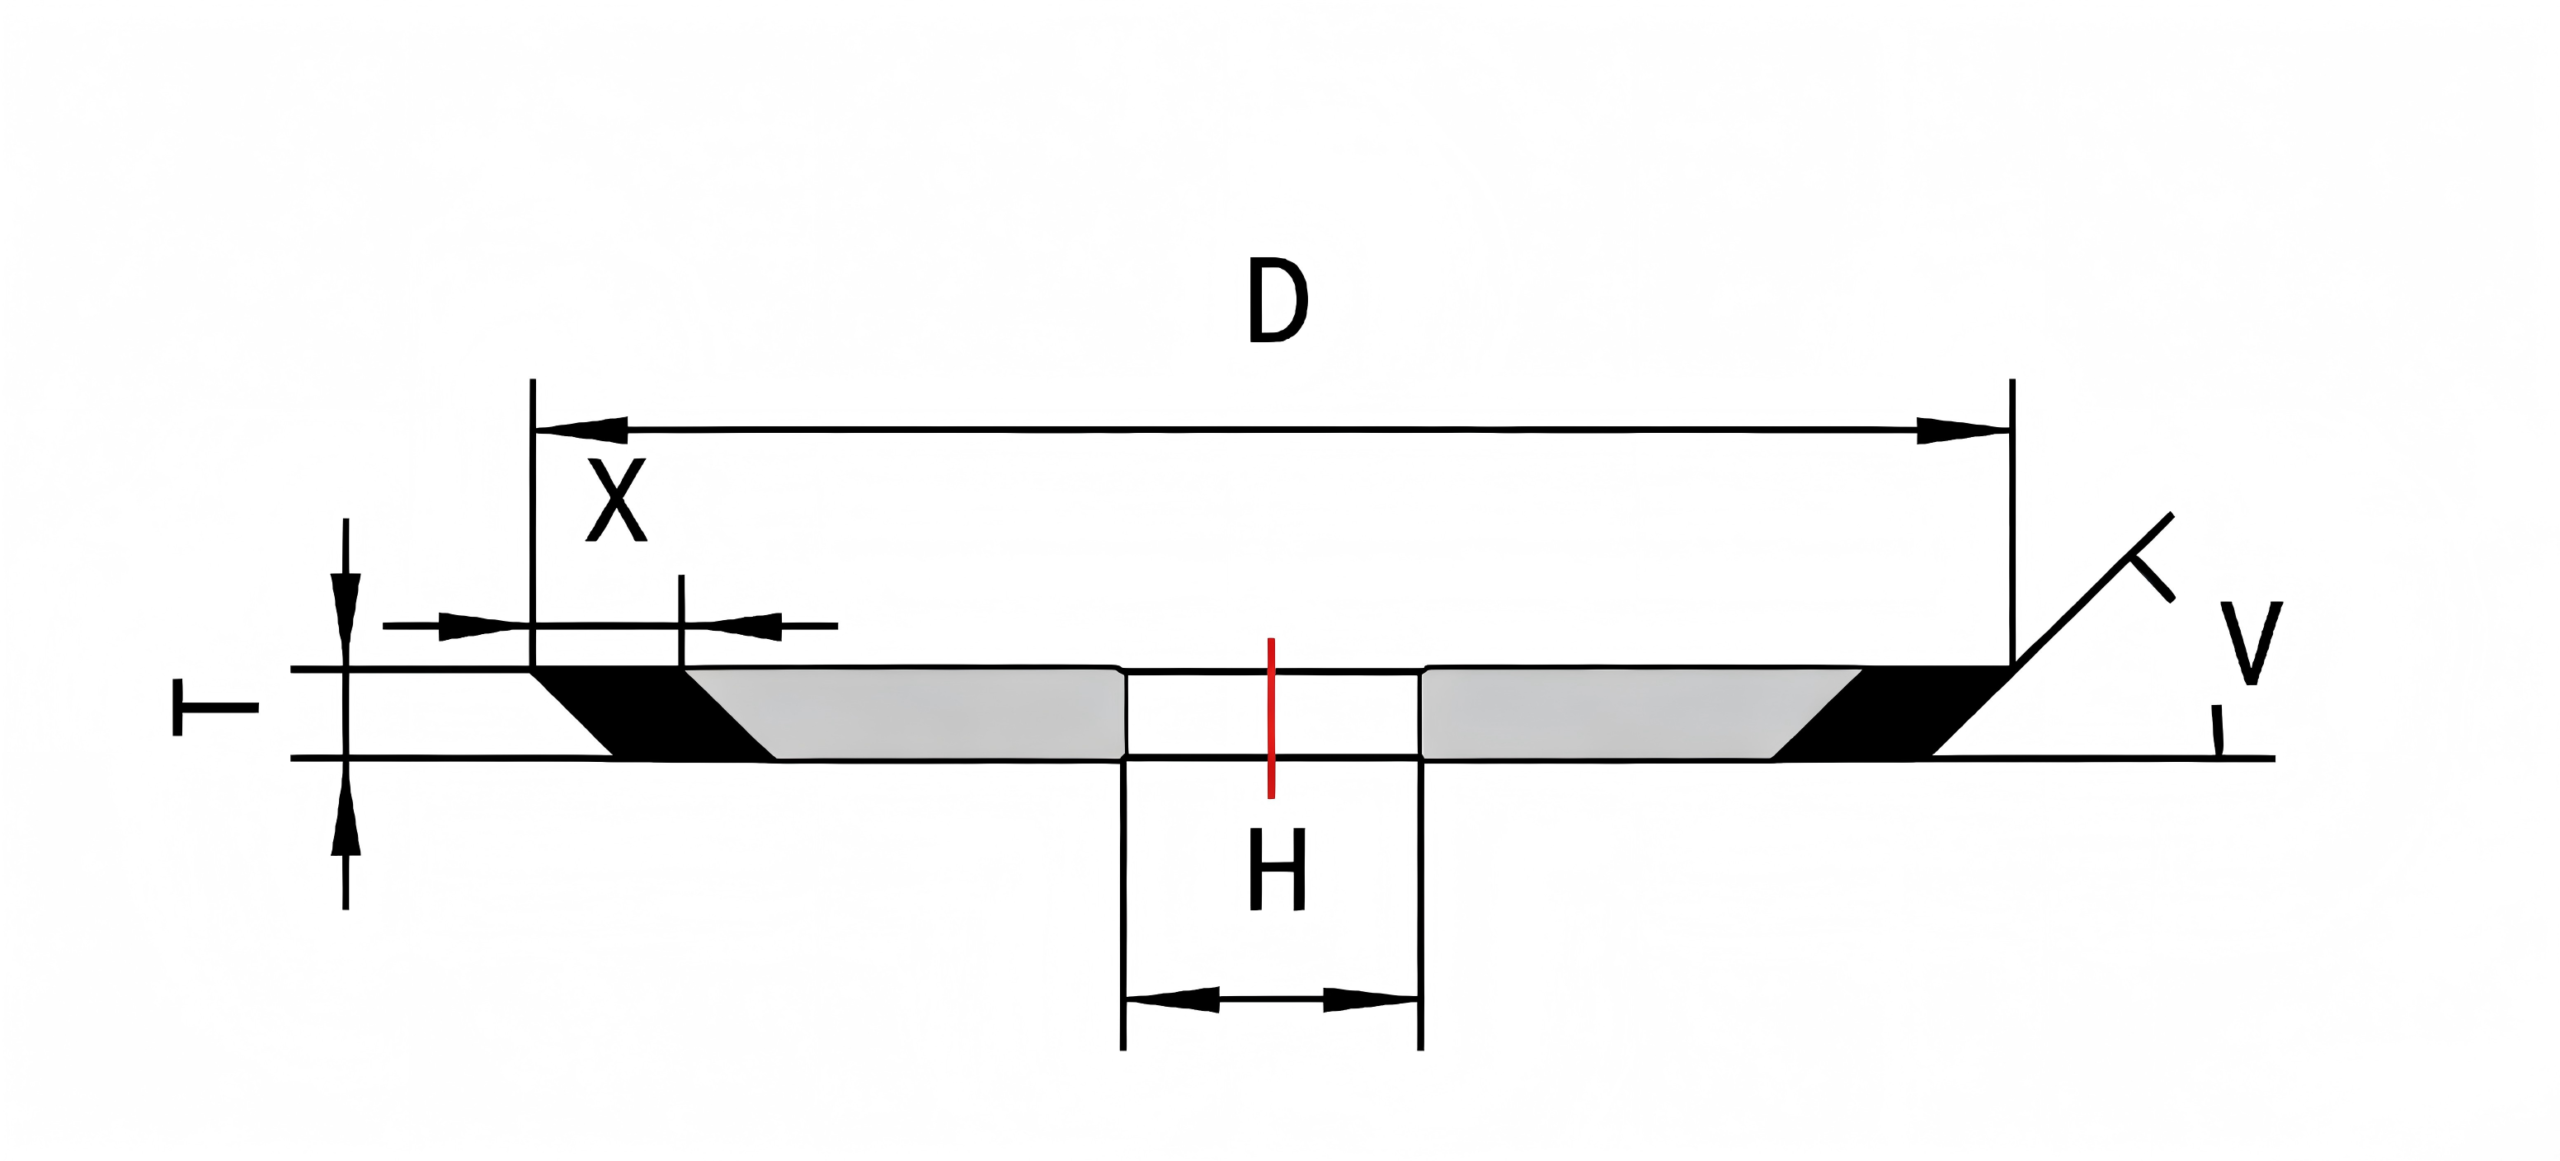
1V1 1V1 wheel drawing Taper or a formed cut in the bore when the stamp is already 1V1

A shank-mounted form is made to drawing.

Send a mark such as 1A1-20-6-6 or 1V1-16-4-6, plus bore size, diamond or CBN, material, and wet/dry. We match diameter, thickness, shank or hole, and grit.
When electroplated jig / internal is the wrong wheel

Related Products

Request a Quote