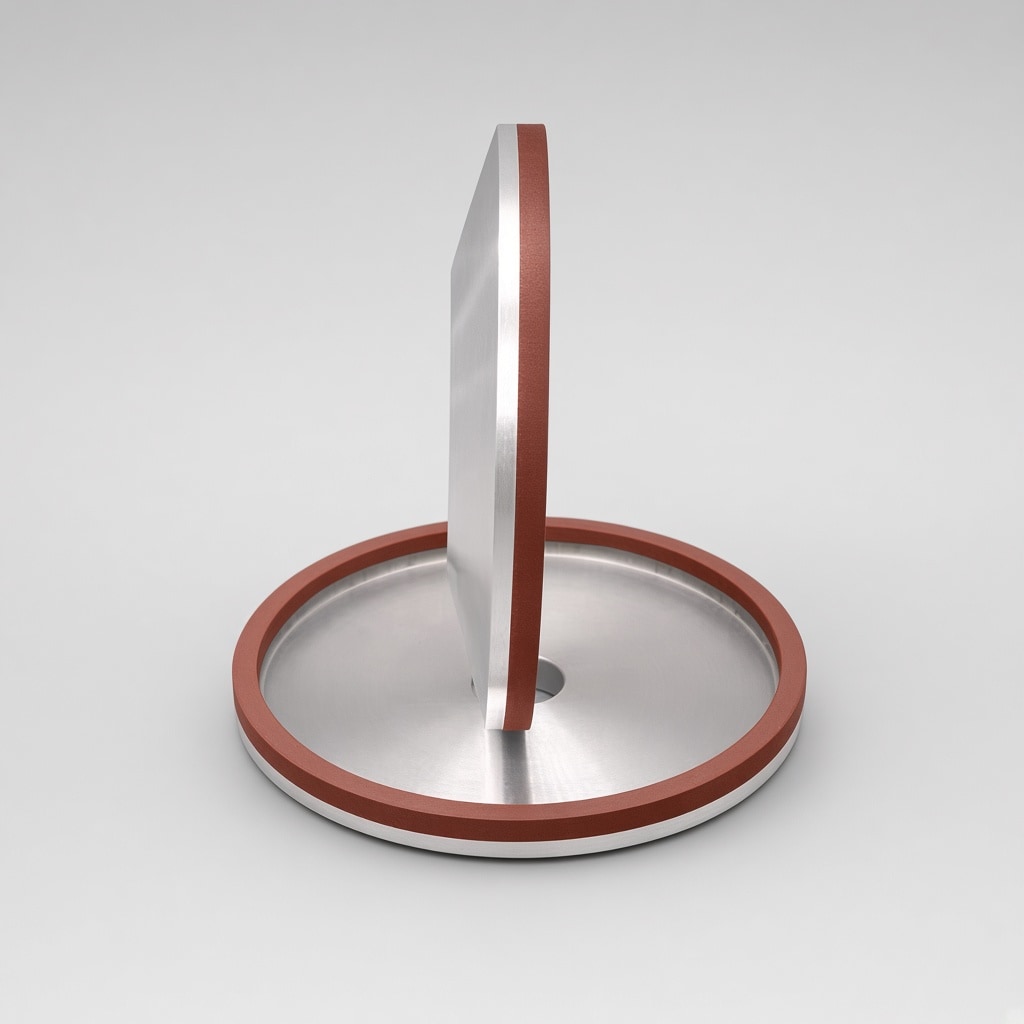
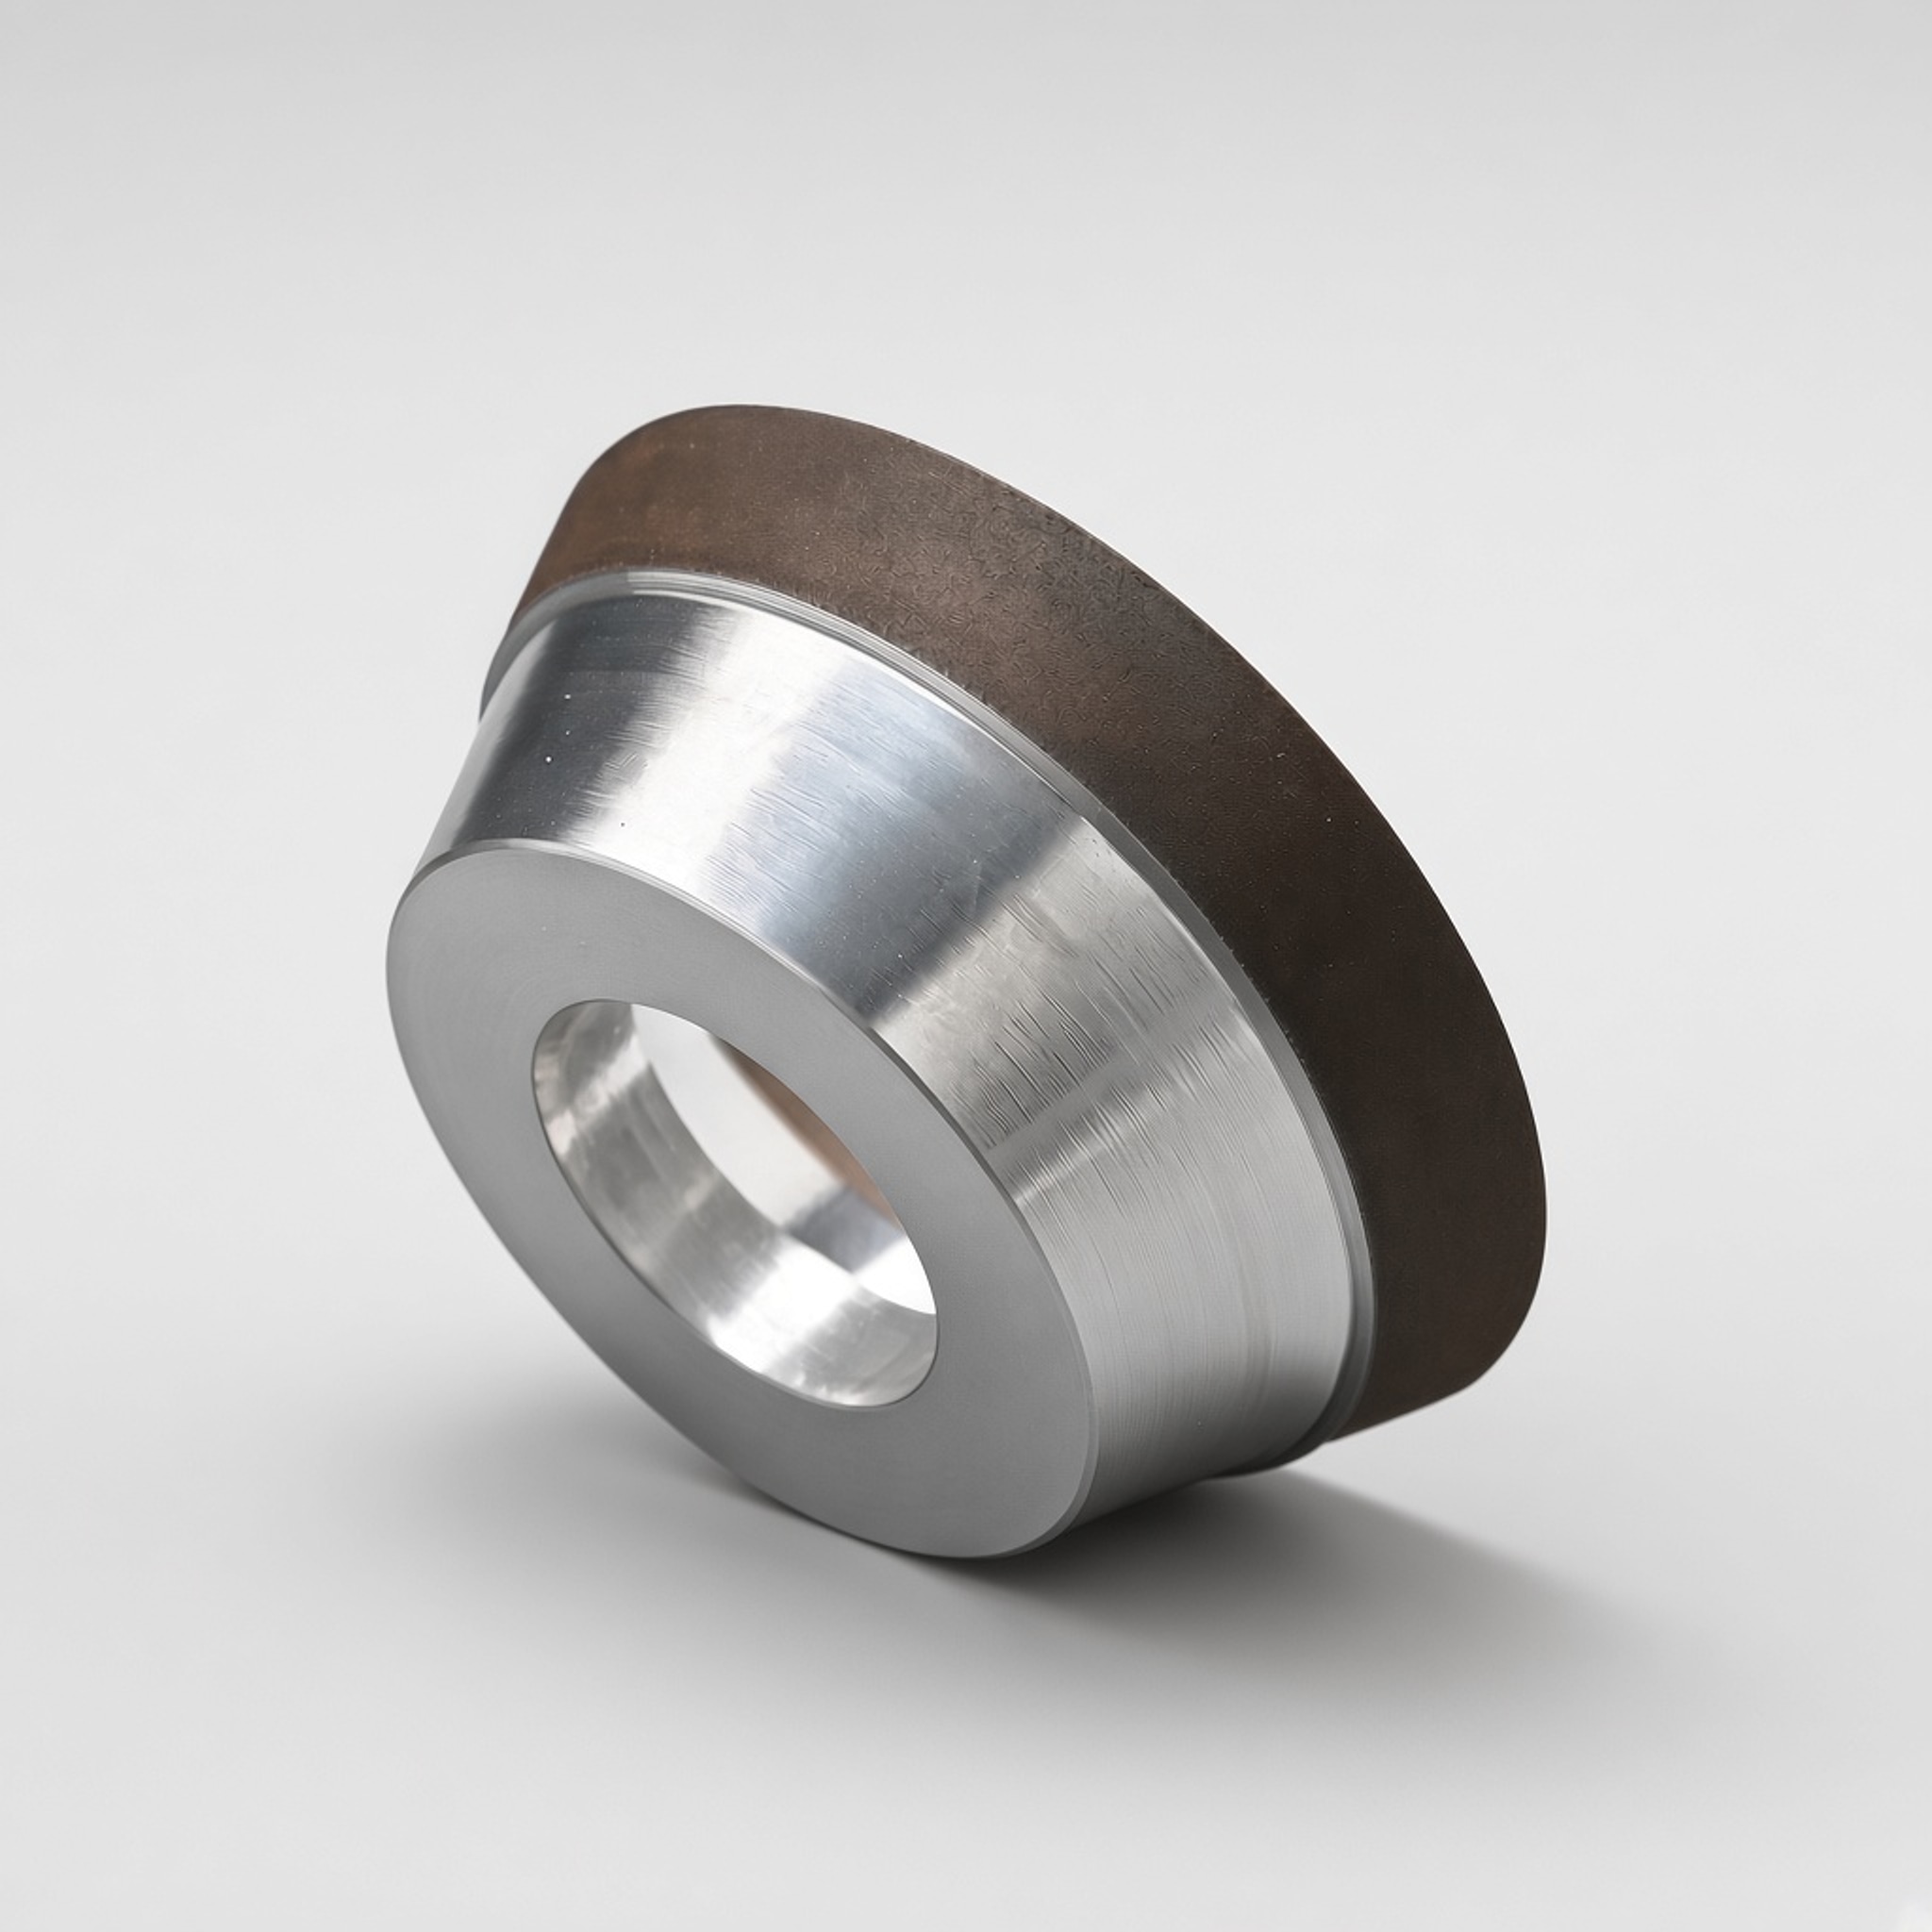
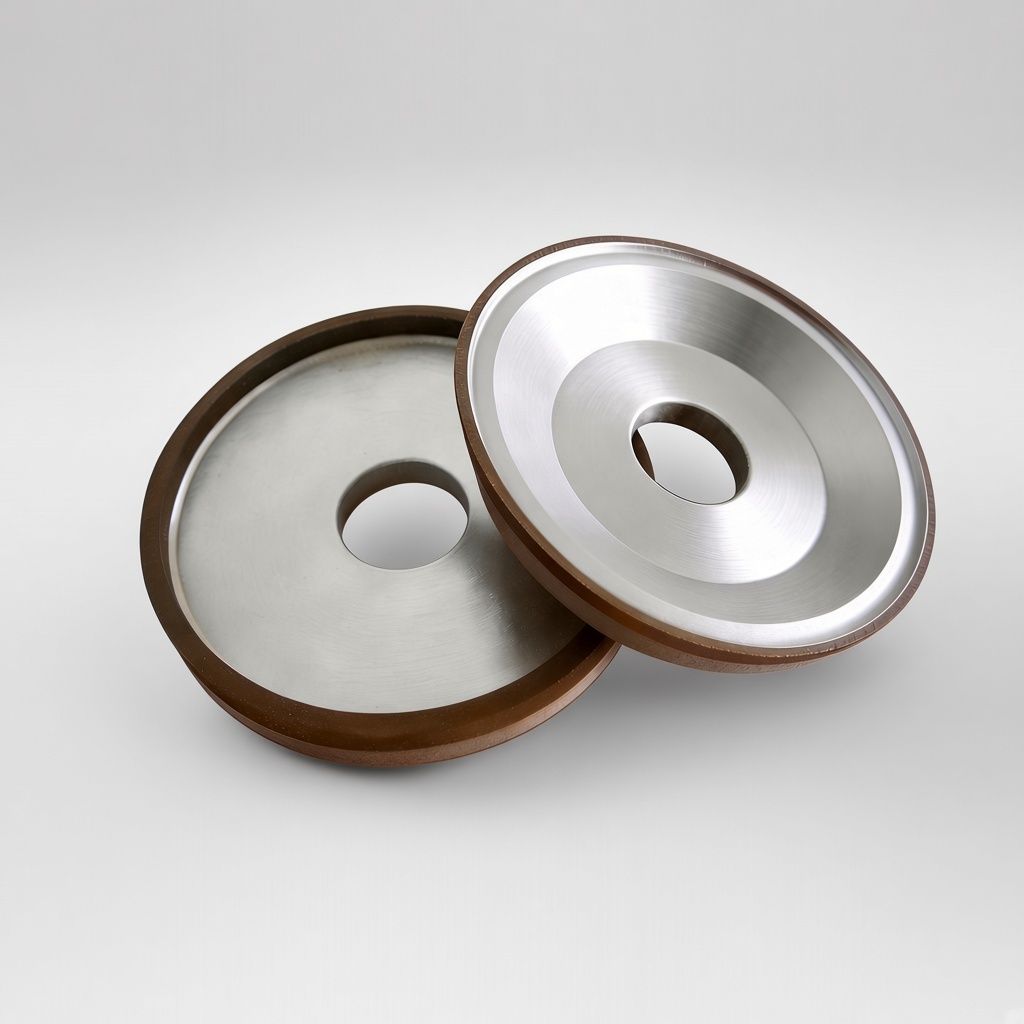
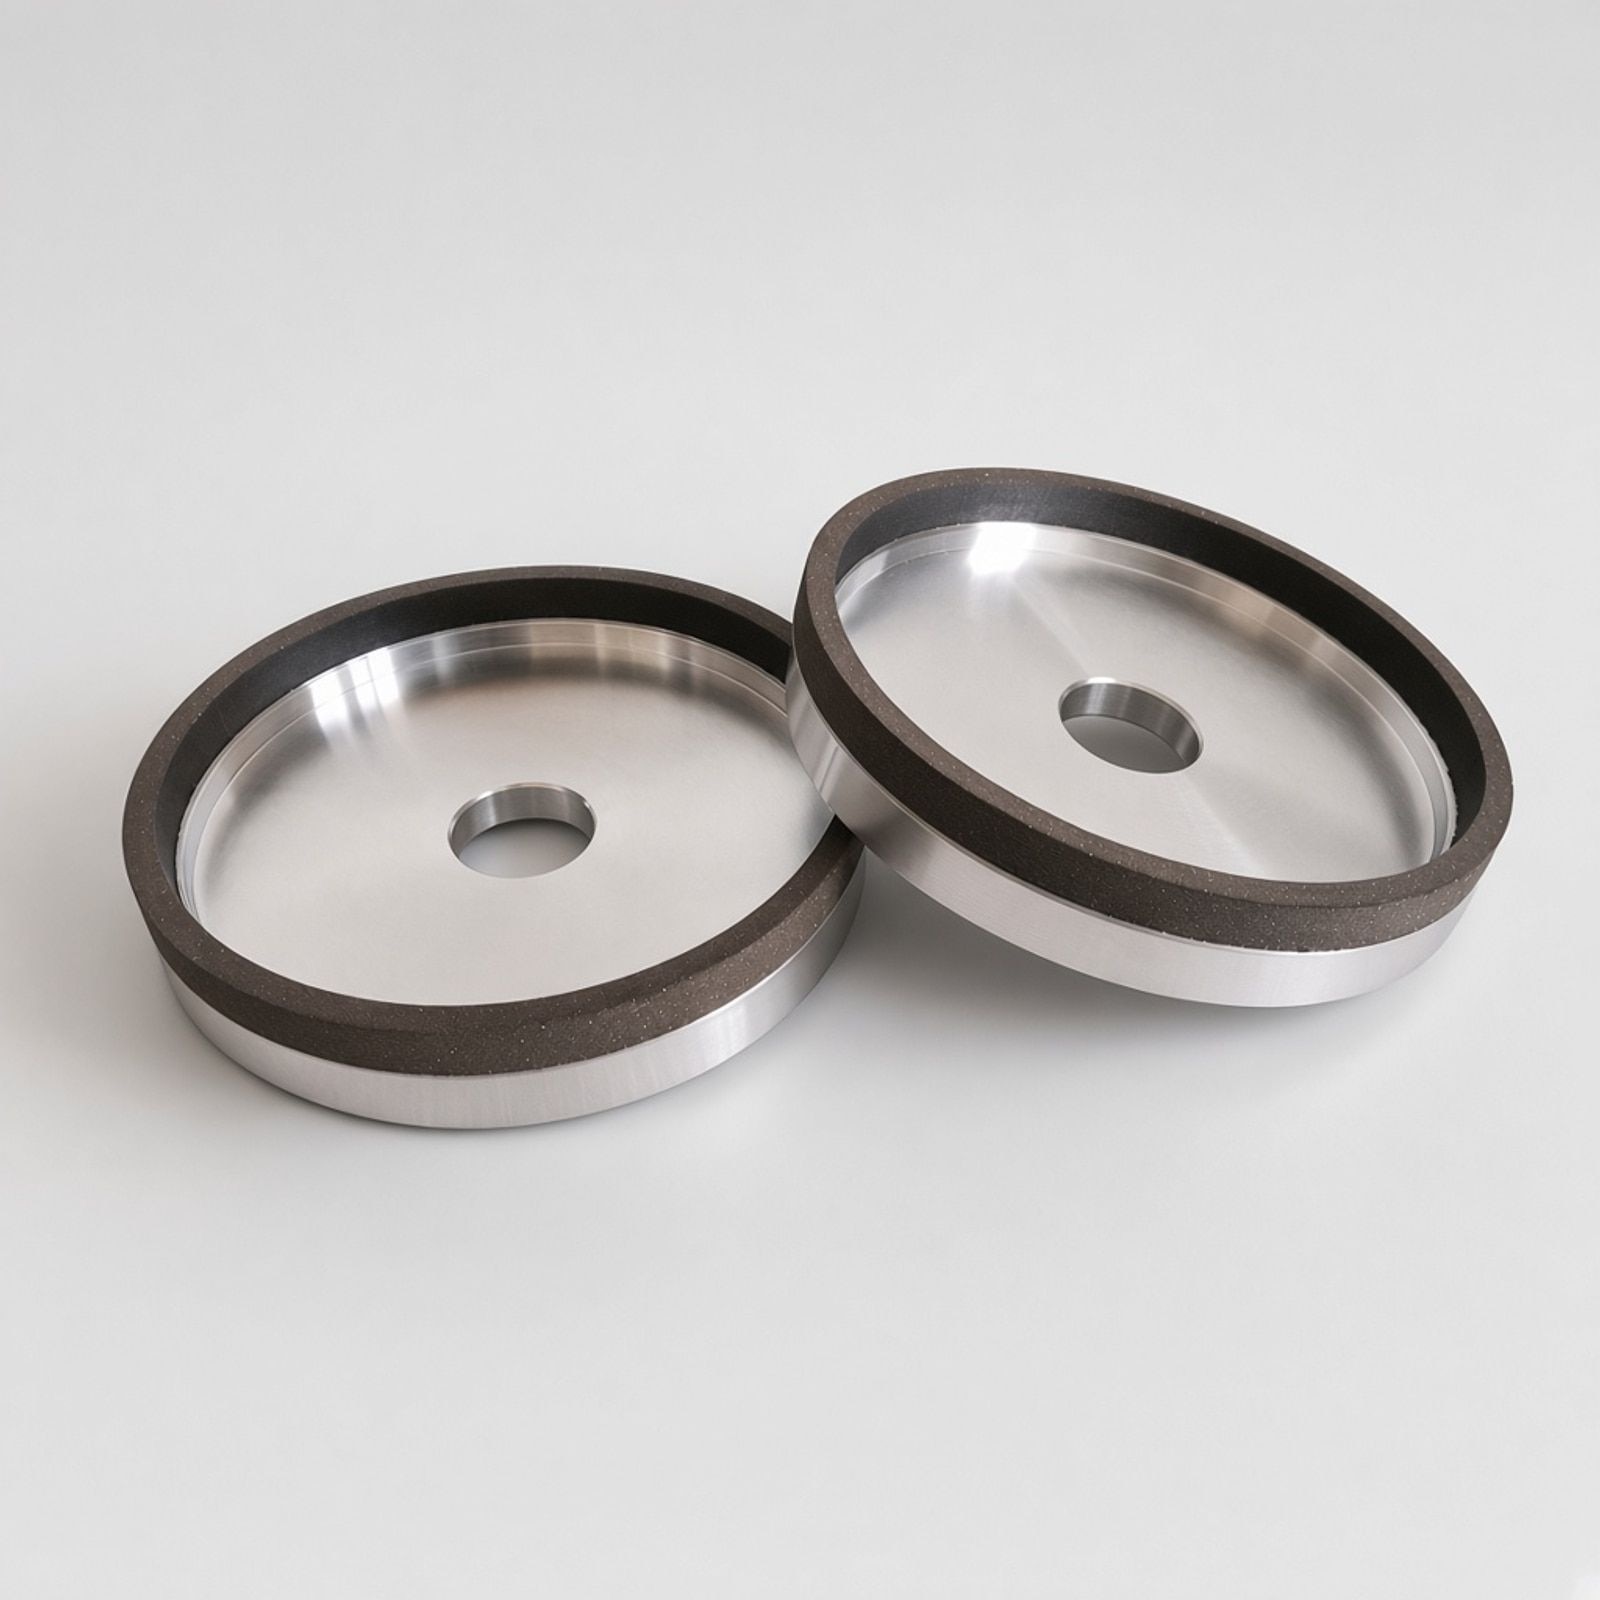
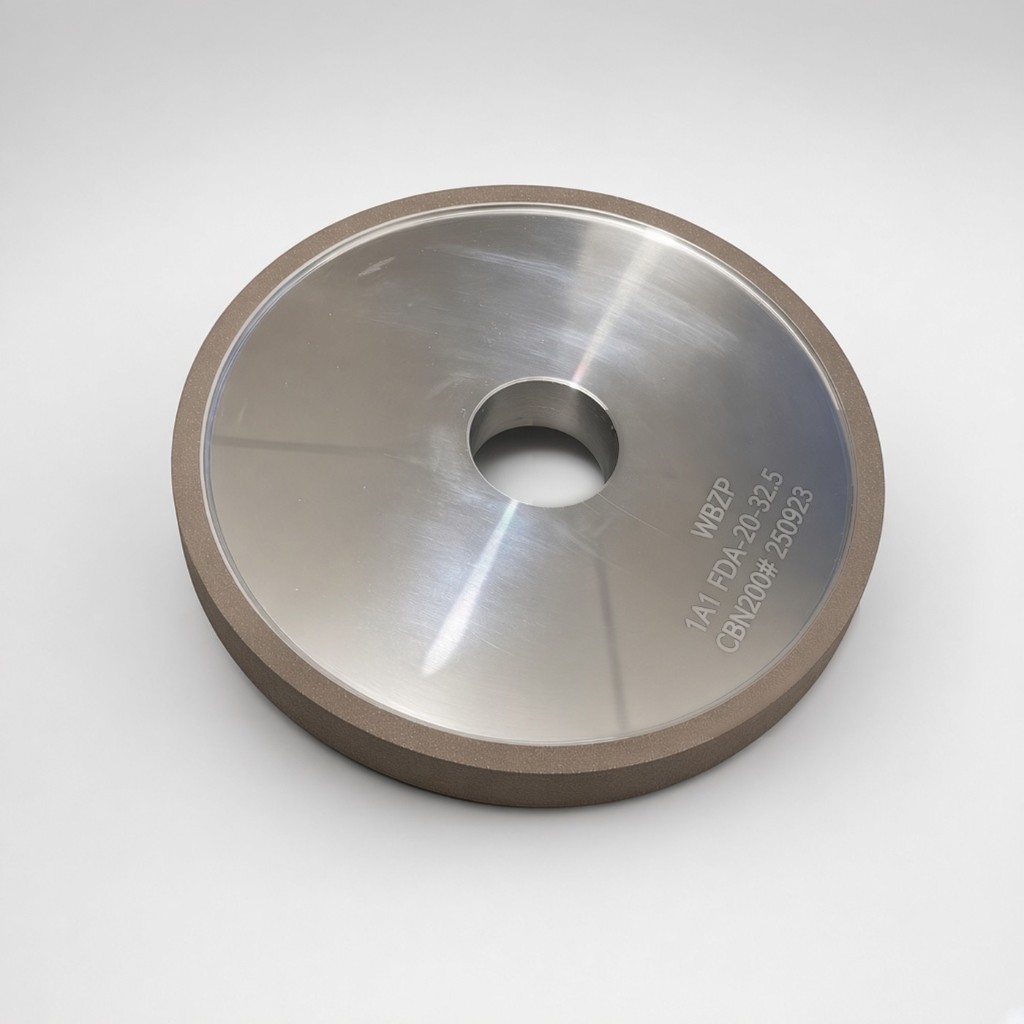
Resin Bond Diamond Wheels for Carbide Cutting Tools
- Cool cutting with low loading on CNC tool grinders
- Fine finish on flutes, clearances, and OD
- Diamond abrasive for tungsten carbide
- Made to your diameter, grit, and concentration
Product Information
Overview
Resin bond diamond wheels grind cemented carbide cutting tools — end mills, drills, reamers, and inserts. The bond self-sharpens, keeps heat low, and delivers a fine surface on flutes and edges.
Typical machines: Walter, ANCA, Rollomatic, and equivalent CNC tool grinders. Diamond resin is for carbide; hardened steel or HSS needs CBN.
Typical Workpieces
| Workpiece | Common operations |
|---|---|
| Solid carbide end mills | Flute grinding, OD, end cutting edge |
| Carbide drills & reamers | Flute, point, clearance |
| Carbide inserts / tips | Face, periphery, clearance |
| Carbide saw blades & router bits | Tooth / flute grinding |
| Carbide dies & form tools | Profile and clearance grinding |
Shapes
| Shape | Drawing | Role on carbide tools |
|---|---|---|
| 11V9 | ![]() |
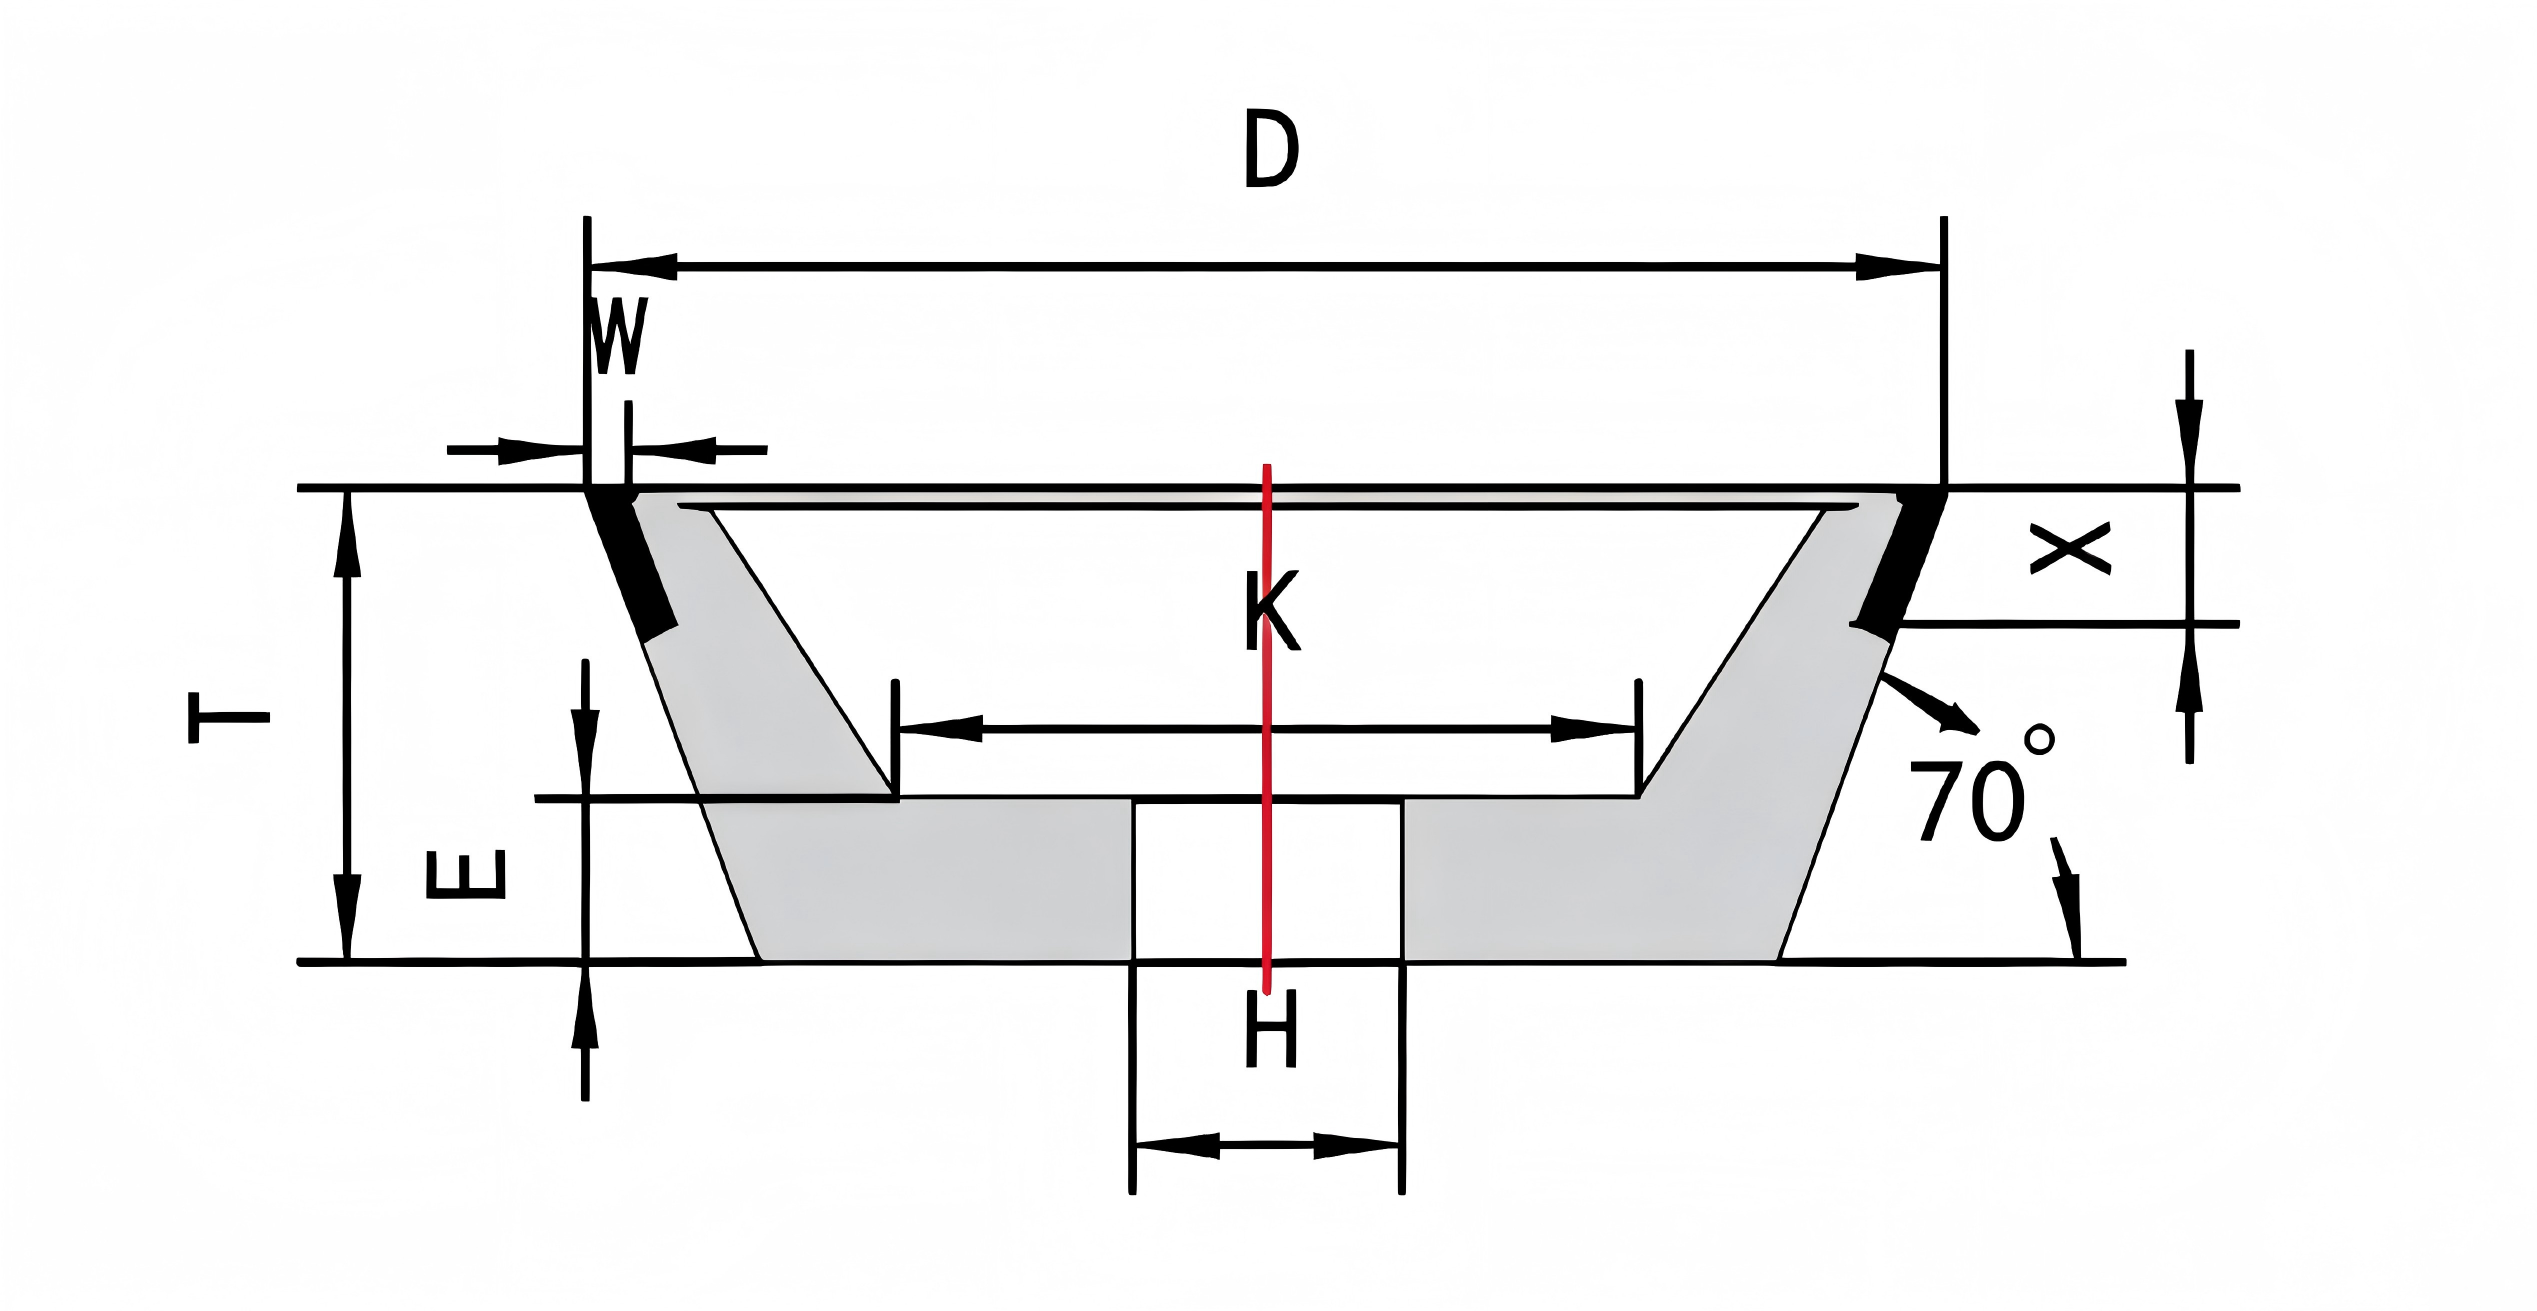
Flute grinding — the most requested dish wheel on tool grinders |
| 12V9 | ![]() |
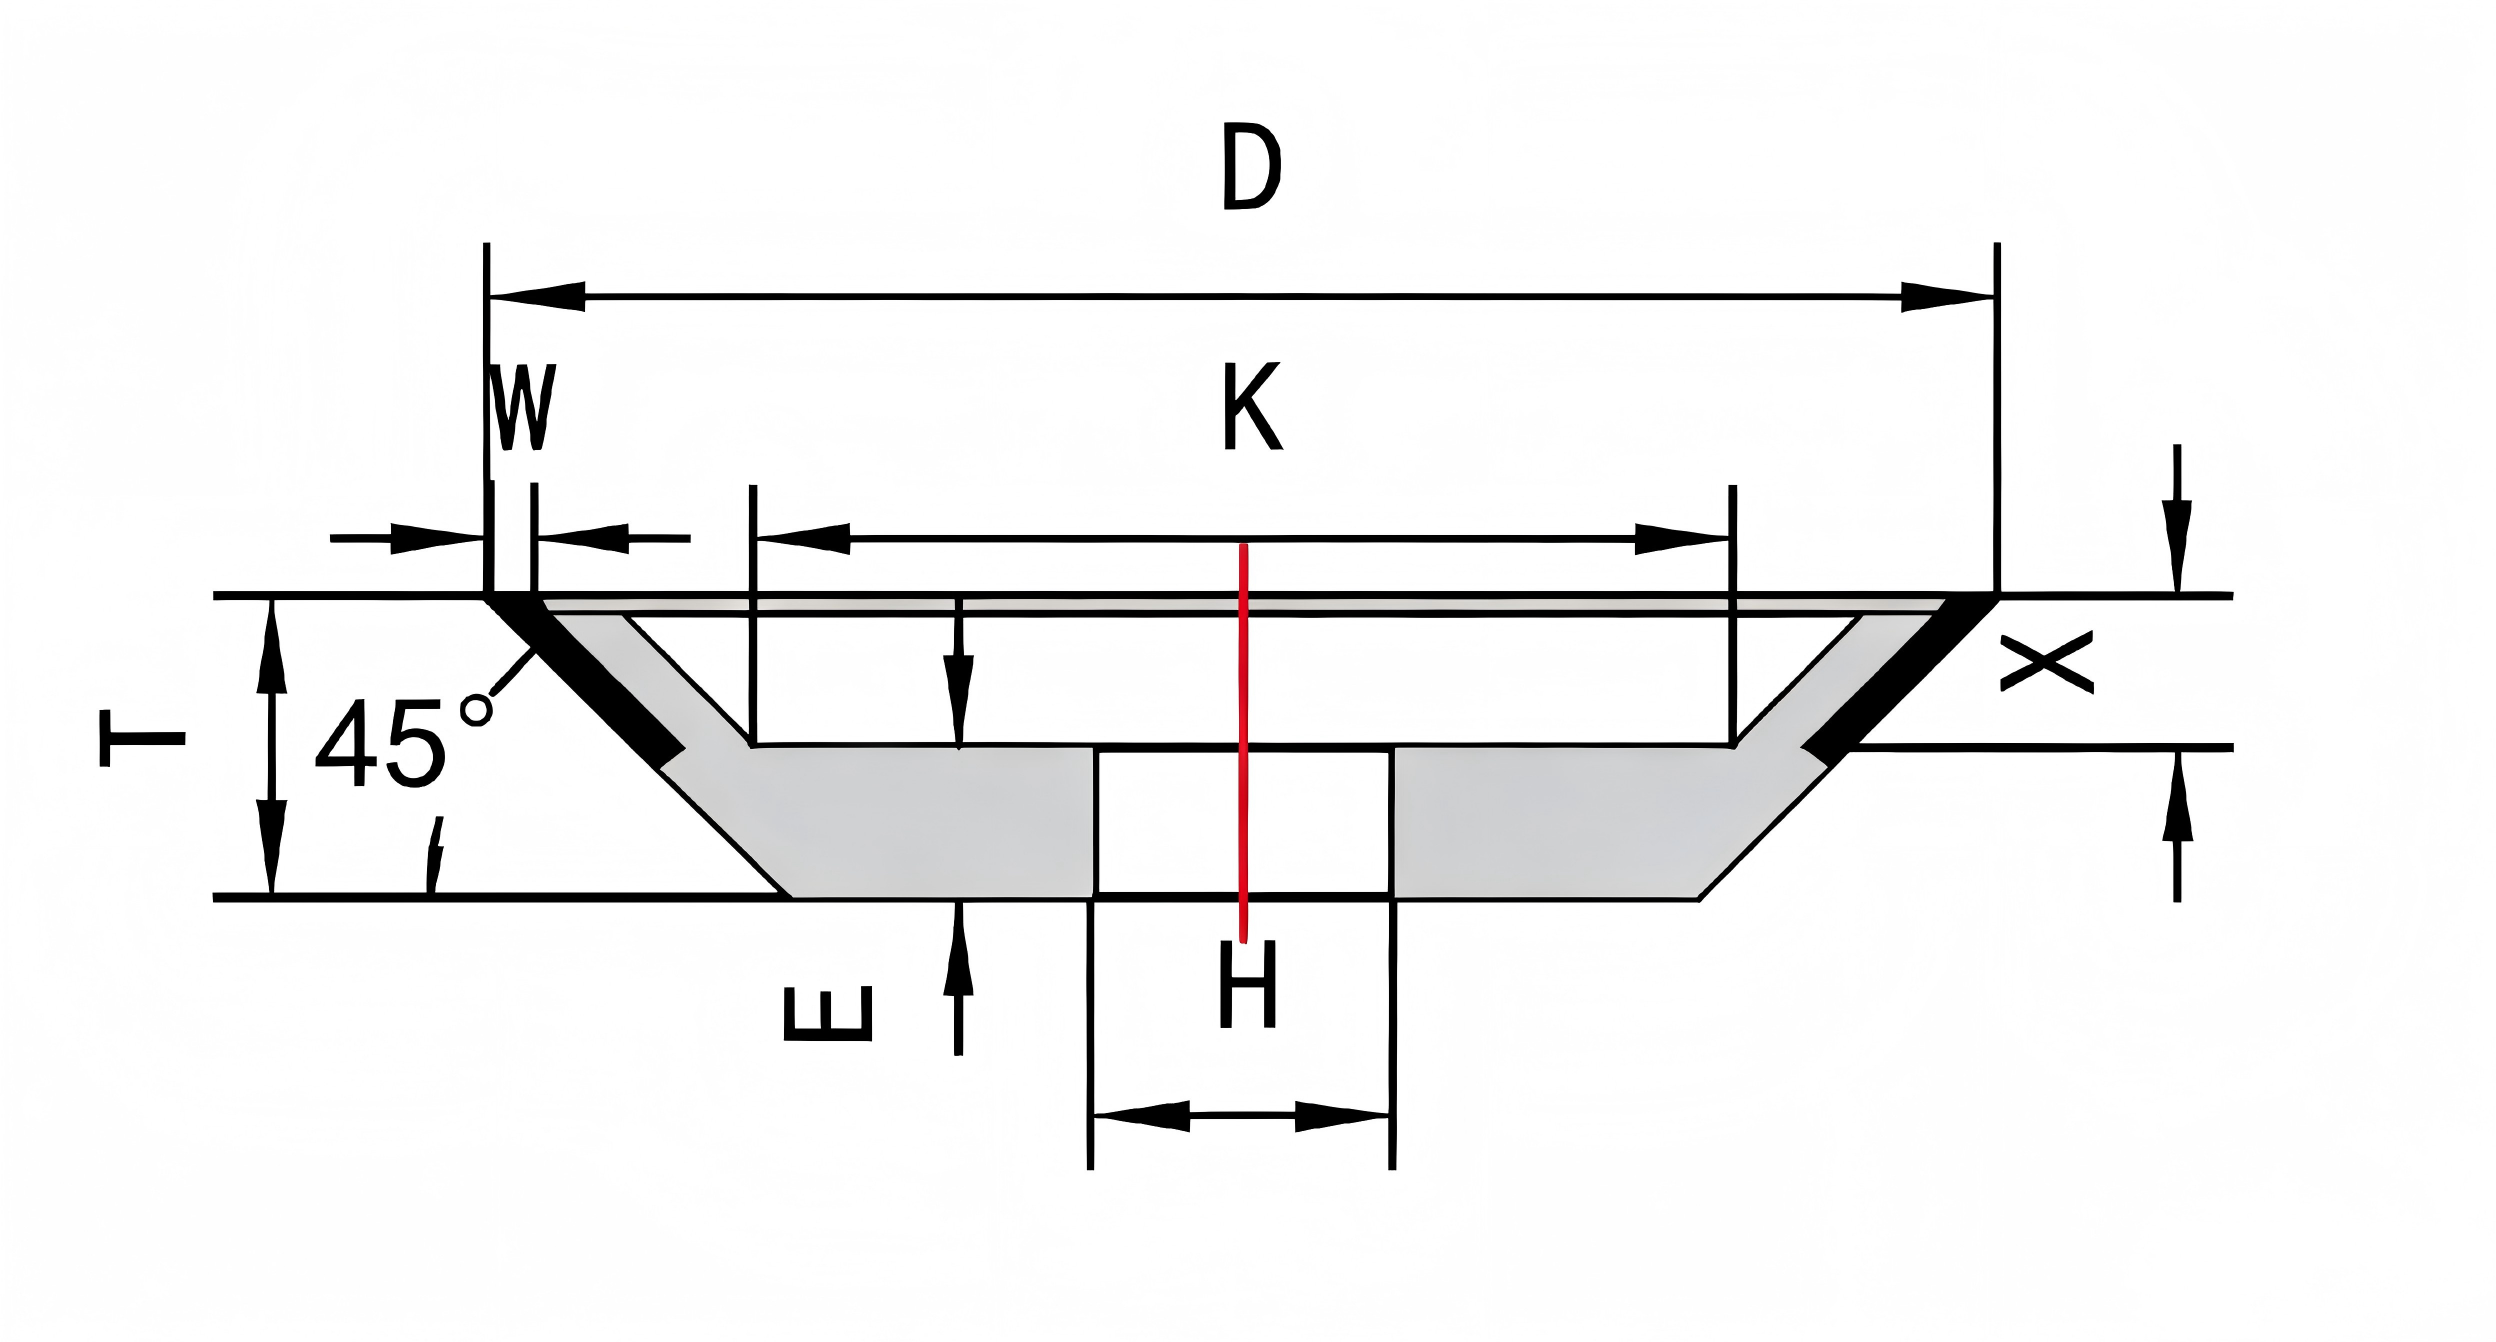
Flute and clearance; angled dish for tighter geometry |
| 6A2 | ![]() |
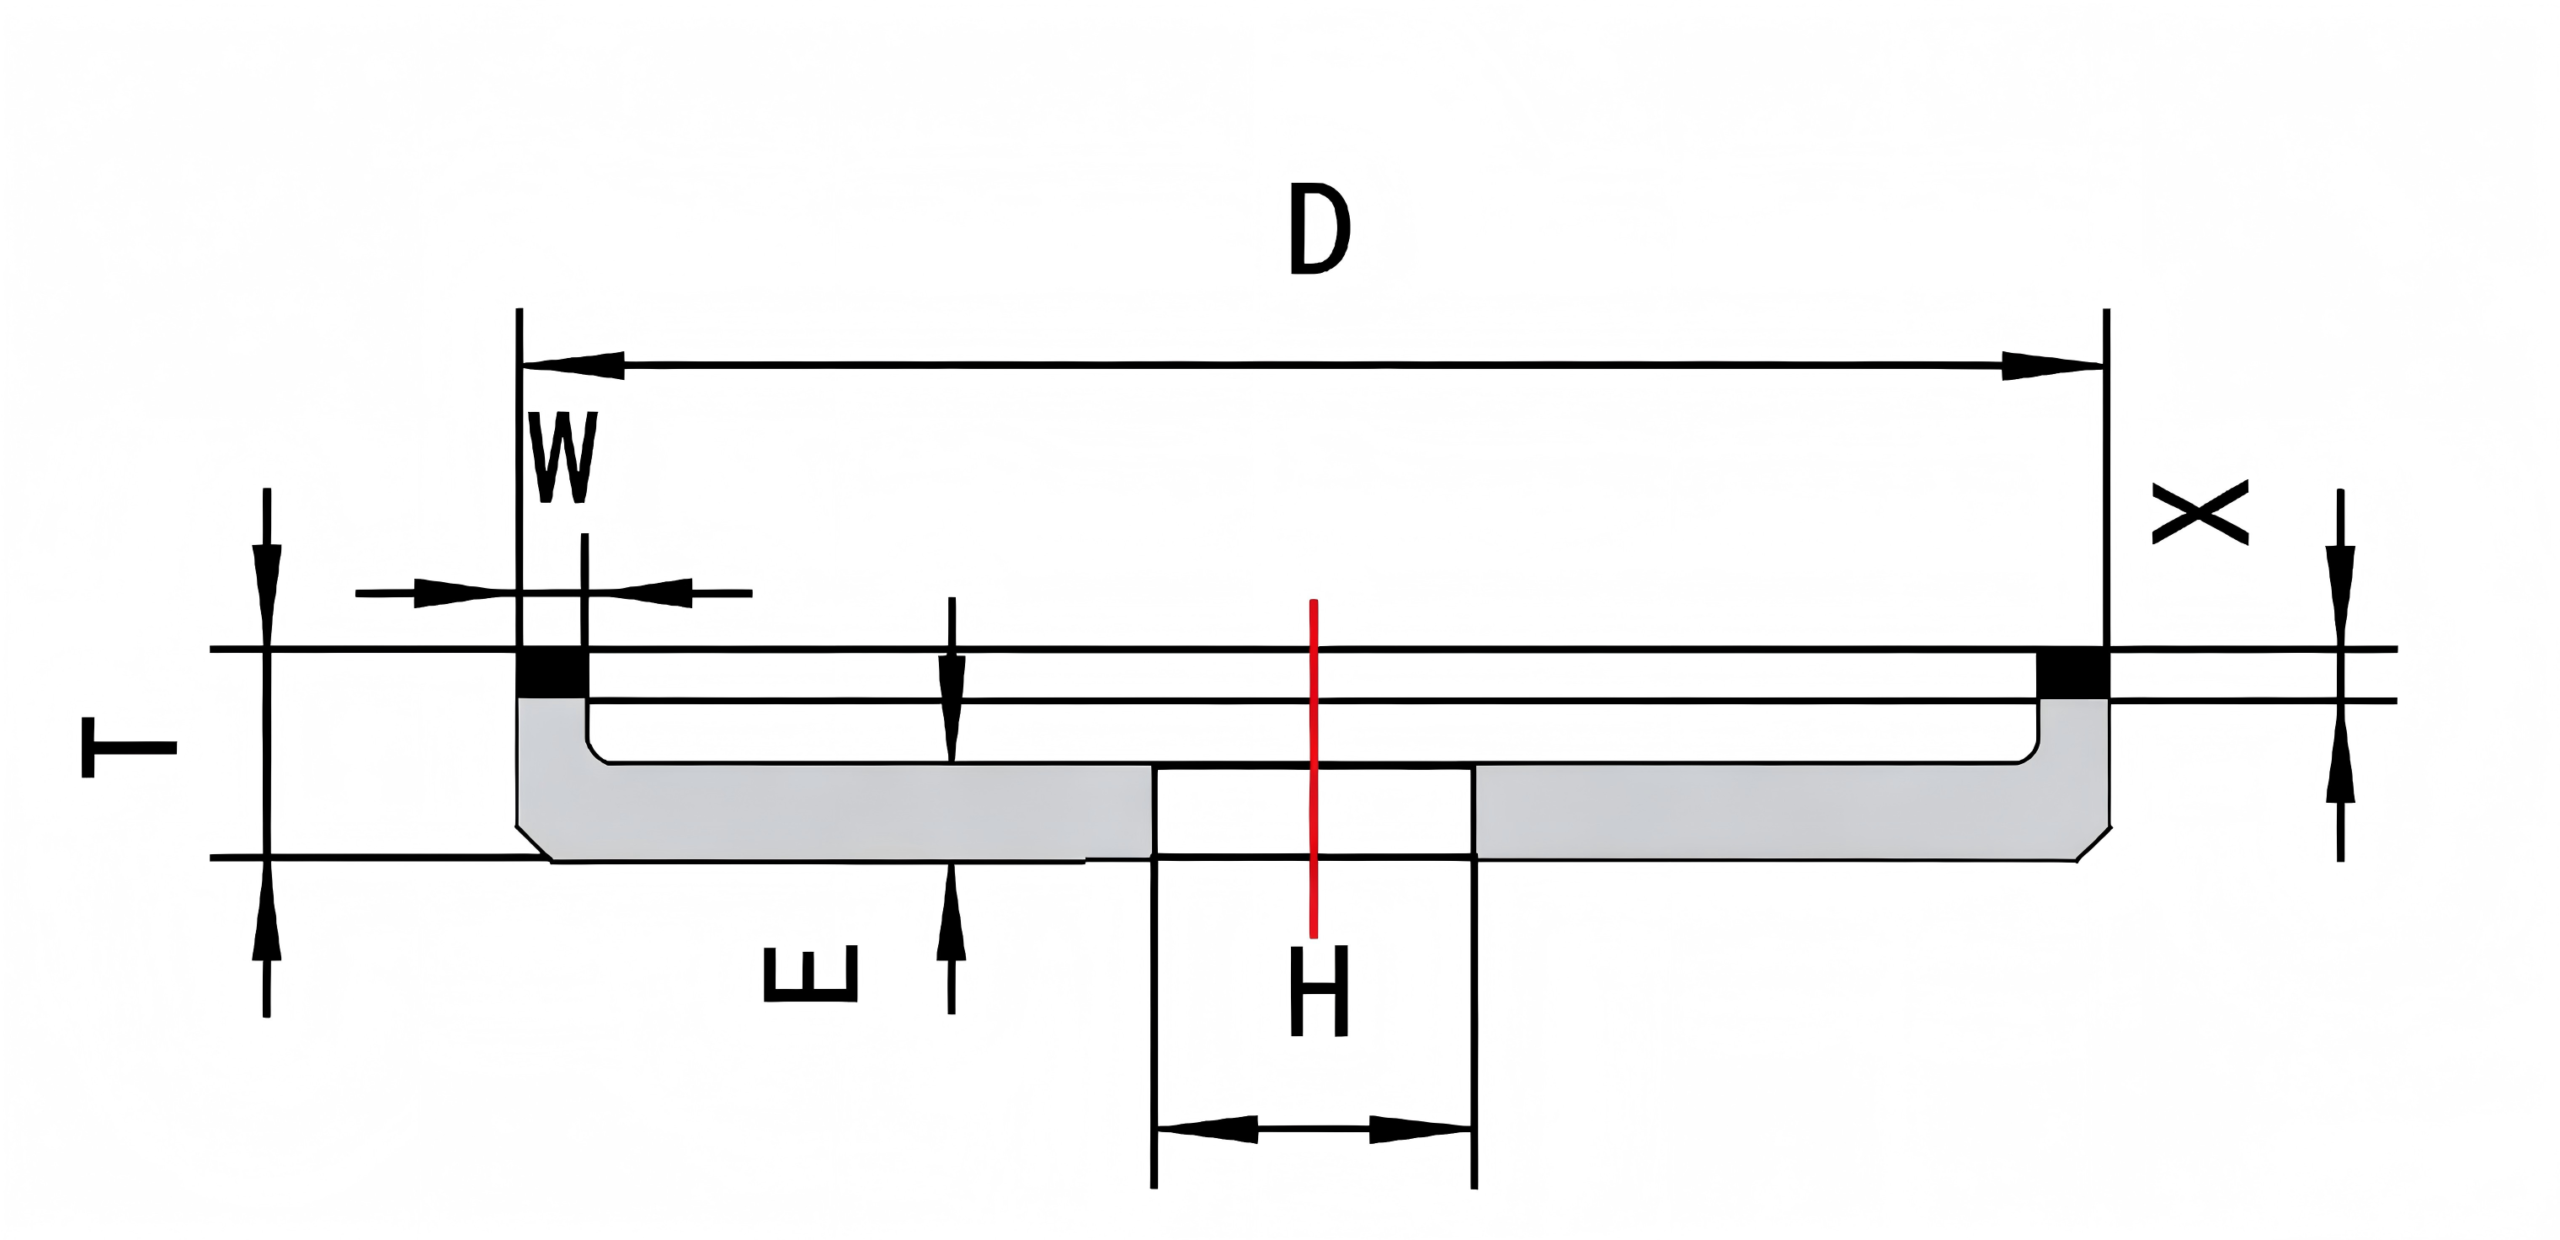
Clearance and cup grinding on faces and flanks |
| 1A1 | ![]() |
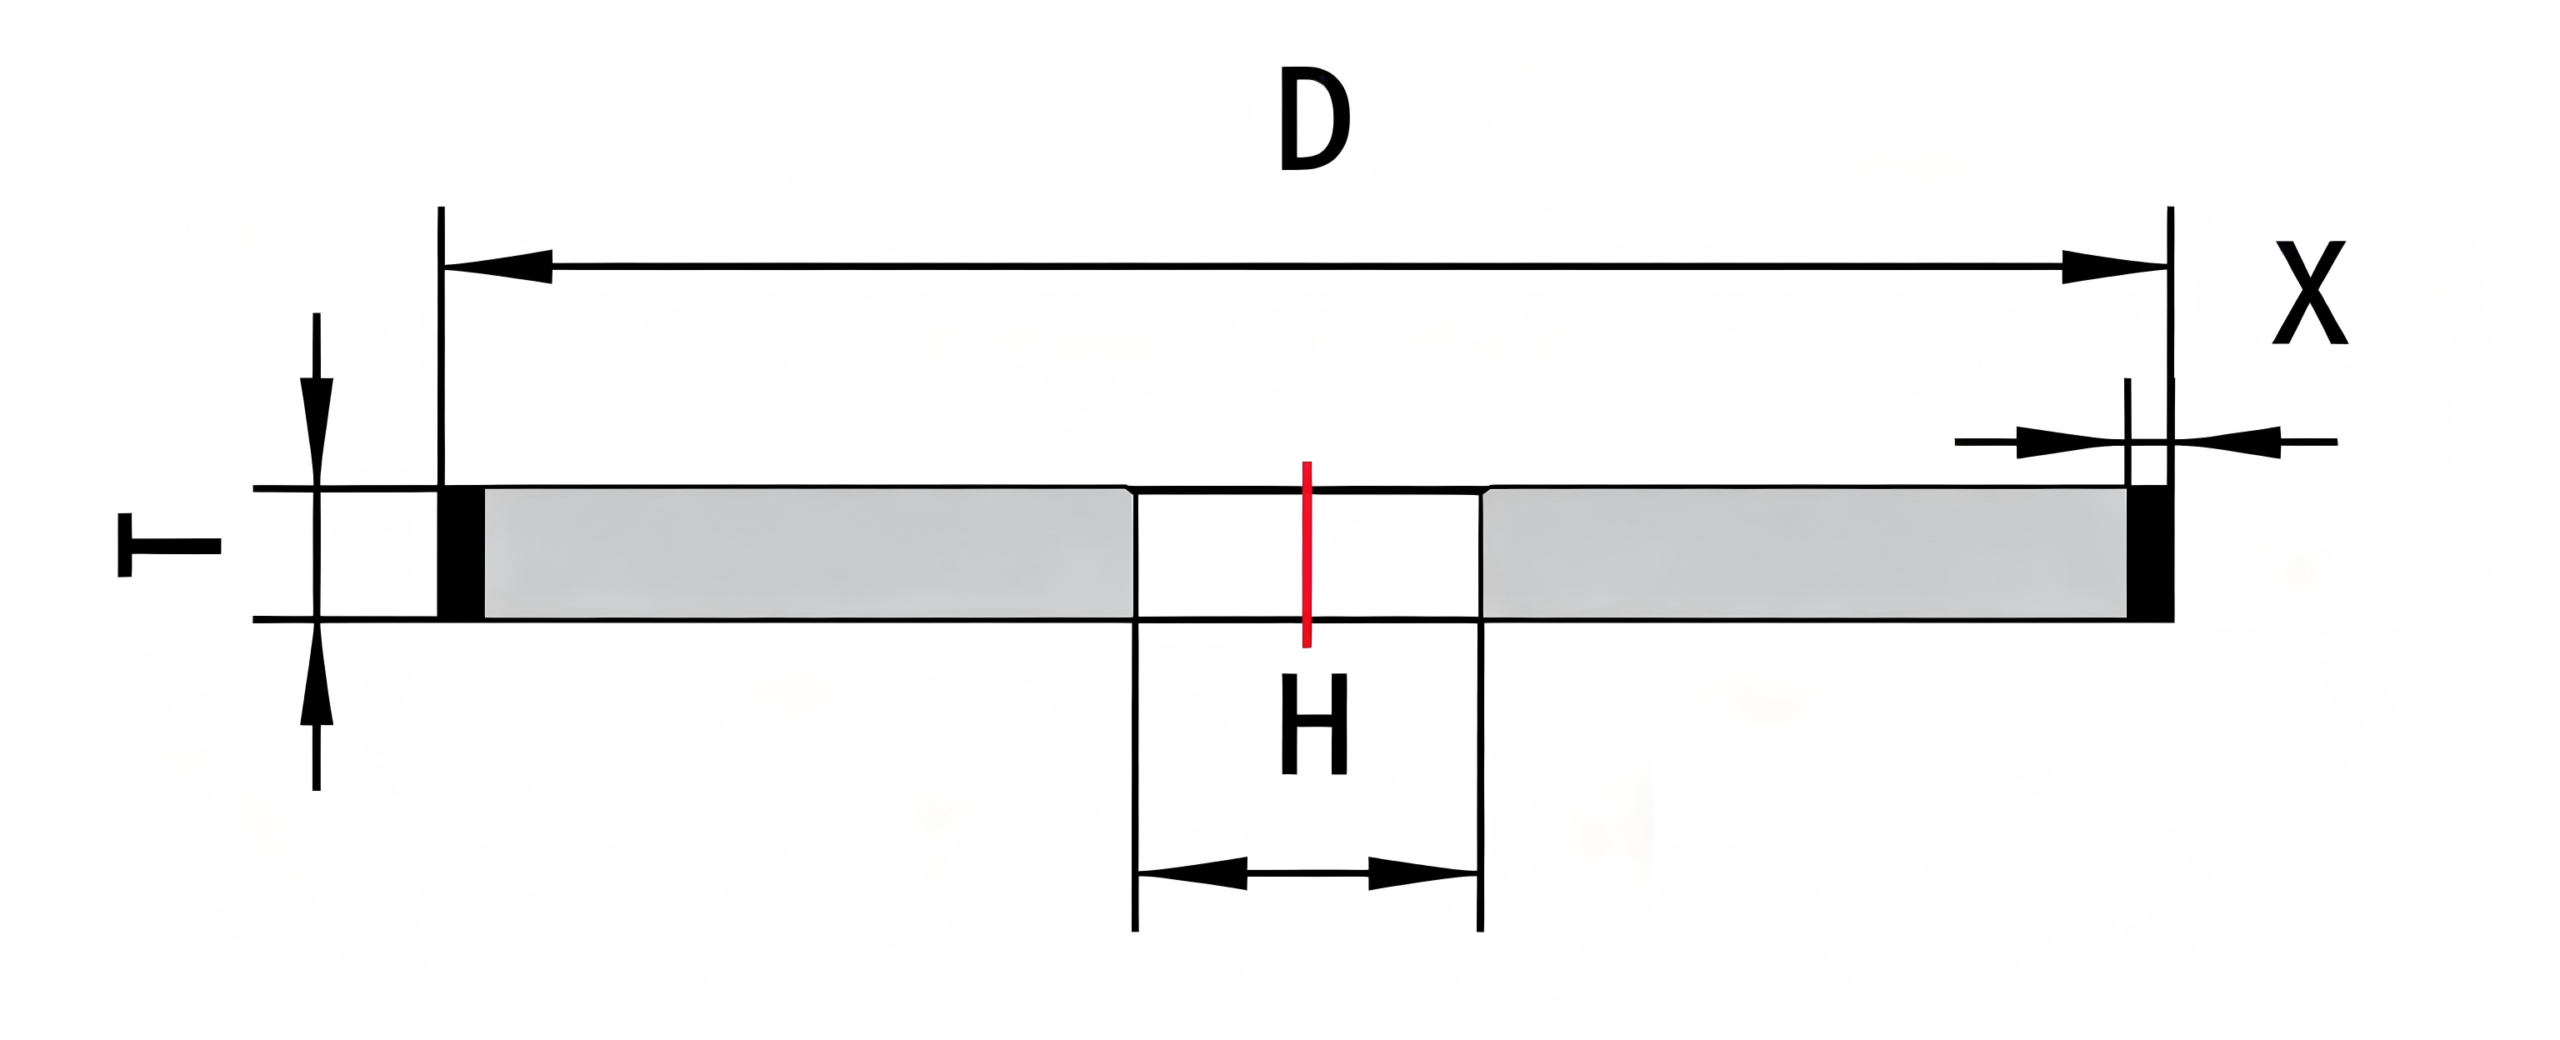
OD and cylindrical grinding of shanks and tool bodies |
Also available: 14V1 (root cleaning and deep flutes), 1V1 (narrow slots and clearances), 4A2, 3A1.
Send your current wheel mark (e.g. 11V9-100-2-20 D64 C75) or a drawing. We match diameter, thickness, hole, grit, and concentration to your machine and coolant.
When not to use resin bond
- Cutting glass, quartz, or LED substrates → metal or electroplated cut-off wheels (1A1R)
- Maximum wheel life with heavy wet grinding of brittle materials → metal bond
- High-volume carbide / PCD with dressing on a production line → vitrified diamond
- Grinding steel or HSS → CBN, not diamond