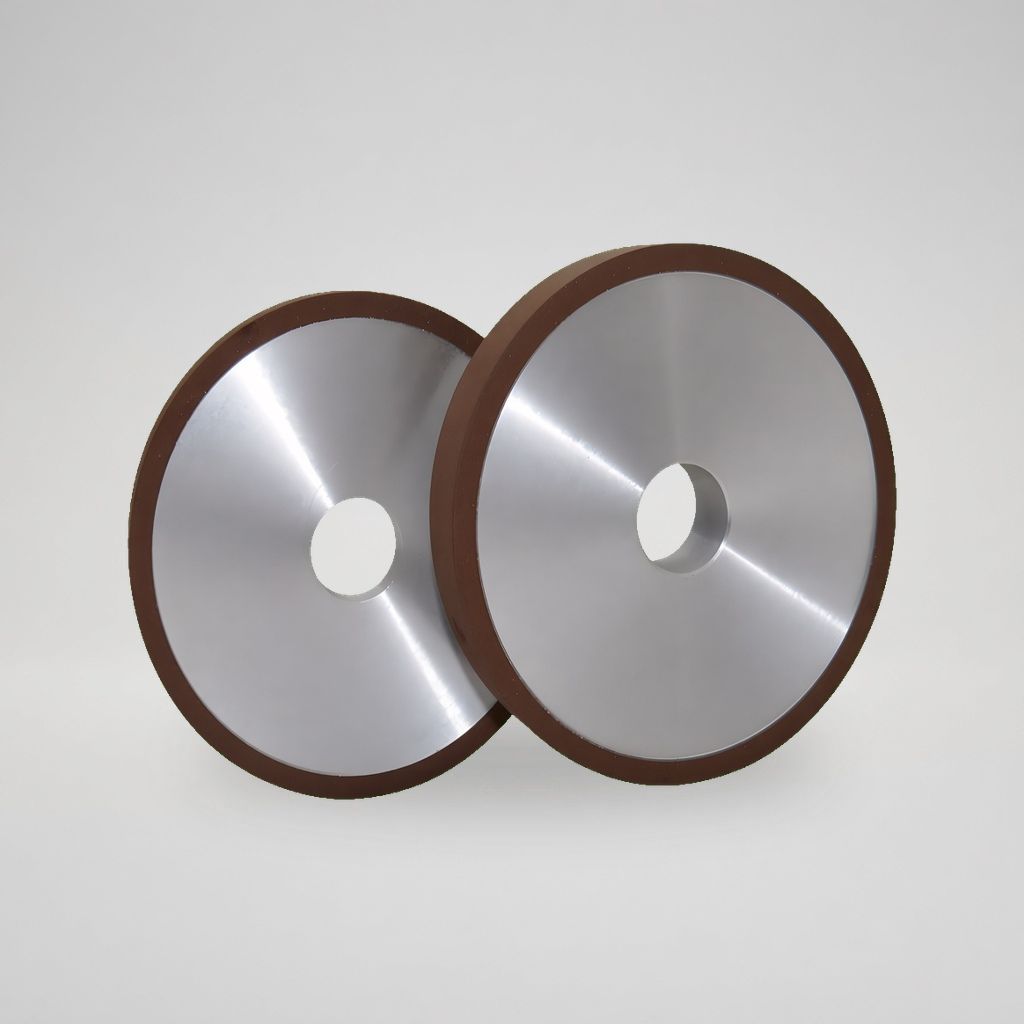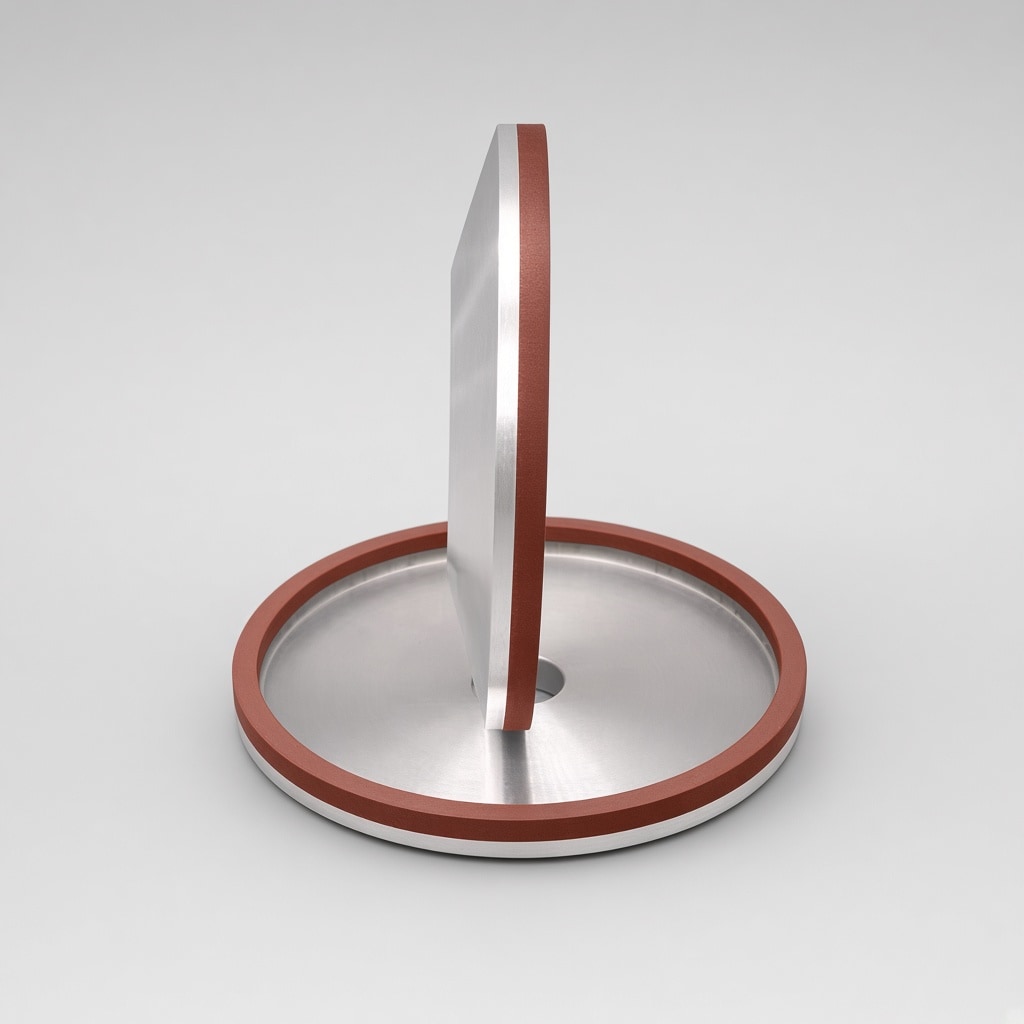
Resin Bond Diamond & CBN Wheels for Mold and Die
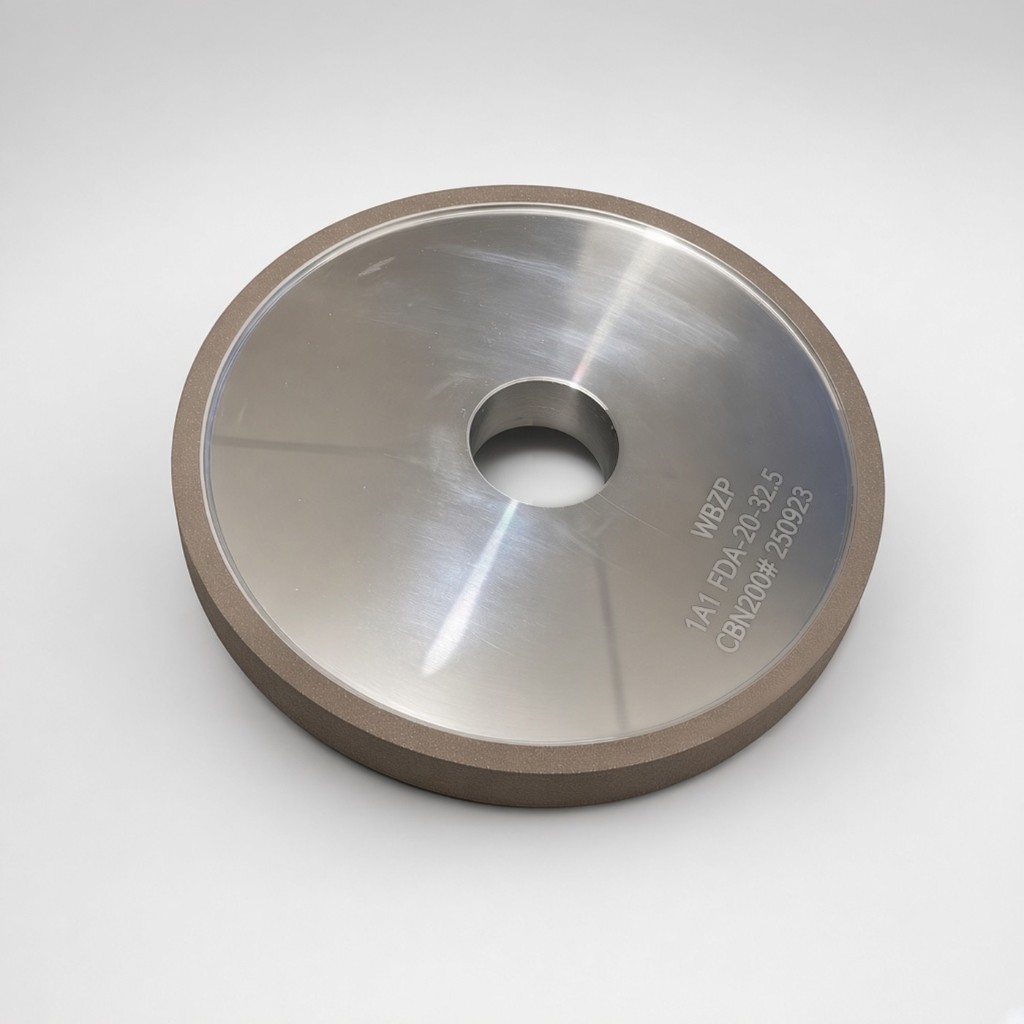
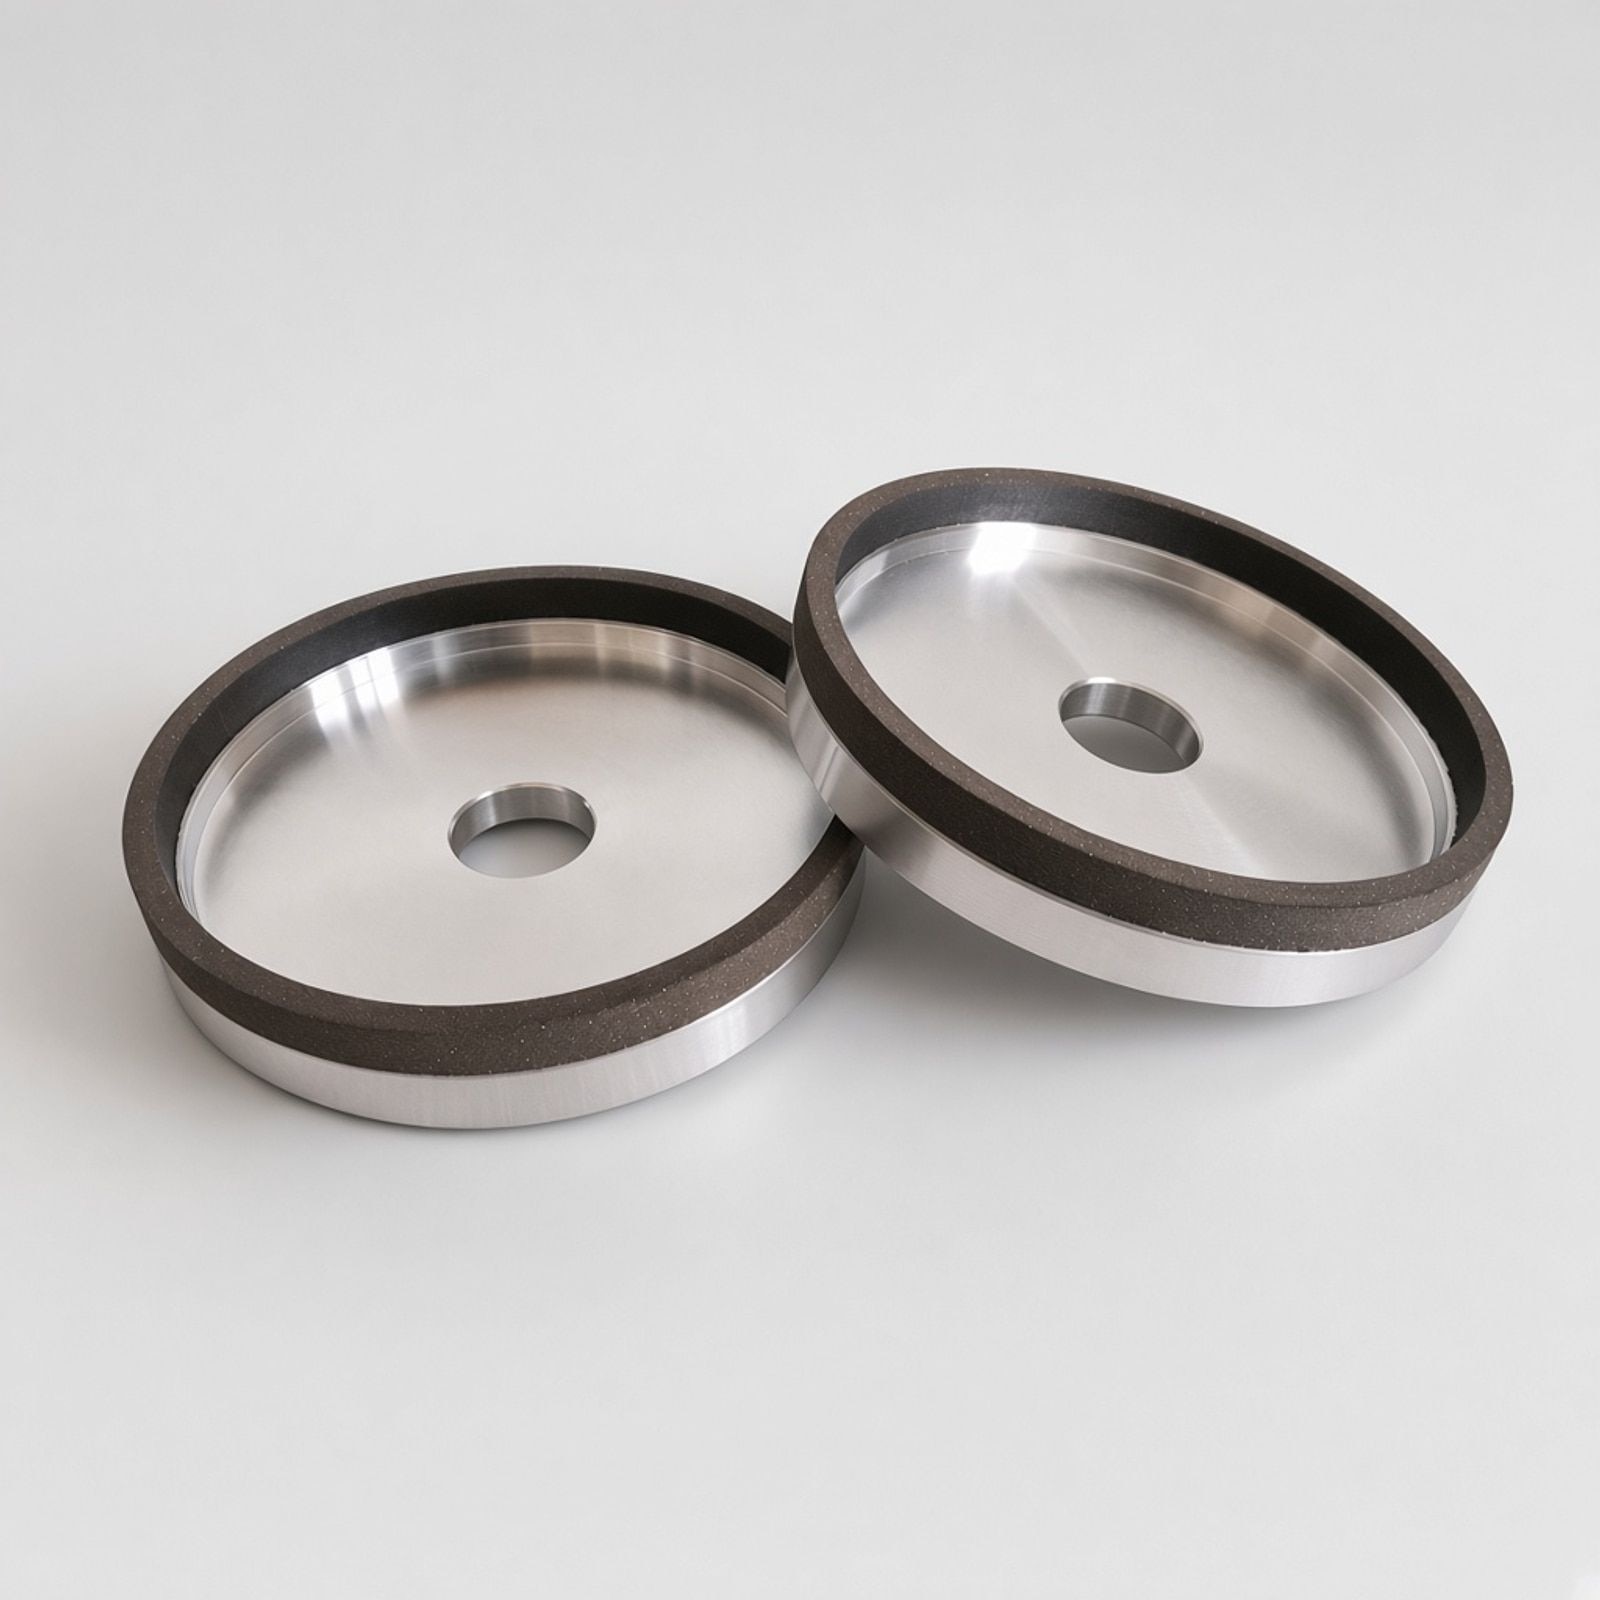
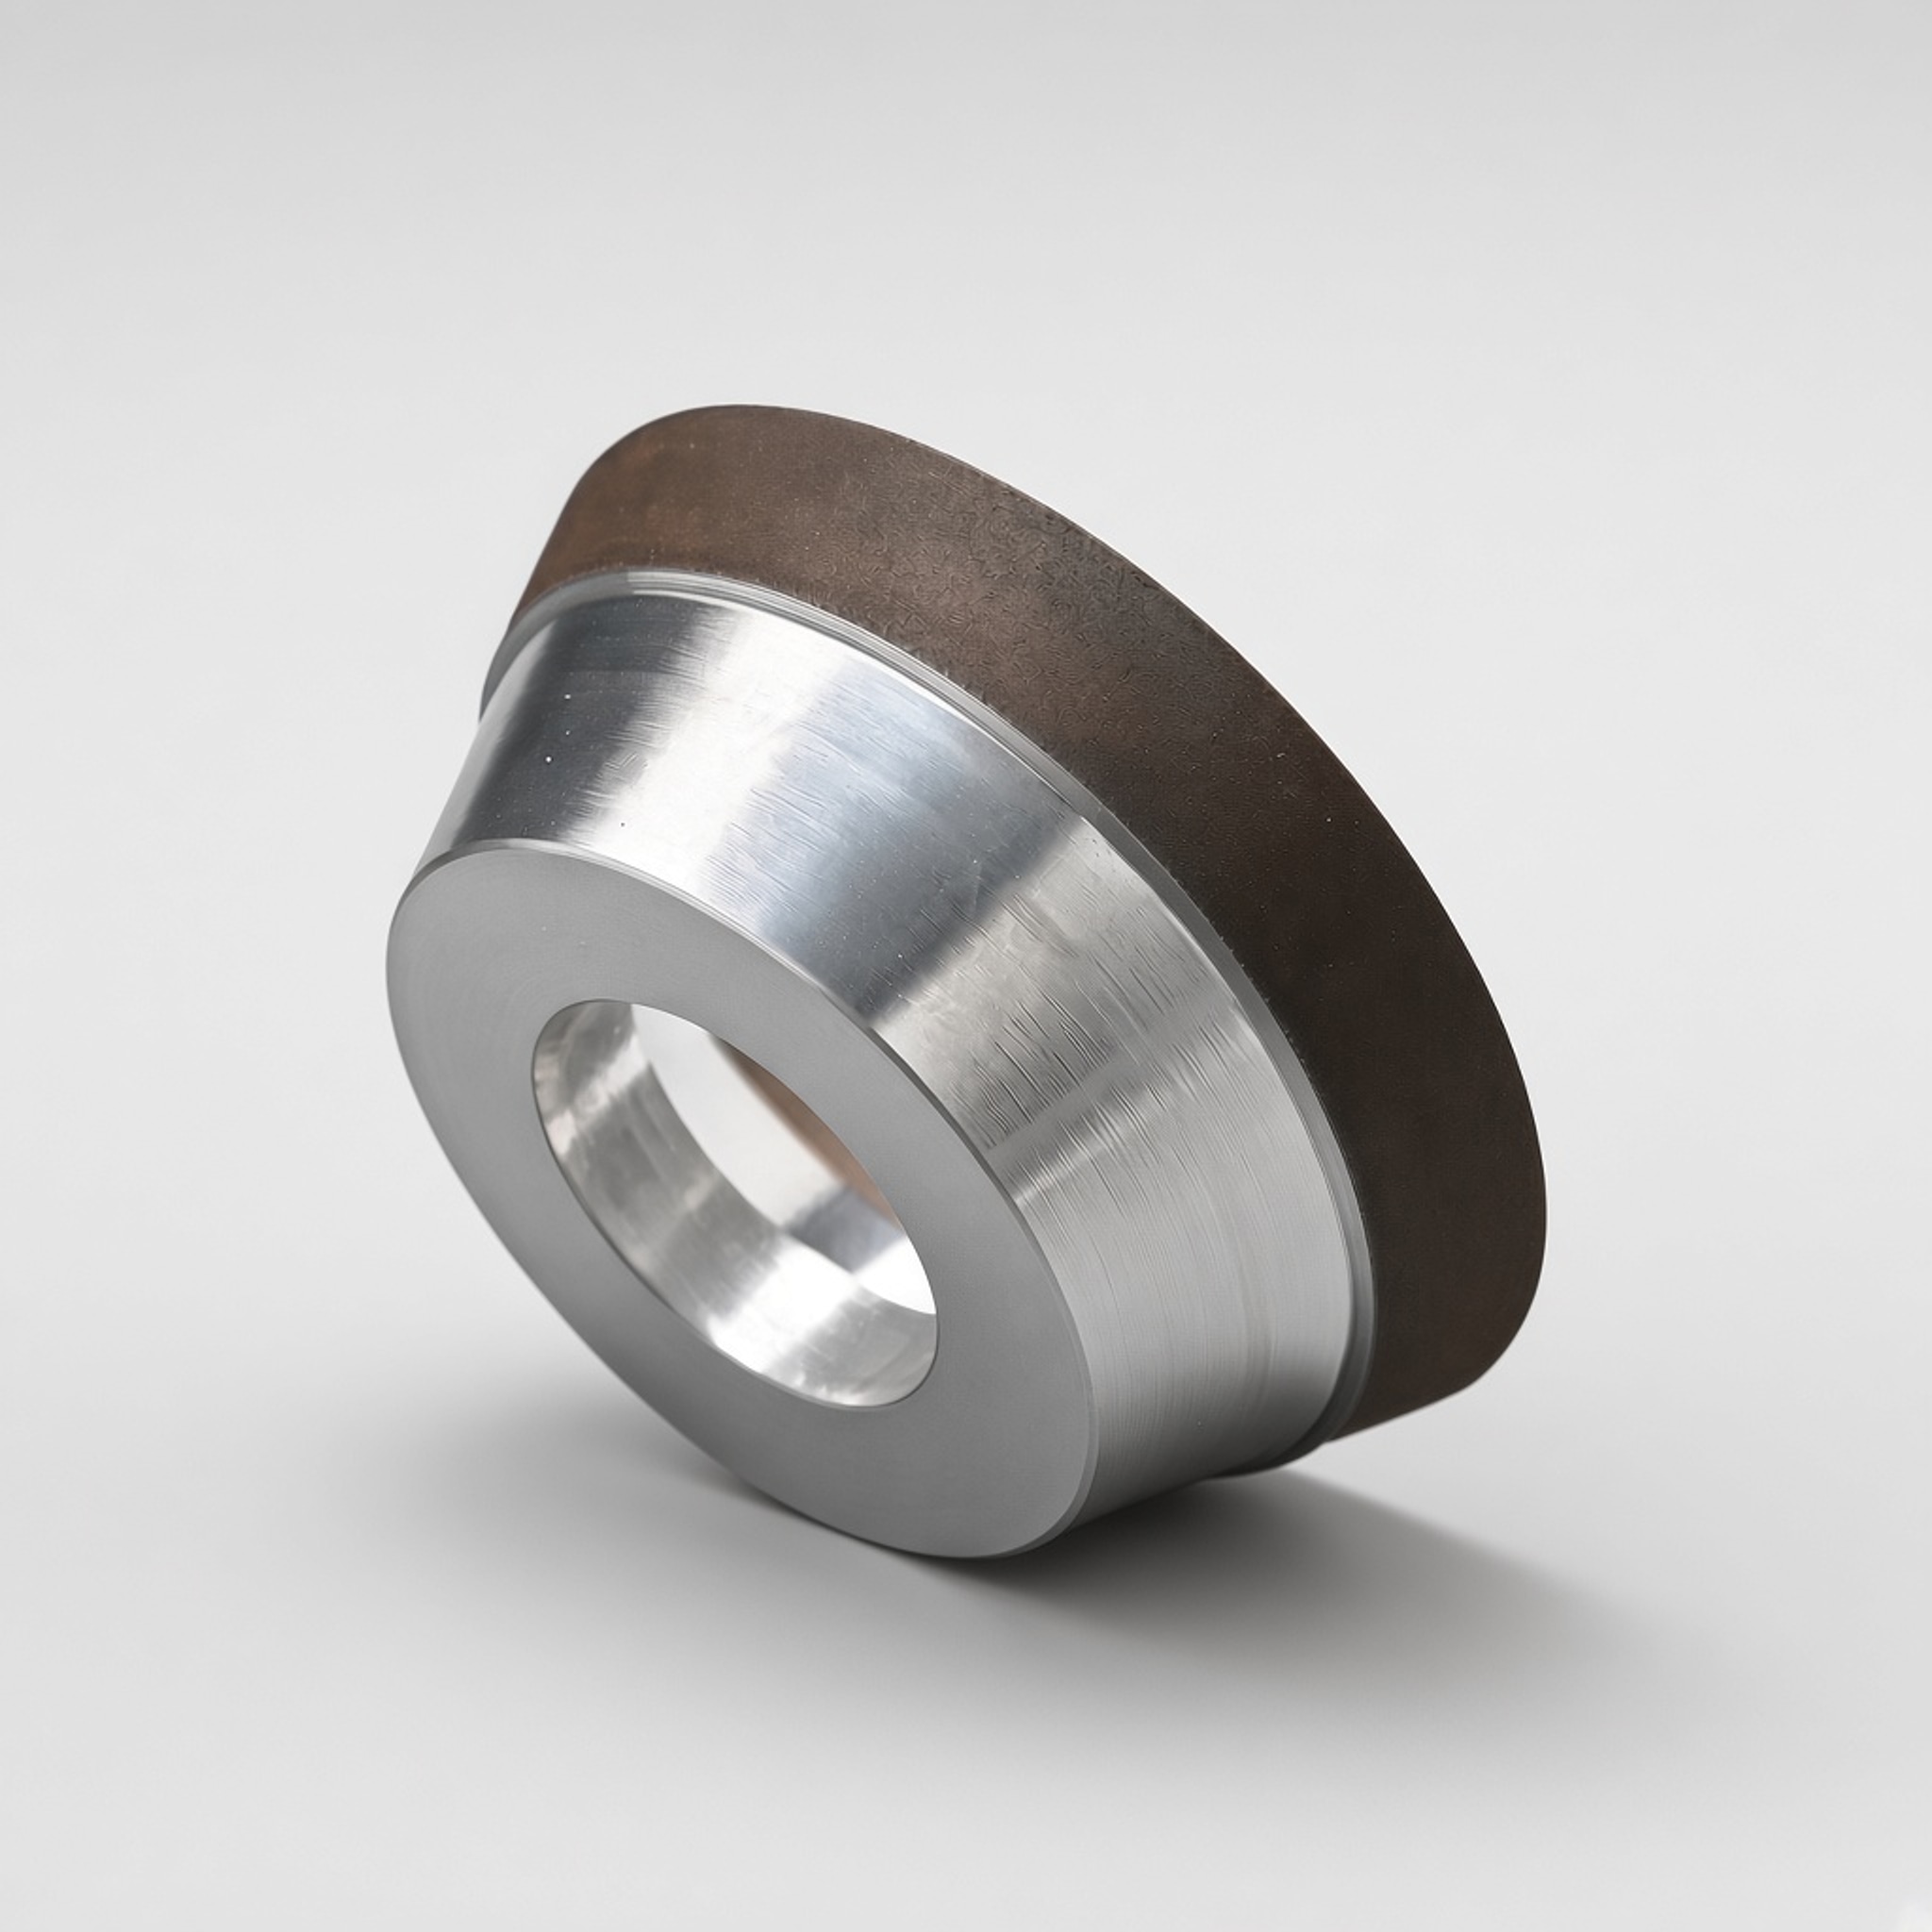
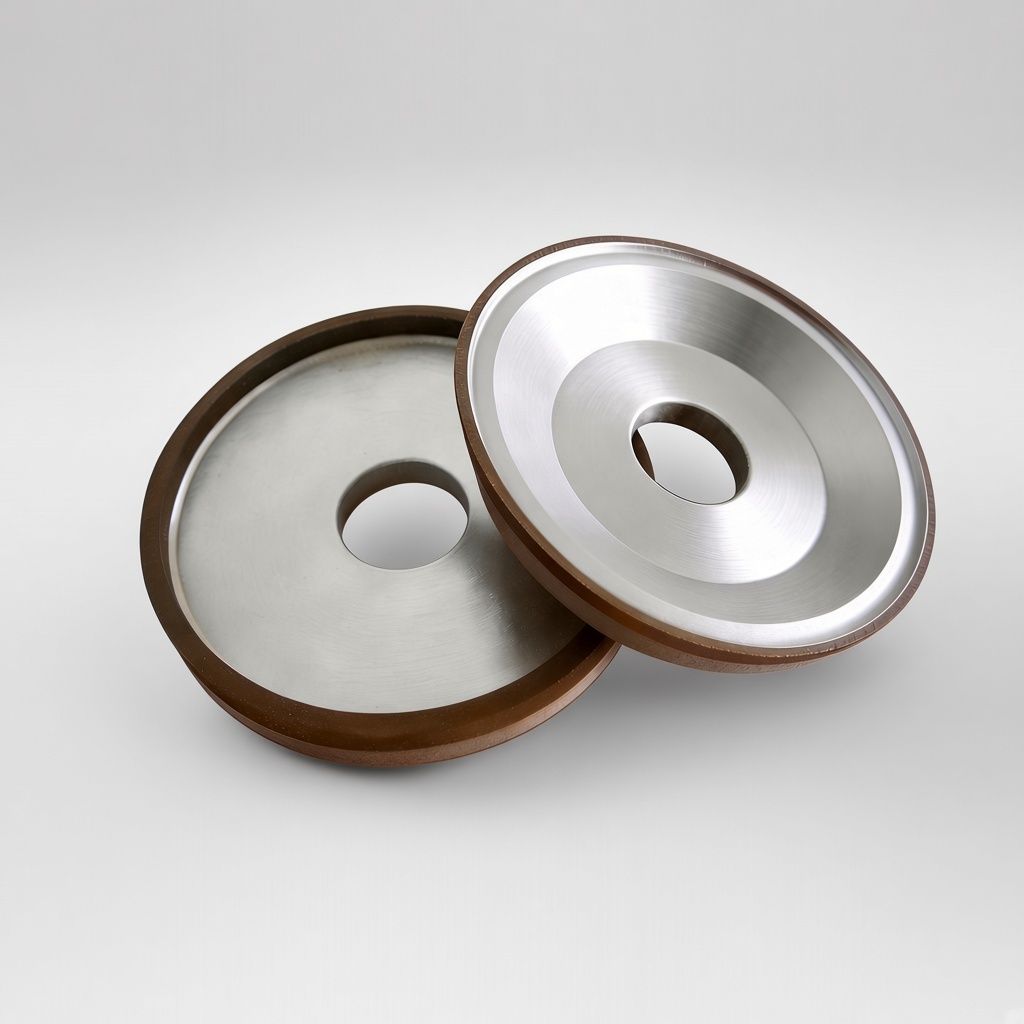
- 1A1 for punch OD and round inserts; 6A2 for die faces
- Diamond on carbide inserts — CBN on mold steel
- Fine finish on punches, cavities, and form inserts
- Made to your diameter, grit, and concentration
Product Information
What we grind
Resin wheels grind the die, not the molded part — punch OD, die-plate faces, carbide inserts, and form cavities. Resin is for finish and geometry: the bond stays cool and self-sharpens on carbide and on hardened die steel.
Typical machines: Okamoto, Jung, Blohm, Chevalier (surface); Studer, Toyoda, Kellenberger (cylindrical); Heald, Moore, Hauser (ID / jig).
Diamond or CBN
| Abrasive | Workpiece | Do not use it on |
|---|---|---|
| Diamond | Carbide die inserts, carbide punches, tungsten-carbide form blocks | Mold steel, H13, D2, SKD11, or any ferrous cavity |
| CBN | Tool-steel / mold-steel punches, cavities, and die plates (D2, H13, SKD11, and similar) | Carbide inserts — use diamond |
If the job is a carbide insert in a steel holder, grind the insert with diamond. Grind the steel body with CBN. One wheel cannot do both.
Shapes
| Shape | Drawing | Role on mold and die |
|---|---|---|
| 1A1 | ![]() |
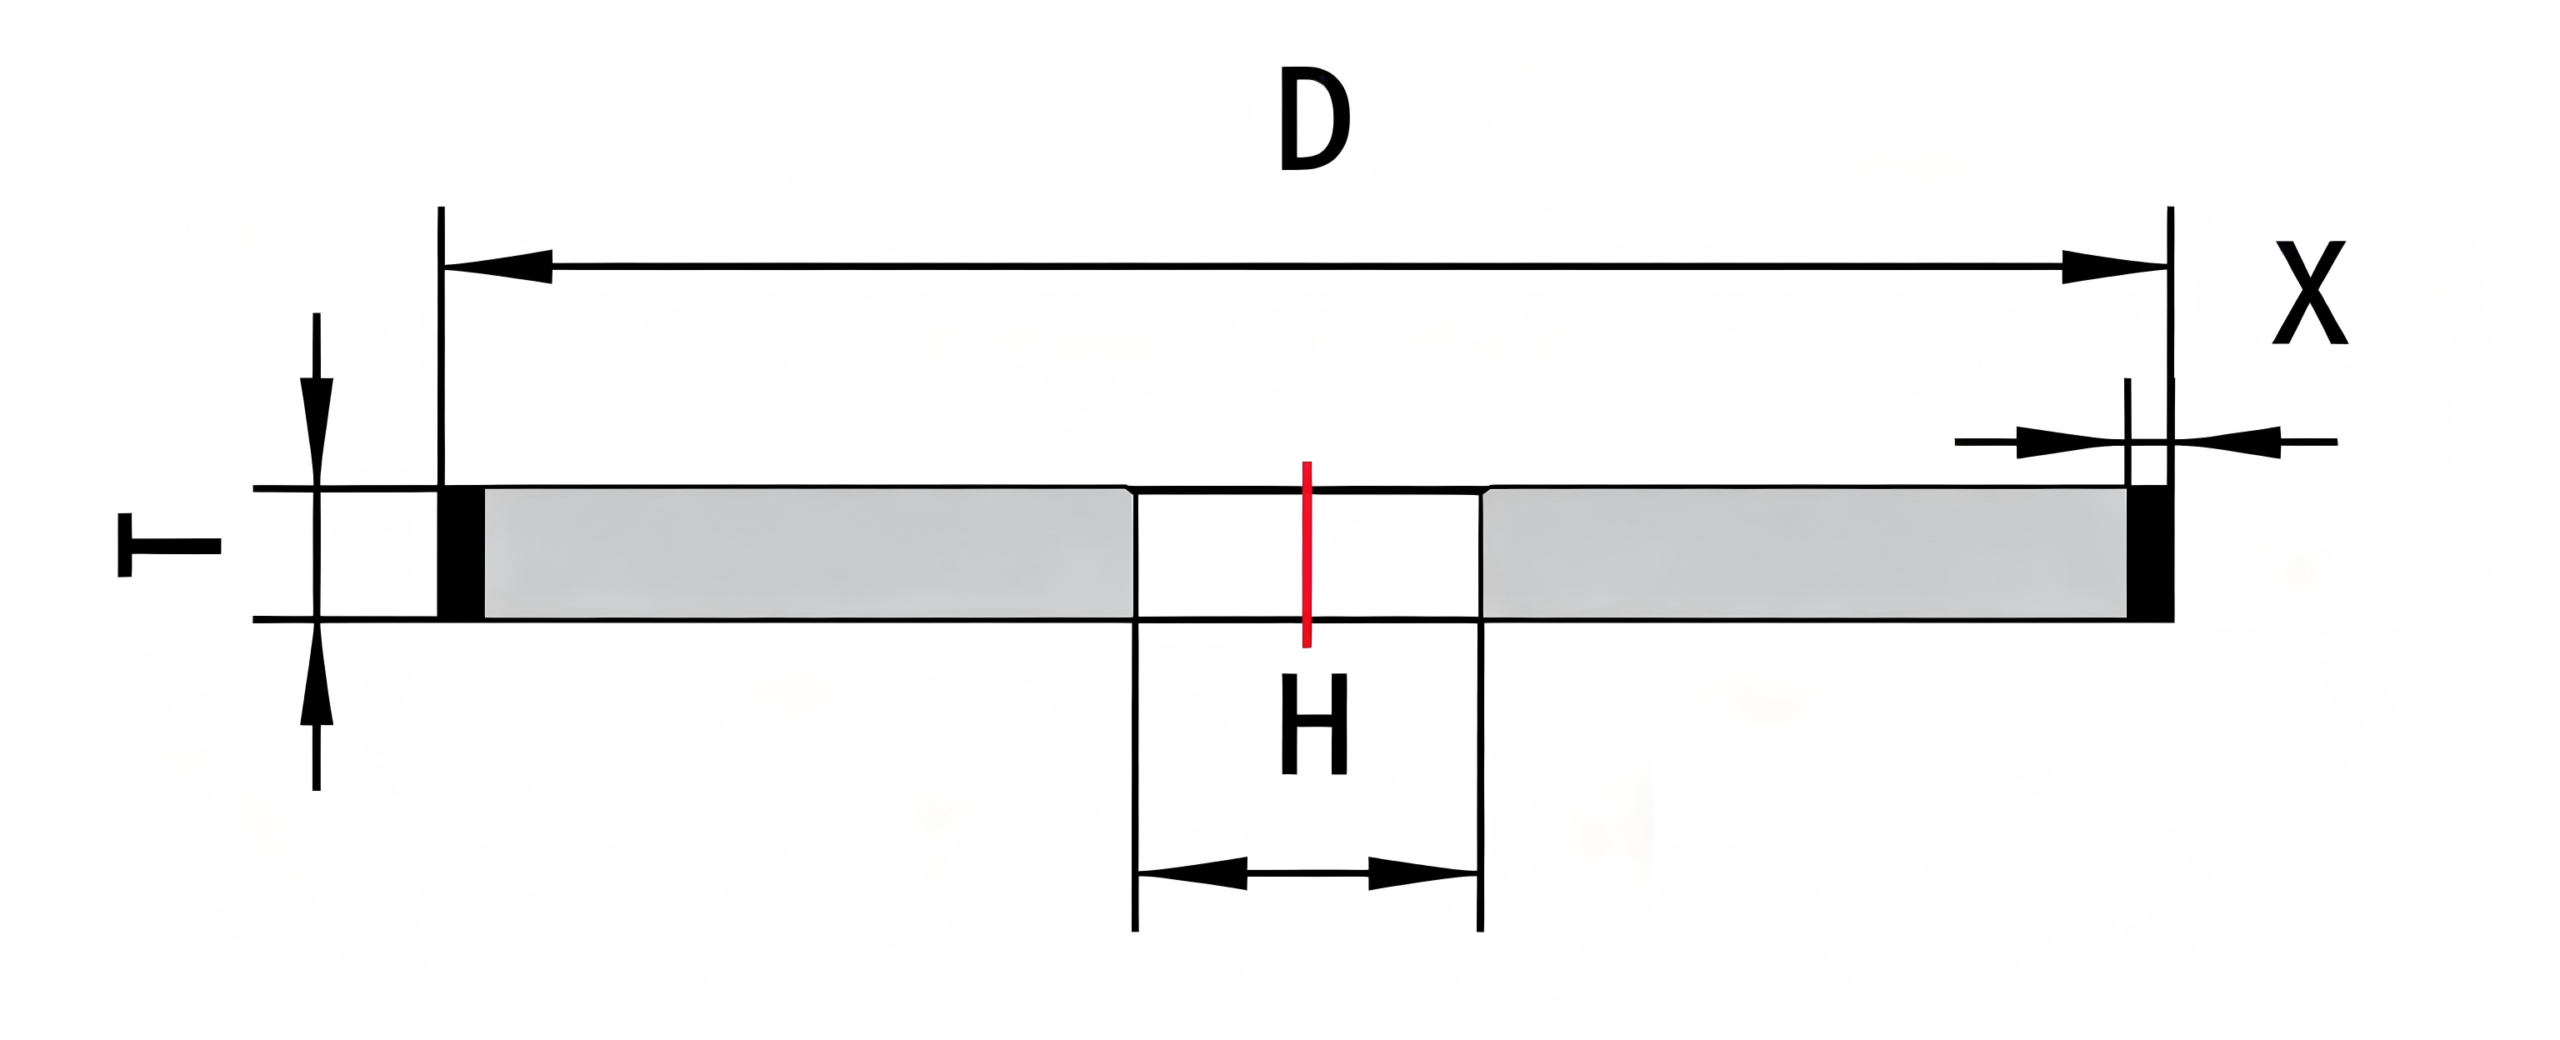
Punch OD; OD / ID of a round insert |
| 6A2 | ![]() |
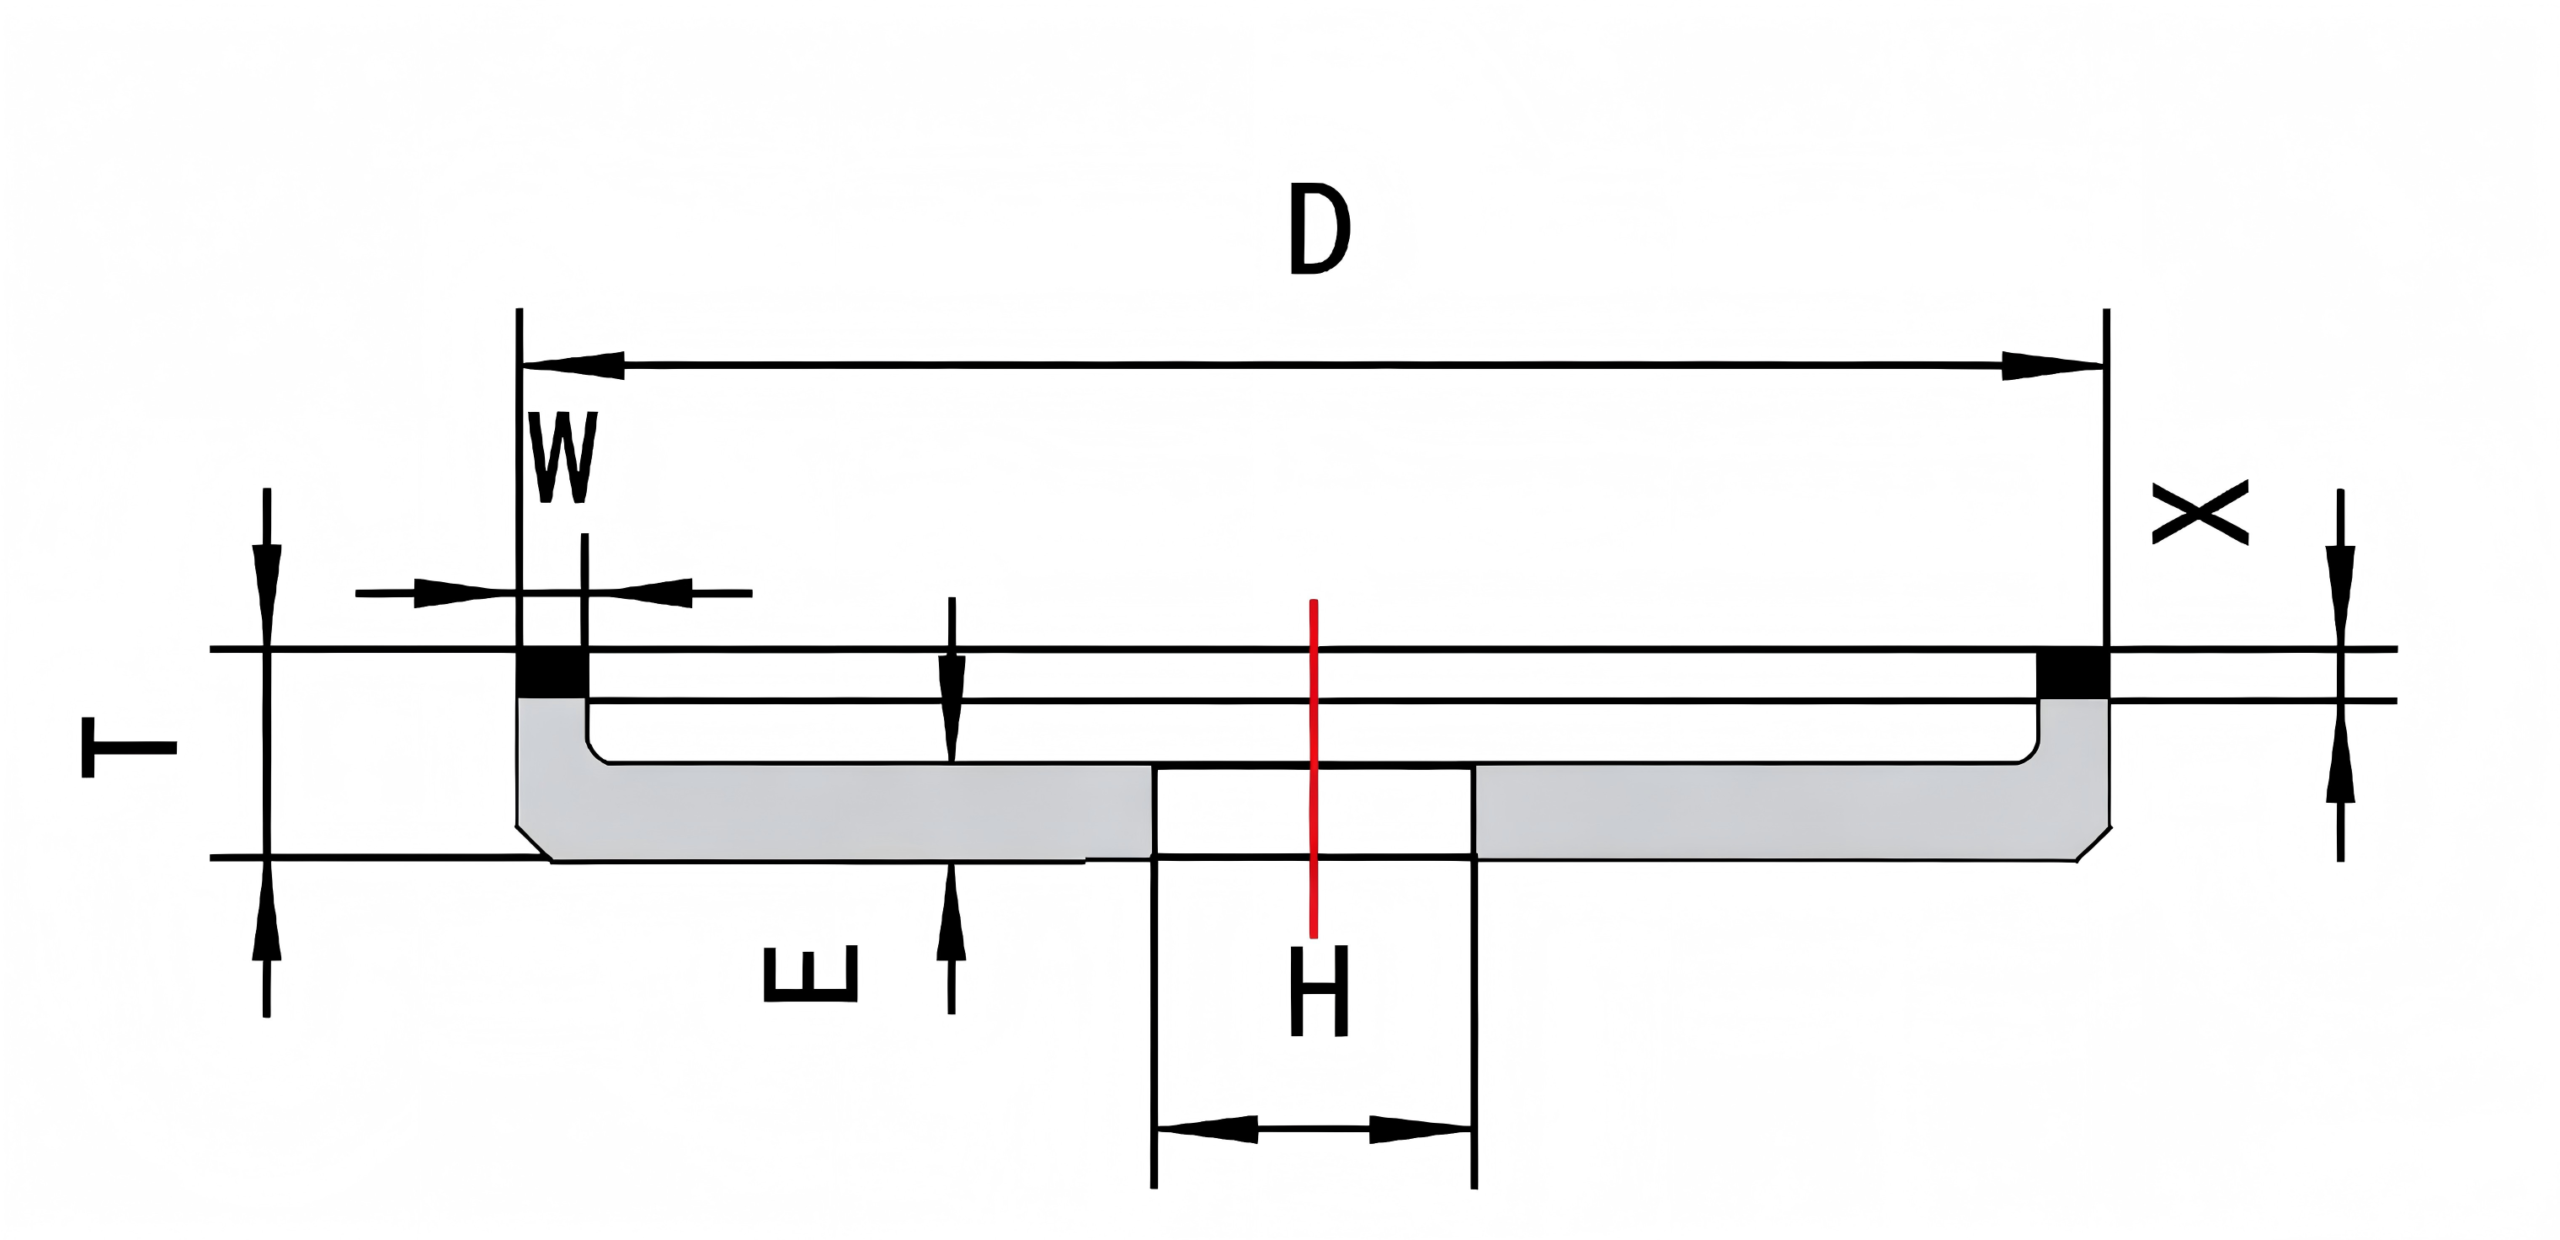
Face of punch or die plate; cup on a flat |
| 11V9 | ![]() |
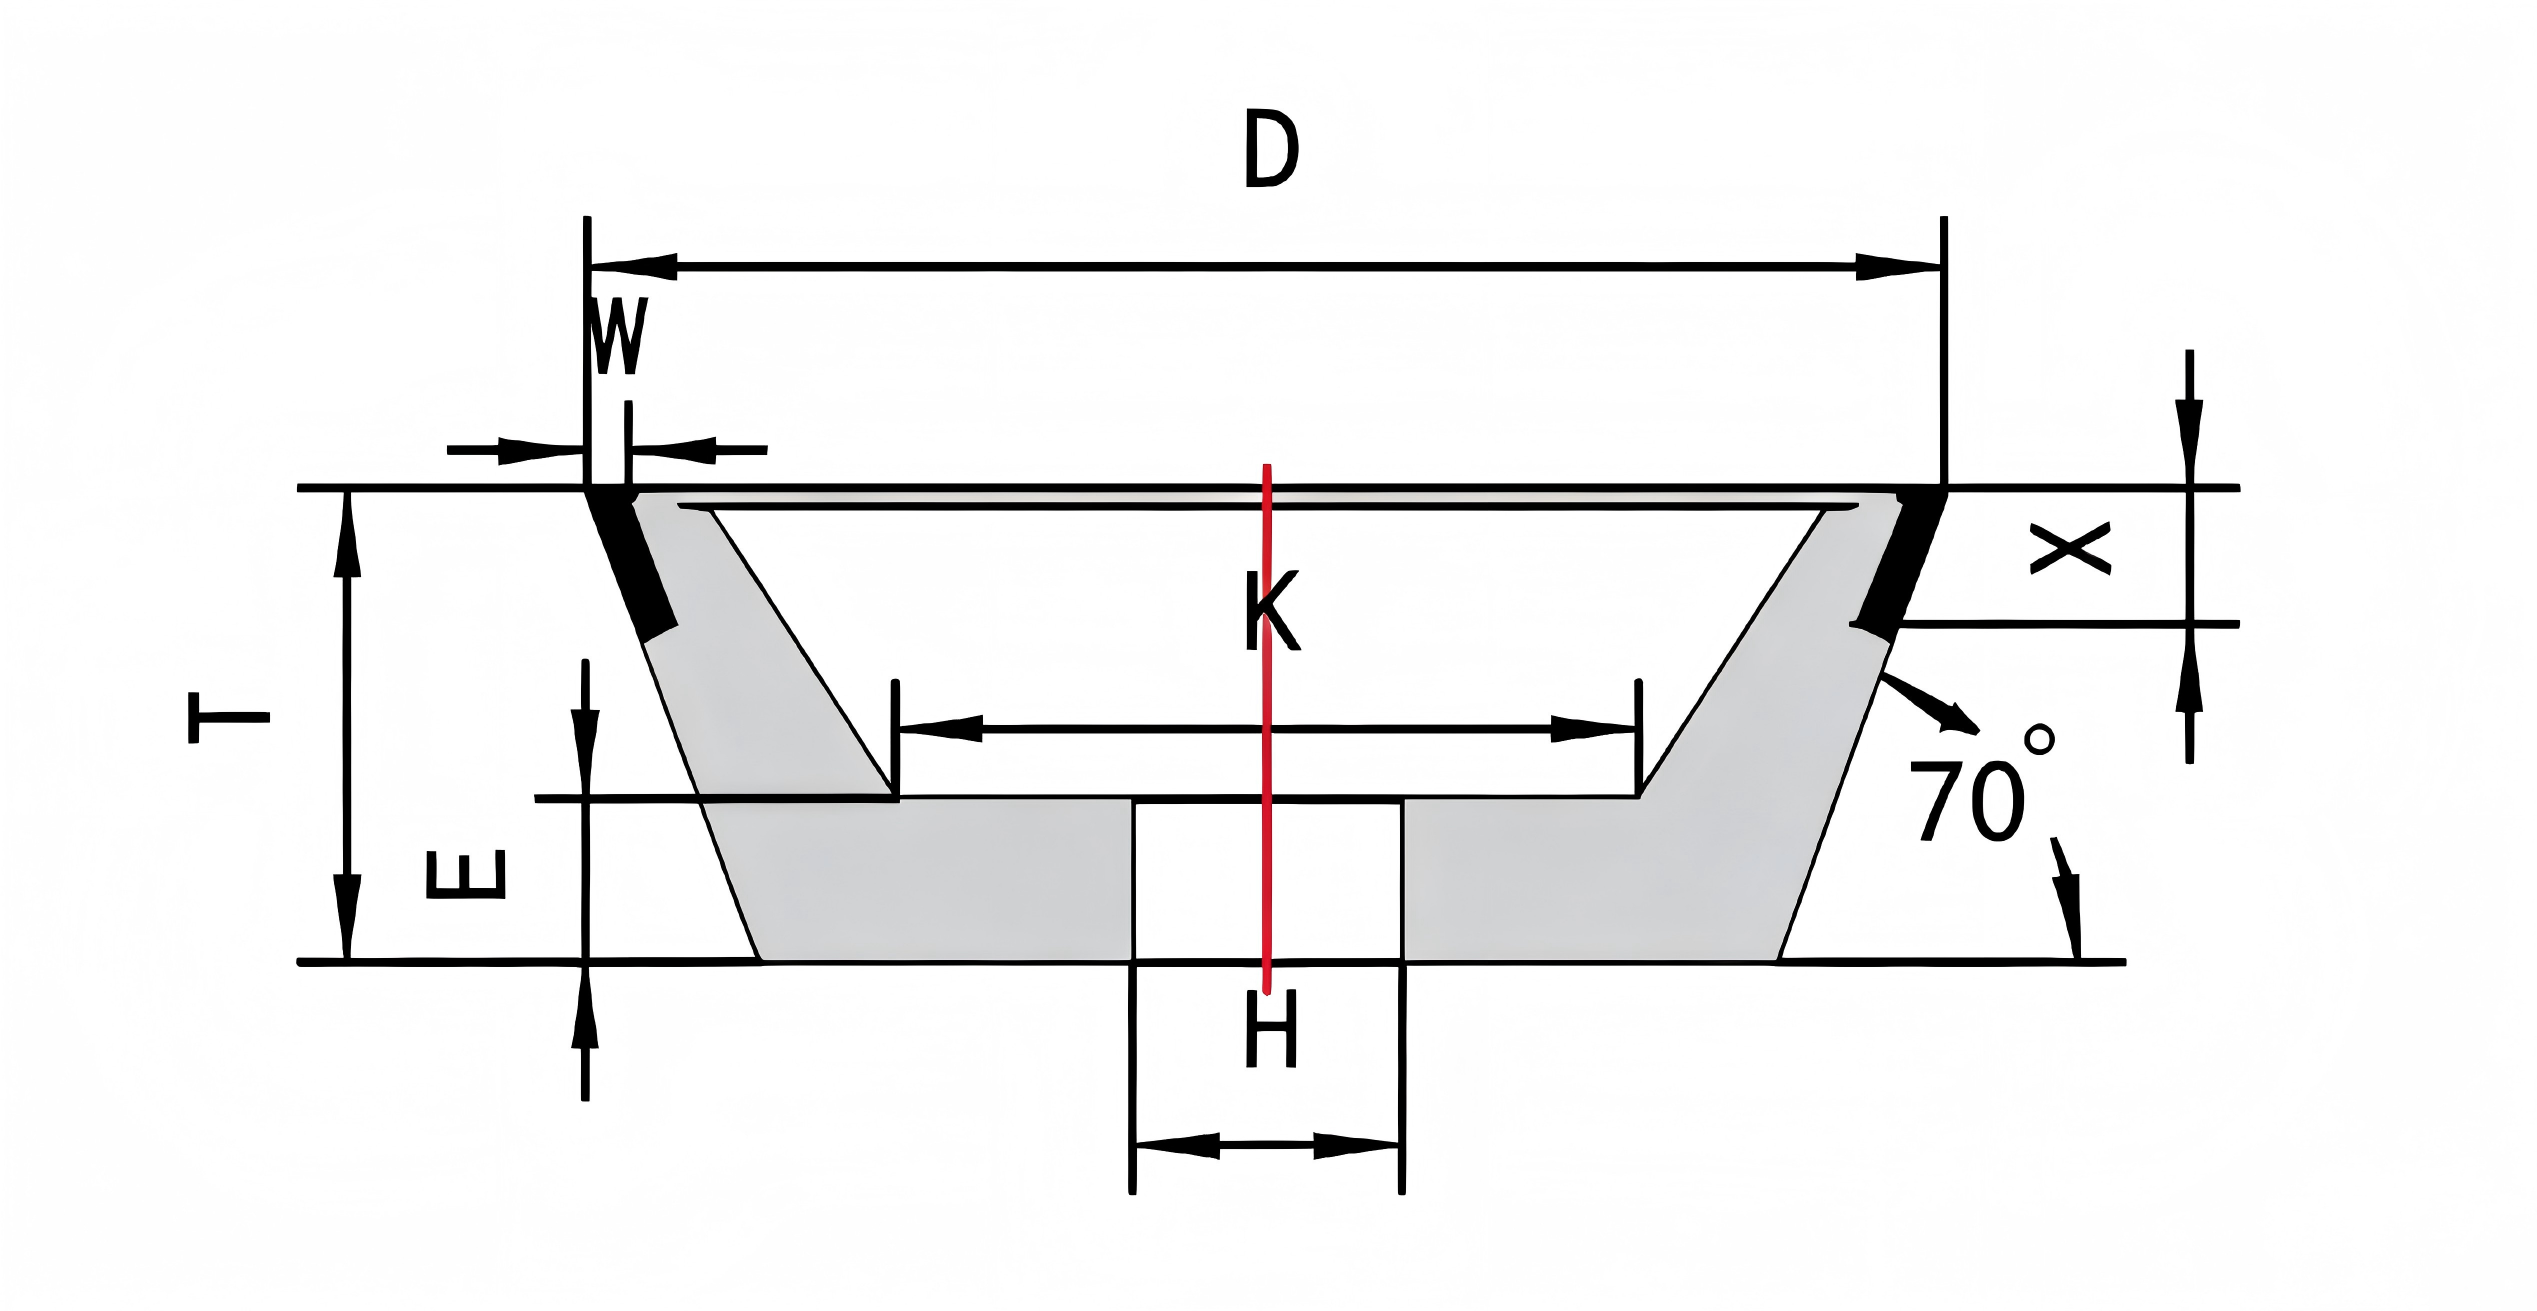
Profile, corner, and clearance on a form insert |
| 12V9 | ![]() |
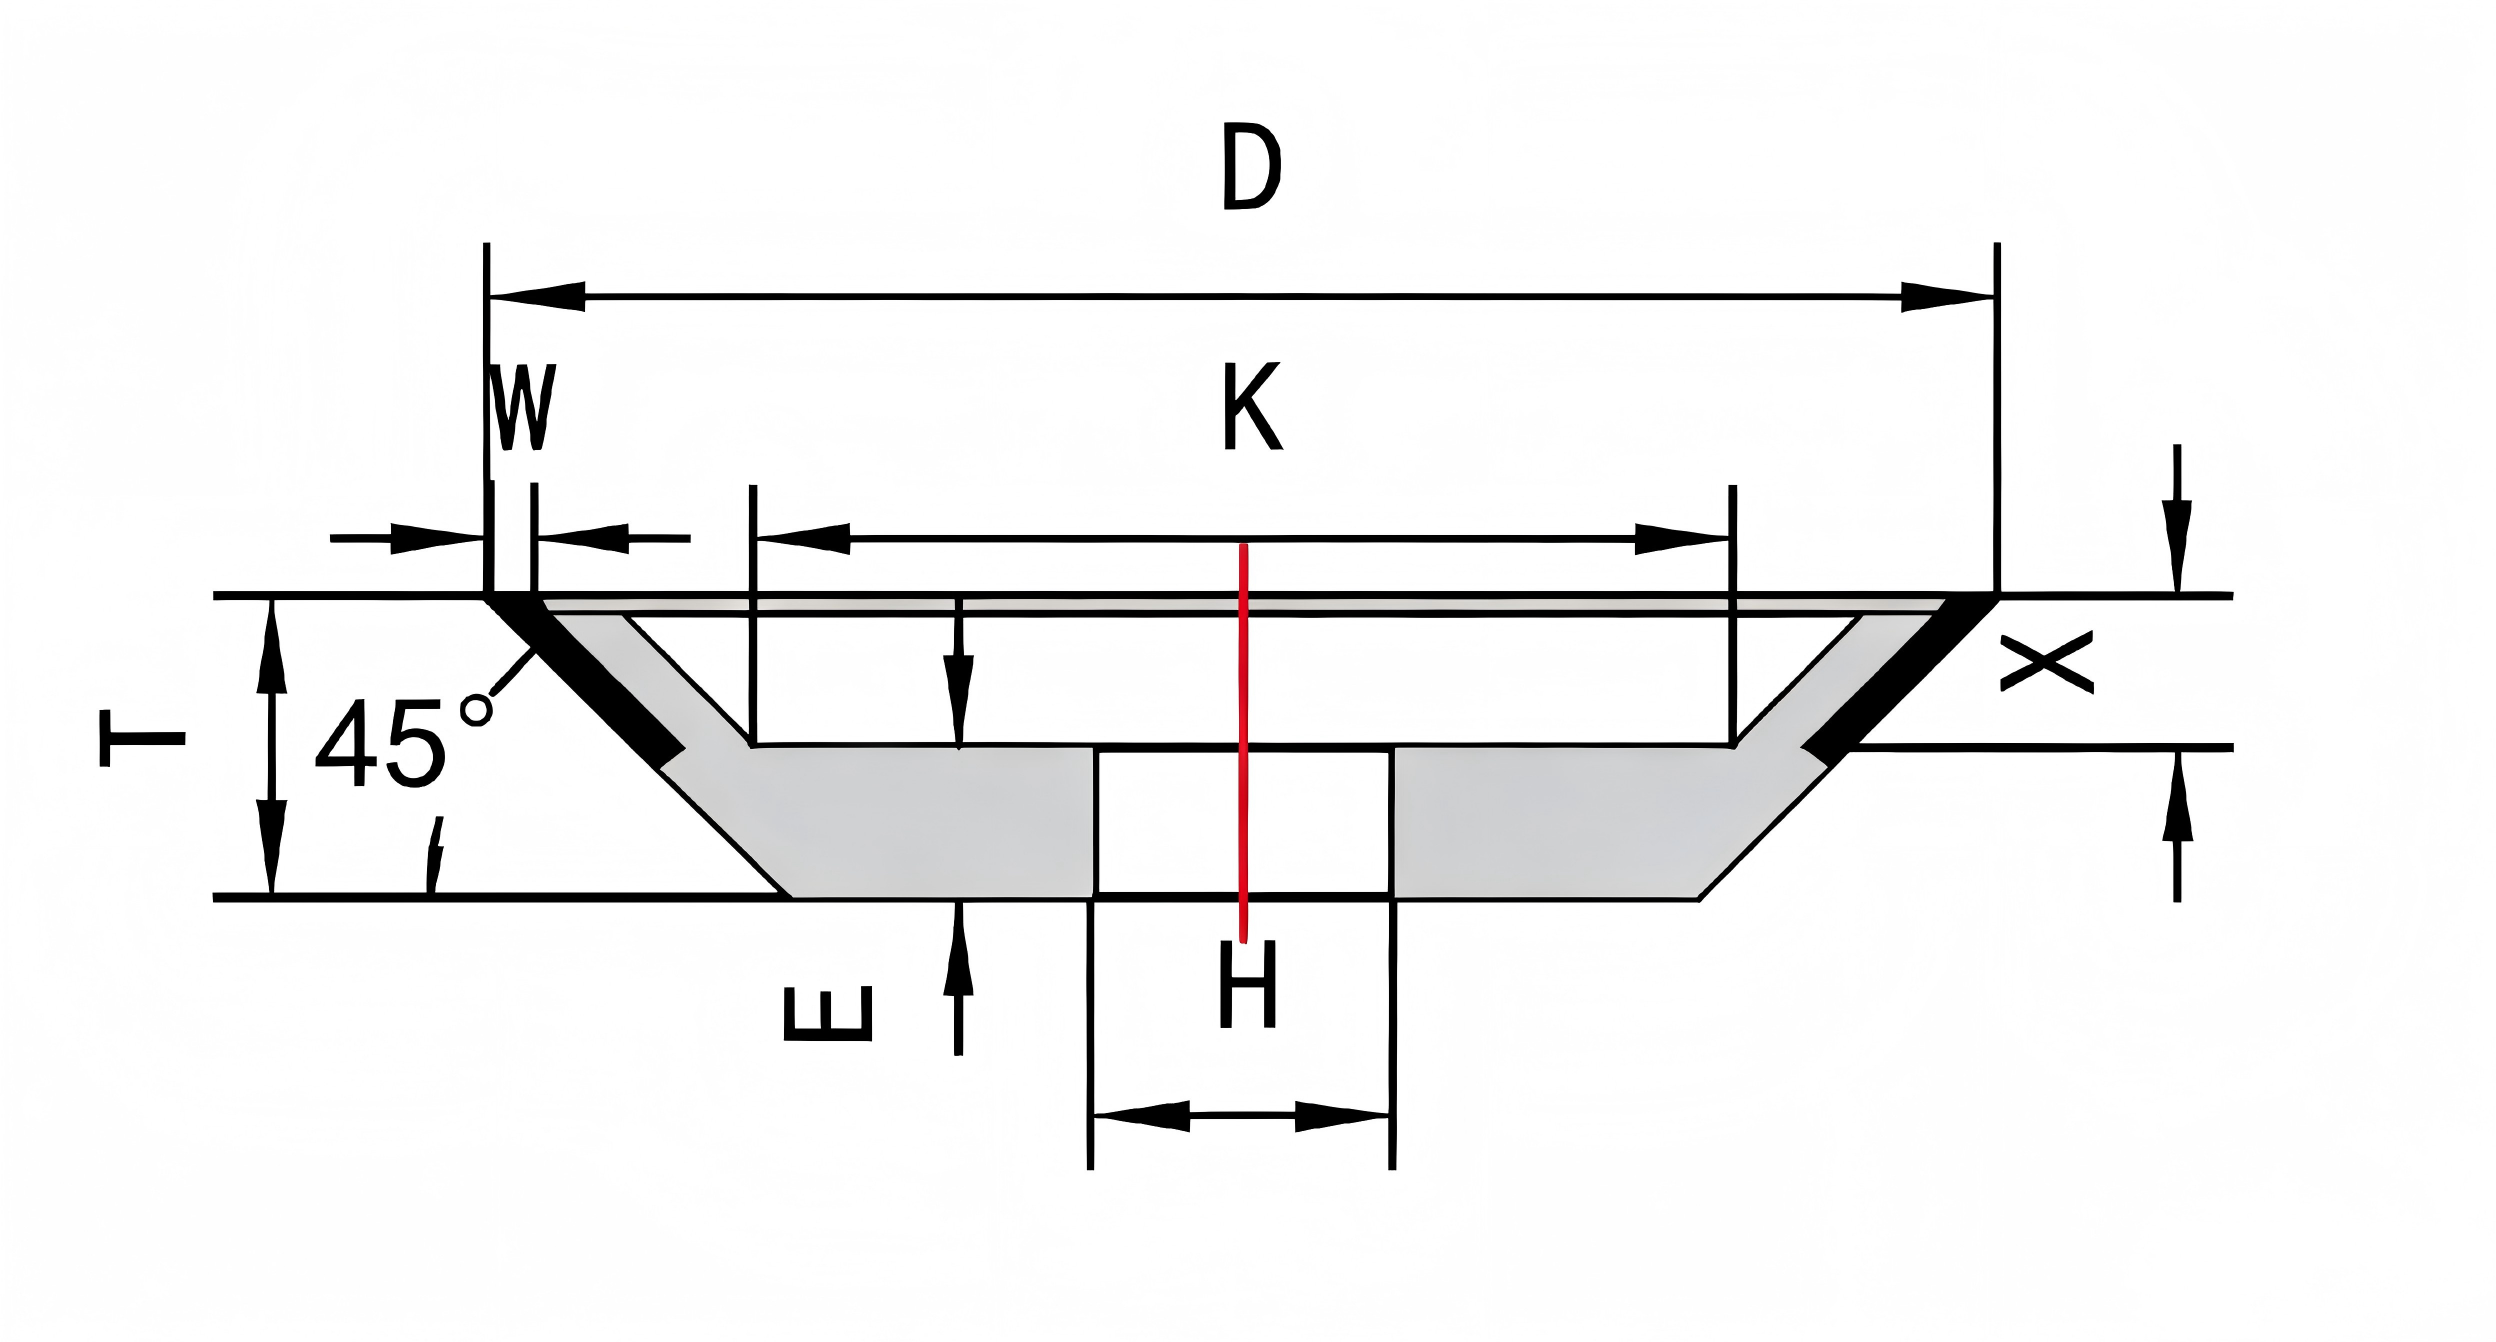
Tighter form-insert gaps than 11V9 |
Also available: 1V1, 3A1 (narrow slot, radius, or step), 14V1.
Send your current wheel mark (e.g. 1A1-150-10-32 D64 C75 or a CBN equivalent) or a drawing. We match diameter, thickness, hole, grit, and concentration.
When resin is the wrong wheel
- Steel punch or cavity with a diamond wheel → CBN
- High-volume PCD / carbide with in-process dressing → vitrified diamond
- Thin cut-off of glass, quartz, or LED substrates → metal or electroplated 1A1R