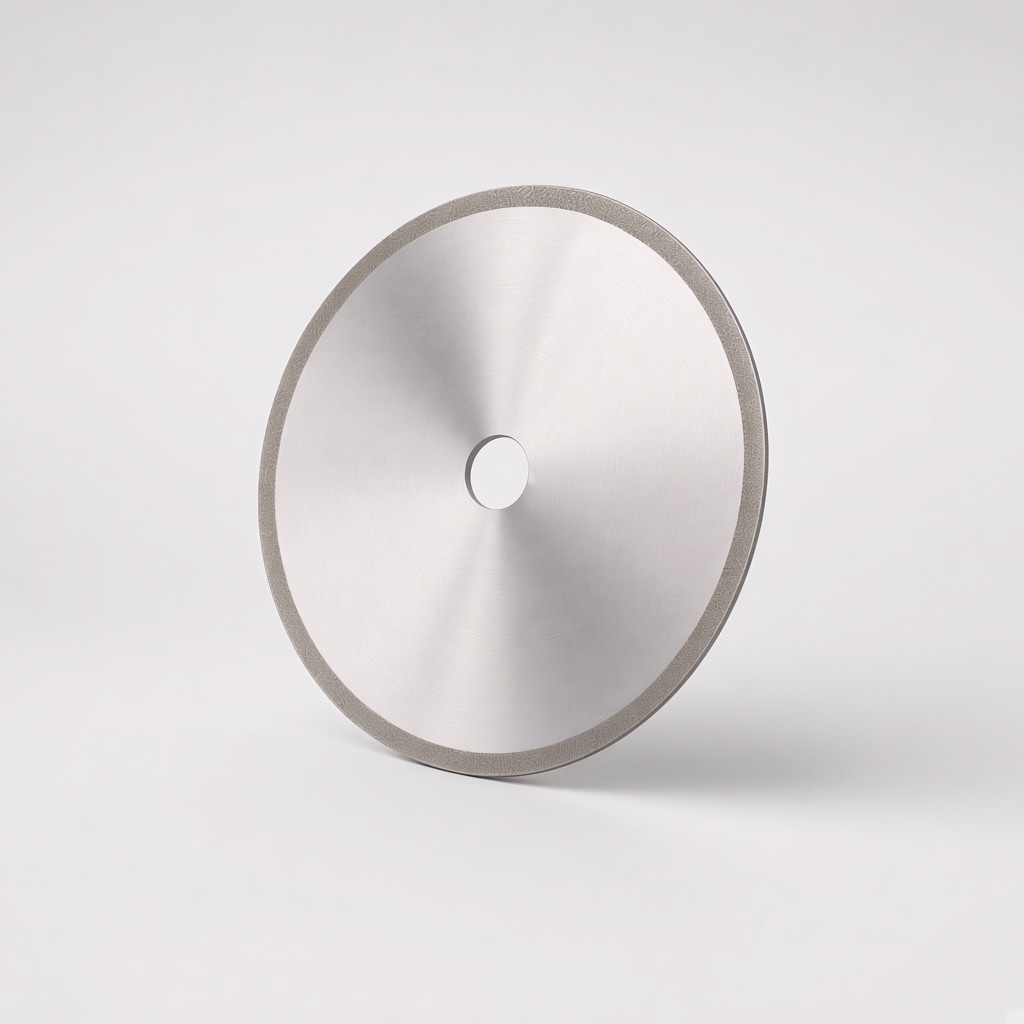
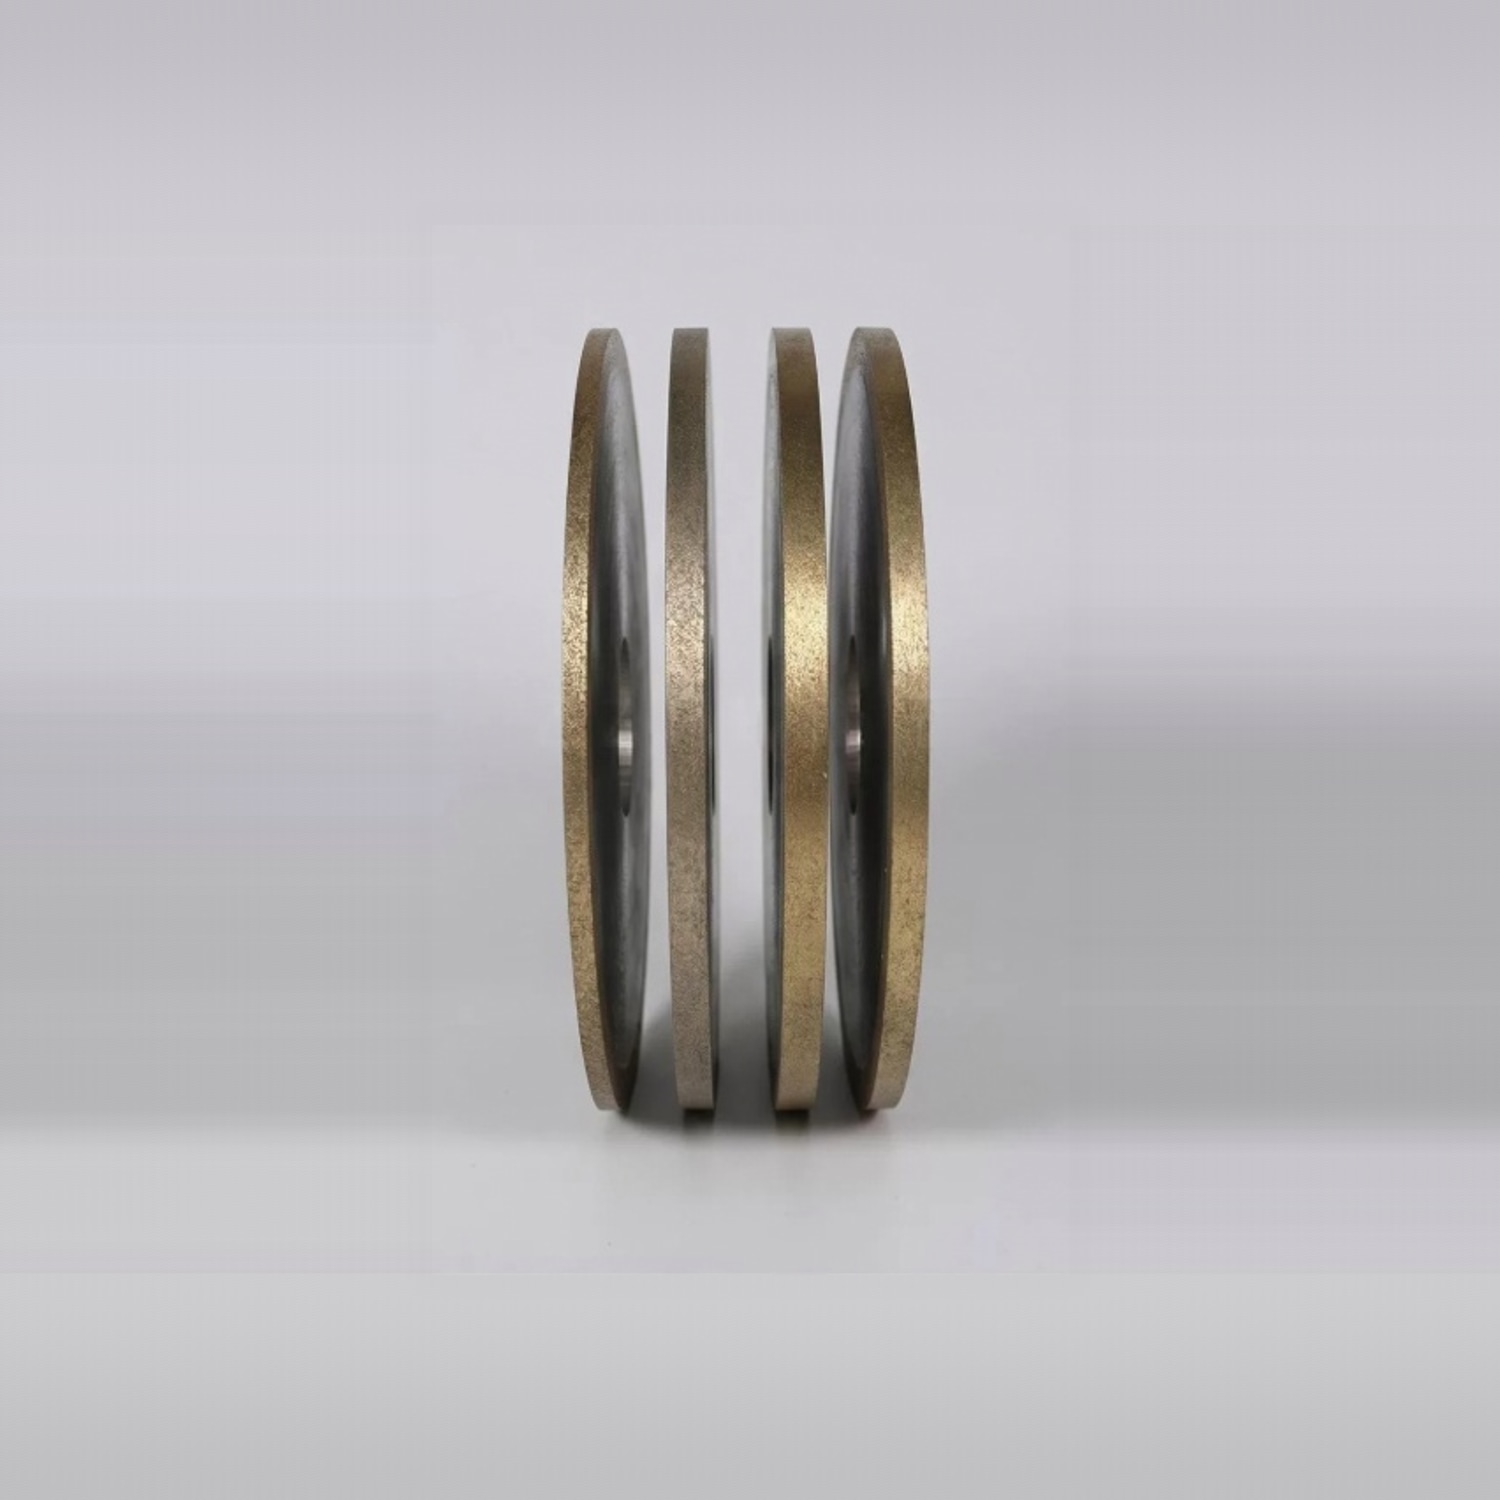
Electroplated Diamond Cut-off Wheels

Product Information​

Overview

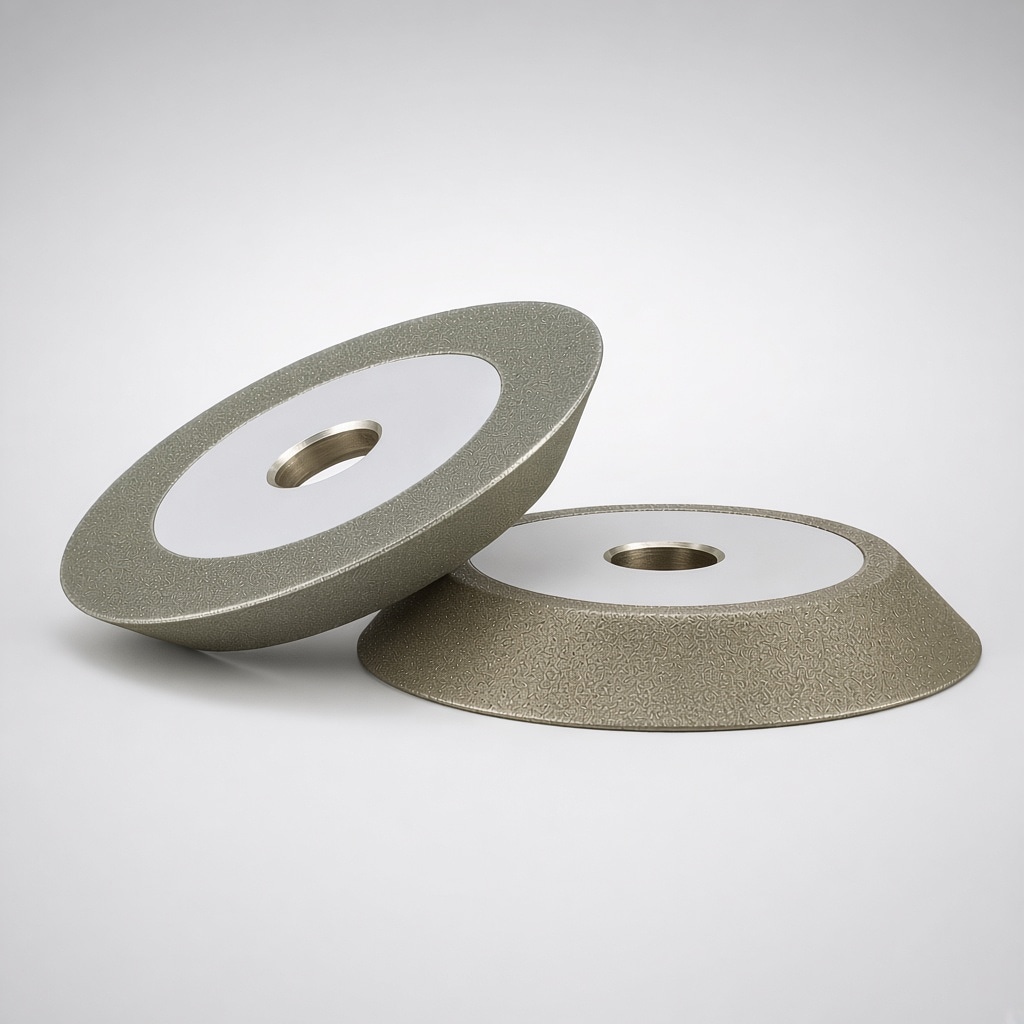
Electroplated wheels for thin cut-off of glass, fused quartz, LED blanks, and technical ceramics. Single-layer diamond on a steel core. Wet cut-off is standard.

  • Sharp on the first cut — low cutting force, less chip-out on glass and quartz
  • Thin rim; thickness is the kerf
  • No dressing — replace the wheel when the rim is dull
  • Short and medium runs

Applications:

  • Glass tube, rod, and sheet cut-off (not straight-line edge grinding)
  • Fused quartz tube, plate, and rod
  • LED wafers, sapphire, and similar hard blanks
  • Technical ceramic bar and plate

Architectural glass edge, arris, and OG stay on metal bond × glass. Silicon wafer production cut-off with life as the first spec stays on metal bond × silicon wafers.

Kerf

Order thickness for the cut you need, not as thin as possible. Glass tube often wants a different T from quartz plate or an LED blank. Wet unless the machine is already dry. Runout on a 0.6 mm rim matters more than a polished side wall.

Metal 1A1R on the same saw is the long-life rim. Keep it if the blade already lasts the shift. Use plated 1A1R when you need a sharper first cut, a thinner T than the metal rim you have, or a diameter and hole the metal tool is not tooled for.

Shapes

Shape Drawing Role
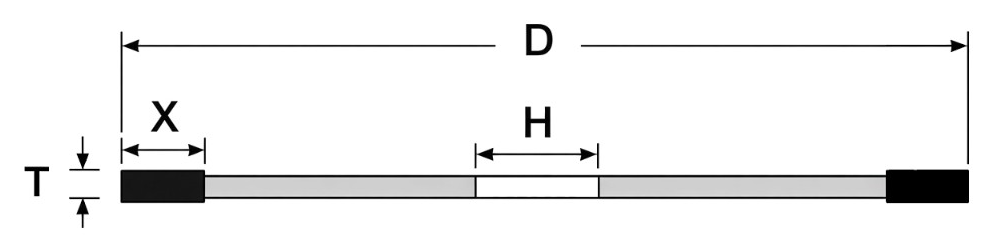
1A1R 1A1R cut-off wheel drawing Thin wet cut-off. Core + plated diamond rim. Kerf follows rim thickness
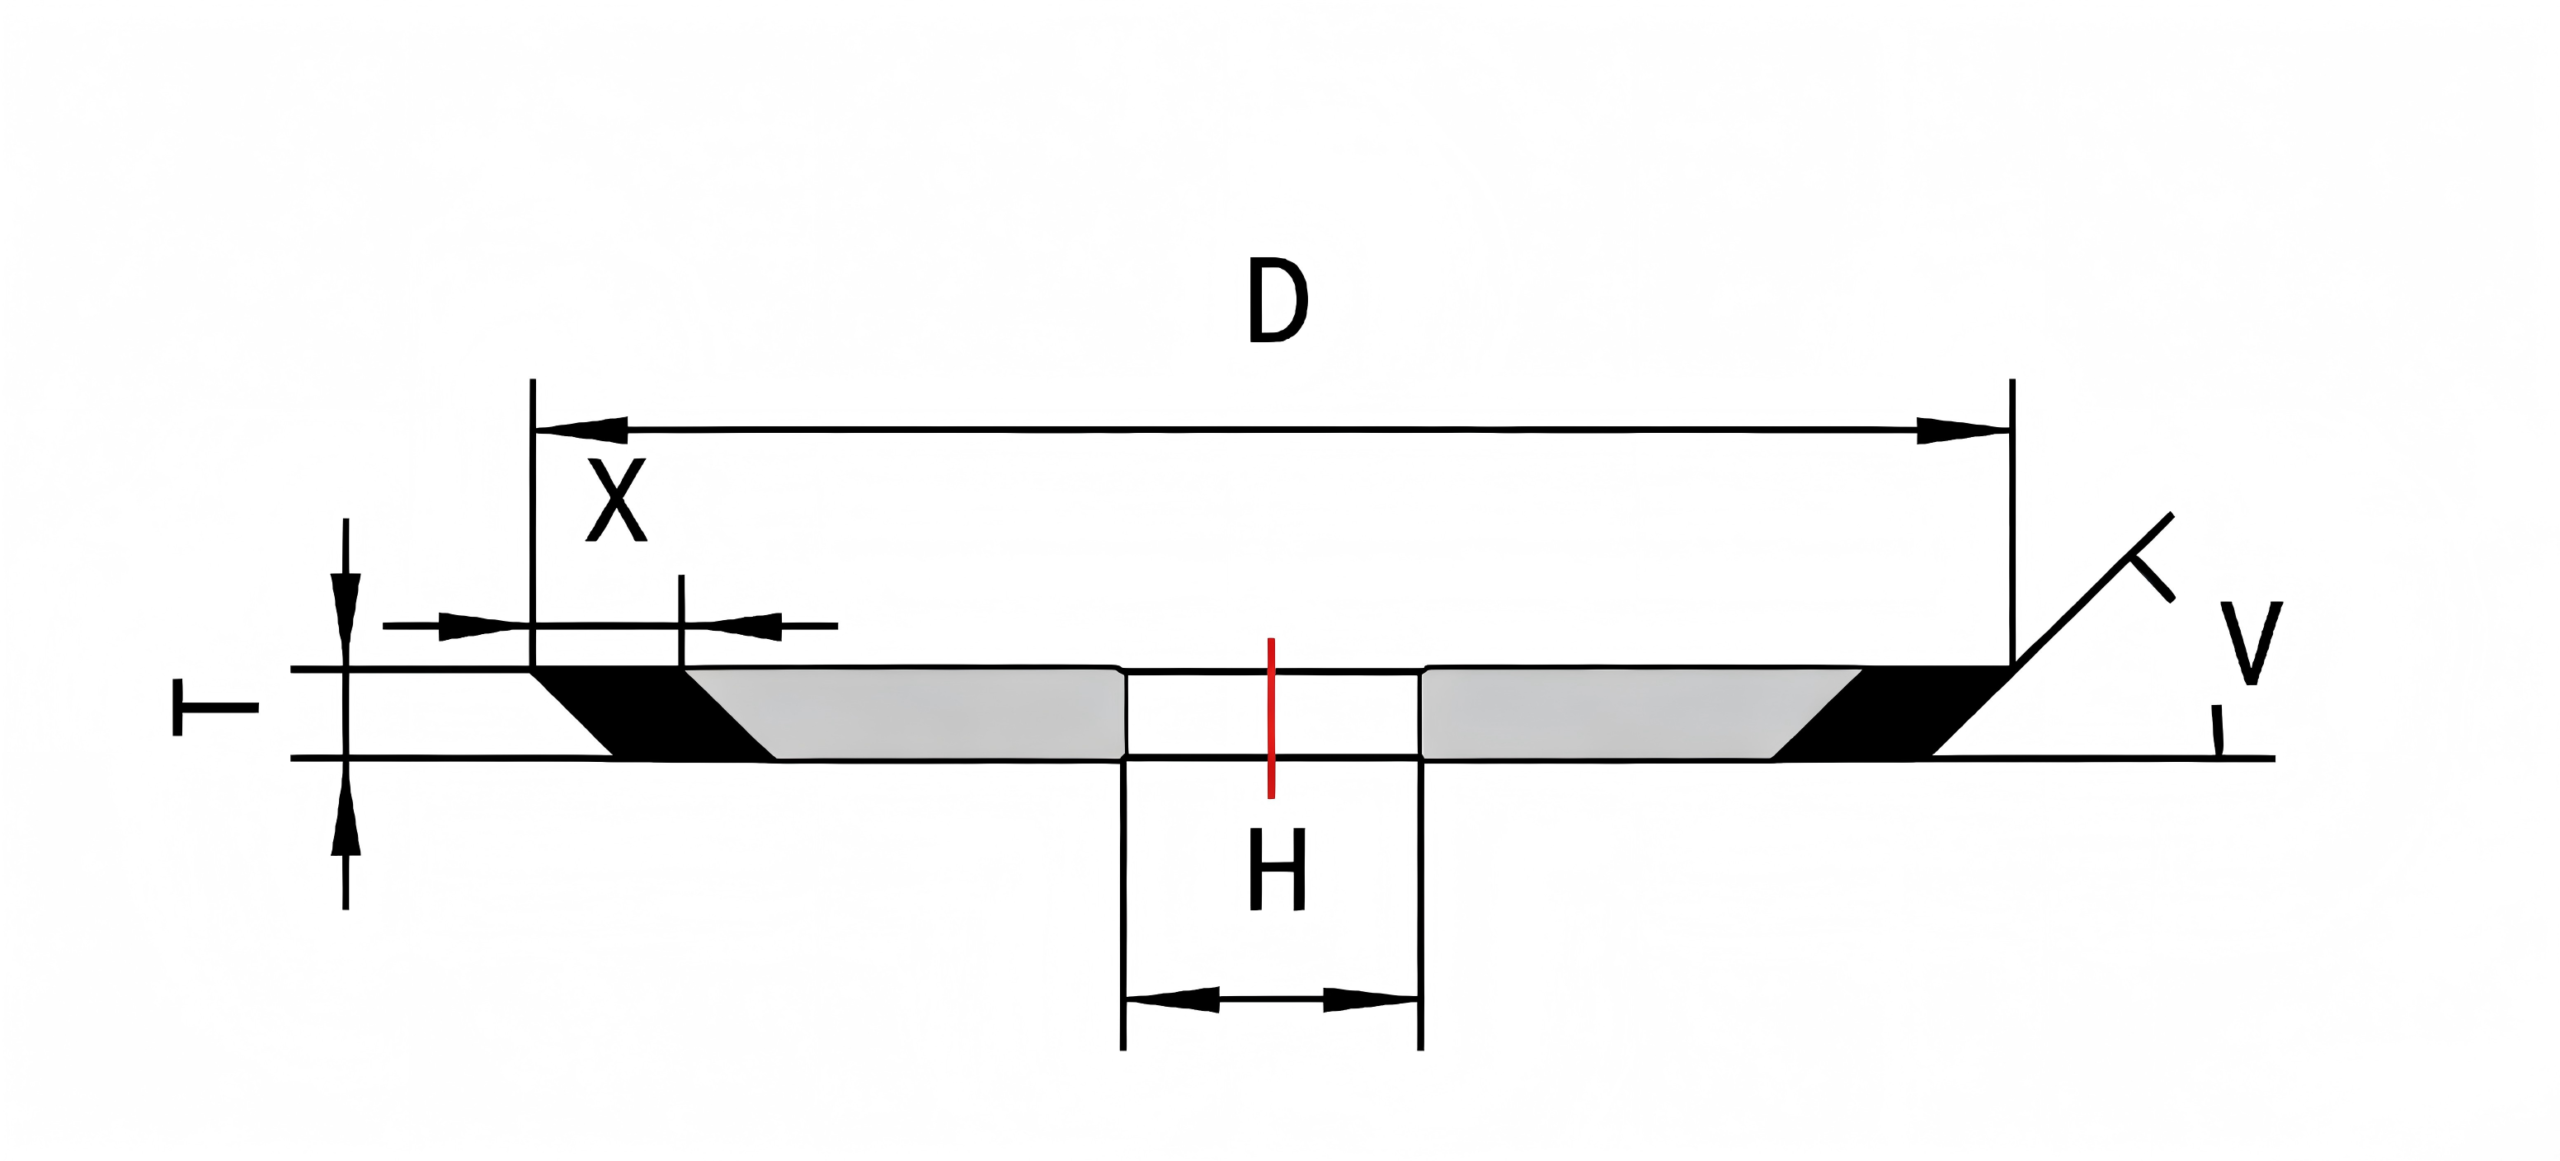
1V1 1V1 wheel drawing Narrow groove or a bevelled cut when the stamp is already 1V1

Send a mark such as 1A1R-125-0.6-22 plus material (glass / quartz / LED / ceramic), wet/dry, and kerf if you already run a number. We match diameter, thickness, hole, and grit.
When electroplated cut-off is the wrong wheel

Related Products

Request a Quote